When it comes to efficient and reliable handling of wheat, the design of a negative pressure pneumatic conveying system represents a critical advancement in agricultural processing technology. This system, developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, is engineered to meet the stringent demands of modern wheat processing operations. The system is specifically tailored to handle the unique characteristics of wheat, ensuring minimal product degradation while maximizing operational efficiency.
Key Features and Technical Specifications
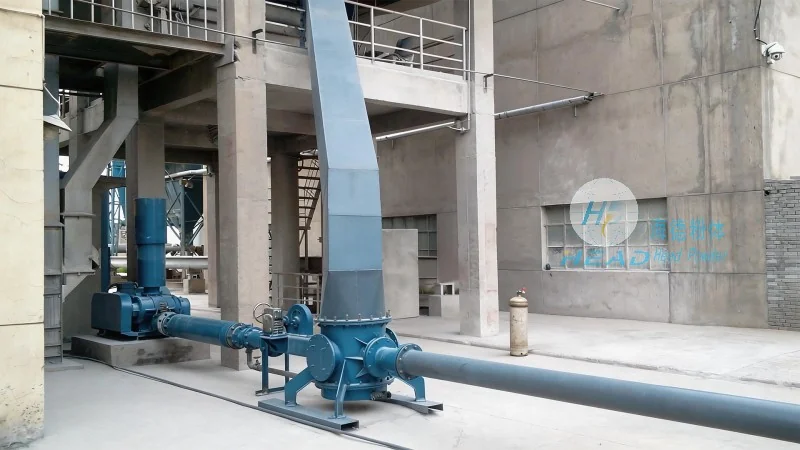
The negative pressure pneumatic conveying system for wheat is built with precision-engineered components that ensure optimal performance under various operational conditions. The system operates on the principle of creating a vacuum within the conveying line, which draws the wheat particles from the source to the destination. This method is particularly effective for handling fine or delicate materials like wheat, as it minimizes the risk of breakage and contamination. The system incorporates high-quality materials, such as stainless steel and corrosion-resistant alloys, to ensure durability and longevity. Additionally, the design allows for adjustable conveying rates, enabling operators to control the flow of wheat according to specific processing requirements. The system also features integrated filtration and cleaning mechanisms to maintain air quality and prevent dust accumulation, which is essential for maintaining product purity and compliance with industry standards.
Advantages of the Negative Pressure System
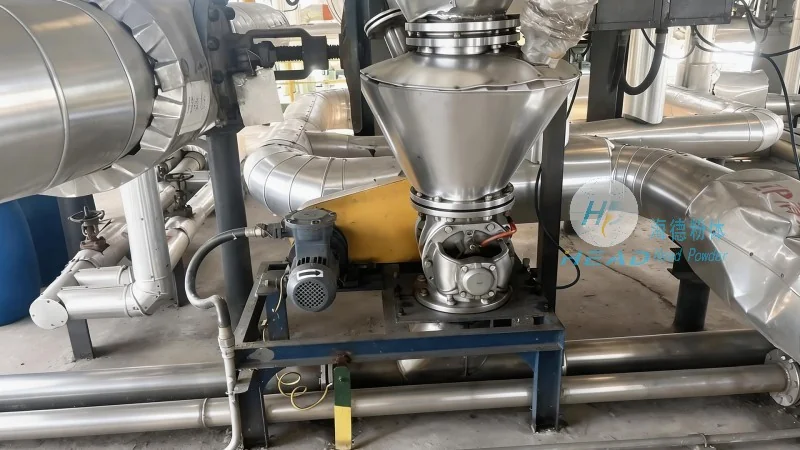
Compared to traditional conveying methods, the negative pressure pneumatic conveying system offers several distinct advantages. Firstly, it provides a closed system, which significantly reduces the risk of dust emissions and environmental contamination. This is particularly important for wheat processing facilities, where dust control is a regulatory and operational priority. Secondly, the system is highly efficient in terms of energy consumption, as it requires less power to operate compared to positive pressure systems. This translates into lower operational costs and increased profitability for the end-user. Thirdly, the system is capable of handling a wide range of wheat types and sizes, making it versatile for various processing applications. The gentle handling of the wheat particles also helps preserve the grain's quality, including its moisture content and nutritional value. Furthermore, the system's modular design allows for easy integration into existing processing lines, minimizing downtime during installation and maintenance.
Application and Operational Considerations
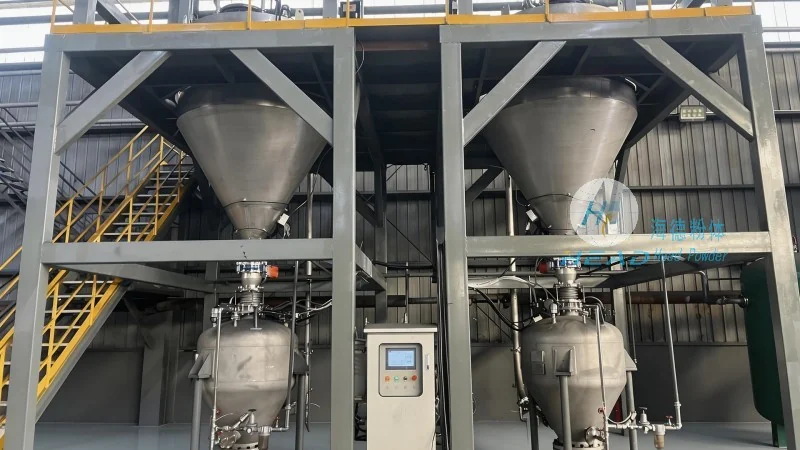
The negative pressure pneumatic conveying system is widely applicable in various stages of wheat processing, including storage, cleaning, and milling. It is particularly suitable for transferring wheat from storage silos to processing equipment, such as cleaners or grinders. The system's ability to handle large volumes of wheat at a consistent rate makes it ideal for high-throughput operations. Operational considerations include proper maintenance of the system's components, such as the vacuum pump and filter, to ensure continuous and reliable performance. Regular cleaning and inspection of the conveying lines are also essential to prevent blockages and maintain air quality. The system's design also allows for easy monitoring of operational parameters, such as pressure and flow rates, which helps in troubleshooting and optimizing performance. Additionally, the system's compact footprint makes it suitable for facilities with limited space, while still providing high conveying capacity.
Conclusion and Company Overview
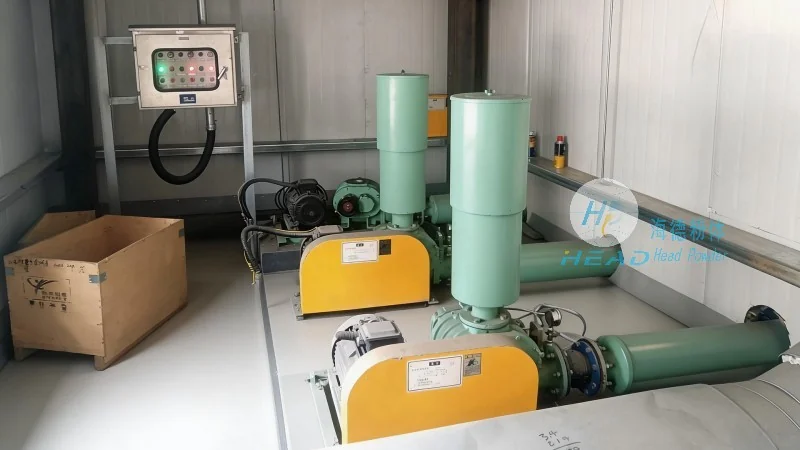
Shandong HeadPowder Engineering Co., Ltd. has demonstrated its expertise in designing and manufacturing advanced pneumatic conveying systems for wheat handling. The negative pressure system, as described, represents a cutting-edge solution that addresses the key challenges faced by modern wheat processing operations. By combining innovative engineering with high-quality materials and rigorous testing, the company ensures that its products meet the highest standards of performance and reliability. The system's benefits, including dust control, energy efficiency, and product preservation, make it a valuable asset for any wheat processing facility. With a strong commitment to customer satisfaction and continuous improvement, Shandong HeadPowder Engineering Co., Ltd. remains a trusted partner for businesses seeking to enhance their wheat handling capabilities. The company's headquarters is located in Shandong, China, where it continues to develop and refine its products to meet the evolving needs of the agricultural industry.




