

What is a Bicarbonate Powder Pneumatic Conveying System? And What Are Its Design Principles?
The bicarbonate powder pneumatic conveying system is a specialized industrial solution designed to transport dry powders, such as sodium bicarbonate (baking soda), through a pipeline using compressed air or other gas. This technology offers a clean, efficient, and often dust-free method for moving bulk materials, making it ideal for applications in food processing, chemical manufacturing, and pharmaceutical industries. The system's design focuses on ensuring minimal product degradation, maintaining product purity, and providing a flexible solution for various production needs.
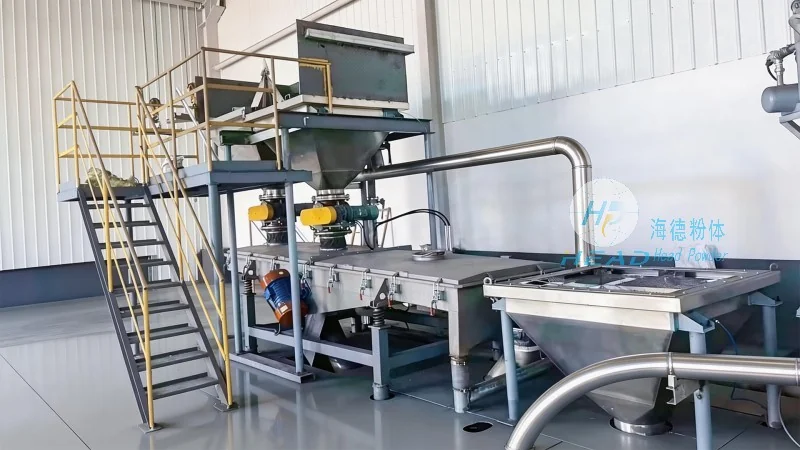
Understanding the Core Function of Pneumatic Conveying
At its essence, a pneumatic conveying system operates by creating a pressure differential between the material source and the destination. Compressed air is introduced into the system, which lifts and propels the powder particles through the pipeline. The system can be categorized into two main types: dilute-phase and dense-phase, each tailored to different material characteristics and conveying distances. For fine powders like bicarbonate, dilute-phase systems are commonly used due to their ability to handle high flow rates and long distances with minimal pressure drop.
Design Principles for Efficient Bicarbonate Powder Handling
The design of a bicarbonate powder pneumatic conveying system involves several critical principles to ensure optimal performance. First, the system must consider the particle size, density, and flowability of the powder. Bicarbonate is a fine, relatively light powder, which means the system needs to be designed to prevent particle segregation and ensure consistent flow. The pipeline diameter and material are also crucial; typically, stainless steel or food-grade materials are used to prevent contamination and corrosion. Additionally, the system incorporates features like cyclones or filters to separate the powder from the air stream, ensuring that the material reaches its destination without loss or contamination.
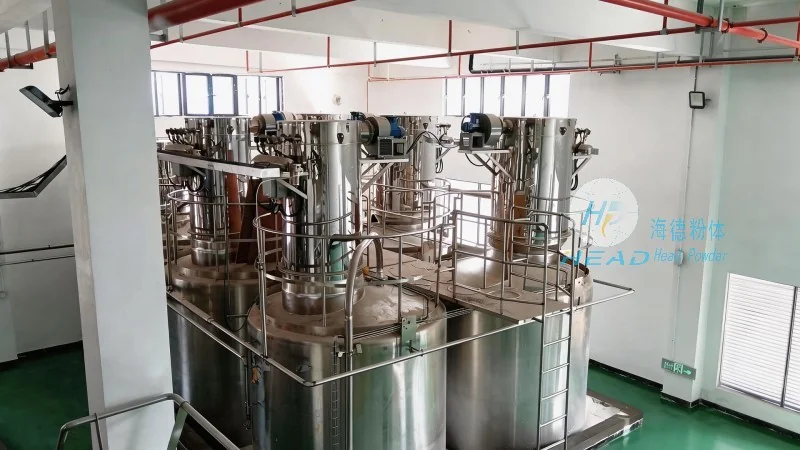
Key Components and Their Roles in the System
Several key components work together to make the pneumatic conveying system function effectively. The material hopper or feeder is the starting point, where the bicarbonate powder is stored and fed into the system. The feeder must be designed to maintain a consistent flow rate, preventing clogging or uneven discharge. The air compressor or blower provides the necessary pressure to move the powder through the pipeline. The pipeline itself is a critical component, with bends and fittings that are carefully designed to minimize pressure loss and prevent particle deposition. The receiving hopper or silo collects the powder at the end of the system, and often includes a dust collection system to capture any fine particles that may escape.
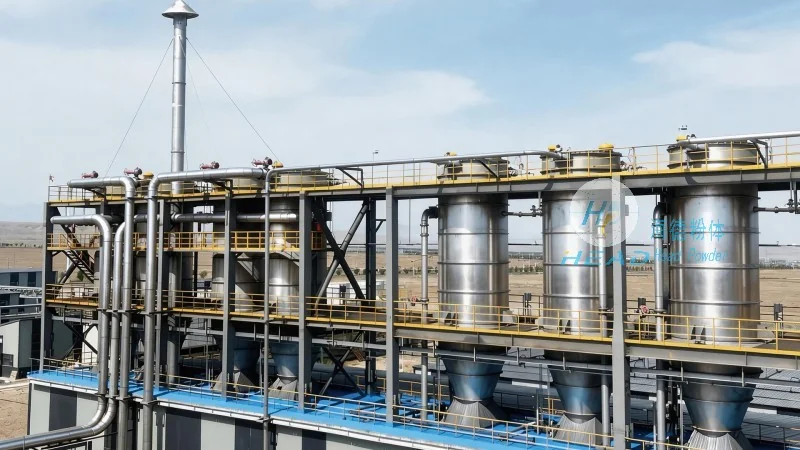
Application Scenarios and Benefits of the System
The bicarbonate powder pneumatic conveying system is widely used in various industries due to its advantages over traditional methods like belt conveyors or manual handling. In food processing, it allows for the safe and hygienic transfer of ingredients without cross-contamination. In chemical manufacturing, it reduces the risk of dust explosions by containing the powder in a closed system. The system also offers flexibility in terms of layout, as the pipeline can be installed in various configurations to fit the production facility's layout. Additionally, it reduces labor costs and improves production efficiency by automating the material handling process.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in industrial conveying systems. With headquarters in Shandong, China, the company has extensive experience in designing and manufacturing pneumatic conveying systems tailored to the needs of various industries. HeadPowder's commitment to quality and innovation ensures that their systems are reliable, efficient, and tailored to the specific requirements of each client. The company's expertise in material handling technology has made them a trusted partner for businesses seeking to improve their production processes and enhance operational efficiency.