

What is a Nanopowder Pneumatic Conveying System? And What Are Its Design Principles?
This section introduces the concept of a nanopowder pneumatic conveying system, explaining its purpose and significance in industrial applications. A nanopowder pneumatic conveying system is a specialized piece of equipment designed to transport fine powders, such as nanoparticles, through a pneumatic system. These systems are crucial in industries where handling ultra-fine powders requires precision and control. The design of such systems is tailored to address the unique challenges posed by nanopowders, including their high surface area, tendency to agglomerate, and sensitivity to moisture and contamination.
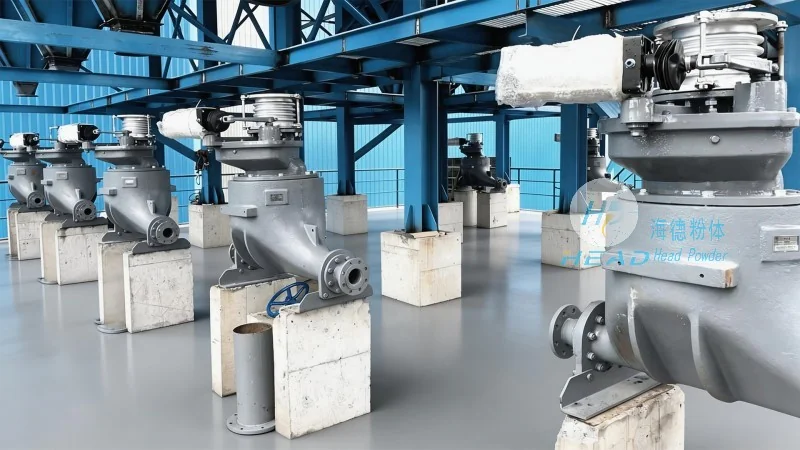
Understanding the Core Function of a Nanopowder Pneumatic Conveying System
The primary function of a nanopowder pneumatic conveying system is to transport dry powders, particularly nanoparticles, from one location to another using compressed air or other gas as the conveying medium. Unlike traditional bulk material handling methods, which often rely on mechanical components like belts or screws, pneumatic conveying systems use air flow to move particles through a pipeline. This method is especially advantageous for nanopowders because it minimizes particle degradation, reduces contamination risks, and allows for precise control over flow rates and particle distribution. The system typically consists of a hopper for powder storage, a feeder to control the powder flow, a conveying line, and a receiver to collect the transported powder.
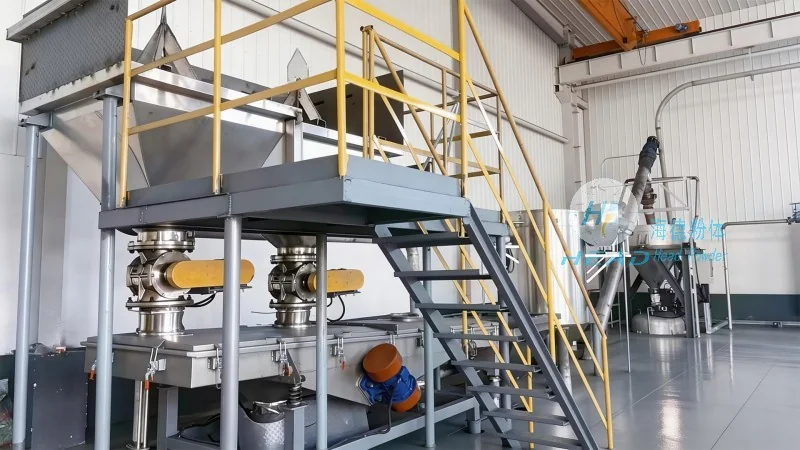
Key Design Principles Behind Nanopowder Pneumatic Conveying Systems
The design of a nanopowder pneumatic conveying system is governed by several critical principles to ensure efficient and reliable operation. First, the system must maintain a consistent air-to-powder ratio, which is crucial for preventing particle agglomeration and ensuring smooth flow. This ratio is carefully calculated based on the particle size, density, and moisture content of the nanopowder. Second, the conveying line must be designed to minimize pressure drop and energy consumption. This involves selecting appropriate pipe diameters, using smooth surfaces to reduce friction, and incorporating components like bends and elbows with low pressure loss. Third, the system must incorporate features to prevent particle segregation and maintain uniformity. This includes using inline mixers or agitators to keep the powder suspended and prevent settling. Additionally, the system is designed to handle variations in powder properties, such as changes in moisture content or particle size distribution, without compromising performance.
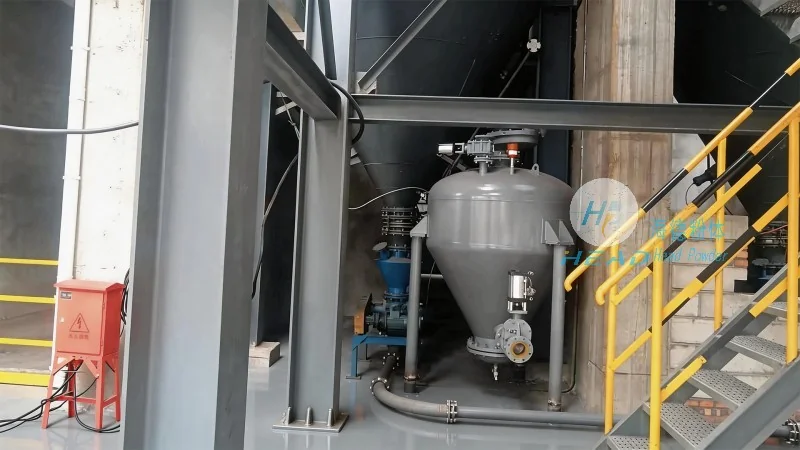
Technical Components and Their Roles in the System
Several key components work together to ensure the proper operation of a nanopowder pneumatic conveying system. The hopper serves as the storage vessel for the nanopowder, providing a stable and controlled source of material. It is typically equipped with a lid to prevent contamination and a discharge valve to regulate the powder flow. The feeder, often a rotary valve or a screw feeder, controls the rate at which powder is introduced into the conveying line. This component is critical for maintaining a consistent air-to-powder ratio and preventing overloading or underloading of the system. The conveying line, usually made of stainless steel or other corrosion-resistant materials, transports the powder and air mixture. The line is designed with appropriate bends and elbows to minimize pressure loss and ensure smooth flow. The receiver, or collection hopper, is where the transported powder is deposited. It is equipped with a dust collection system to capture any particles that may escape during the conveying process. Finally, the air compressor or blower provides the necessary pressure and flow rate to move the powder through the system. The compressor is typically sized to meet the system's air demand while minimizing energy consumption.
Application Scenarios and Industry Relevance
Nanopowder pneumatic conveying systems are widely used in various industries due to their ability to handle ultra-fine powders with precision and efficiency. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the powders remain sterile and free from contamination. In the chemical industry, they are used to handle catalysts, pigments, and other fine chemicals, where precise control over particle size and distribution is essential. The electronics industry also relies on nanopowder pneumatic conveying systems to transport materials like silicon powders and metal oxides, which are critical components in semiconductor manufacturing. Additionally, the food and beverage industry uses these systems to handle fine powders such as spices, flavorings, and nutritional supplements, where maintaining product quality and preventing cross-contamination is paramount. The versatility of nanopowder pneumatic conveying systems makes them indispensable in any industry where handling ultra-fine powders is required.
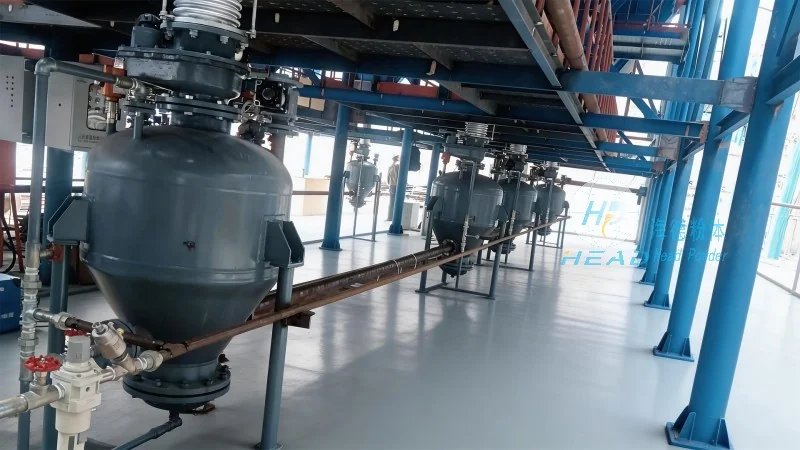
The Role of Shandong HeadPowder Engineering Co., Ltd. in the Field
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of nanopowder pneumatic conveying systems. The company specializes in designing and manufacturing customized solutions tailored to the specific needs of its clients. HeadPowder's expertise lies in understanding the unique challenges of nanopowder handling and developing systems that address these challenges effectively. The company's team of engineers and technicians work closely with clients to assess their requirements, provide technical consultations, and design systems that meet their operational needs. HeadPowder's products are known for their high quality, reliability, and efficiency, making them a trusted choice in the industry. The company's commitment to innovation and customer satisfaction has earned it a reputation as a leading provider of nanopowder pneumatic conveying systems. With its headquarters in Shandong, China, HeadPowder serves clients both domestically and internationally, providing comprehensive support and after-sales service to ensure the long-term performance of its systems.