HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced powder handling systems. This article explores the concept of negative pressure dilute phase powder conveying, detailing its operational principles and design considerations to help industry professionals understand this critical technology.
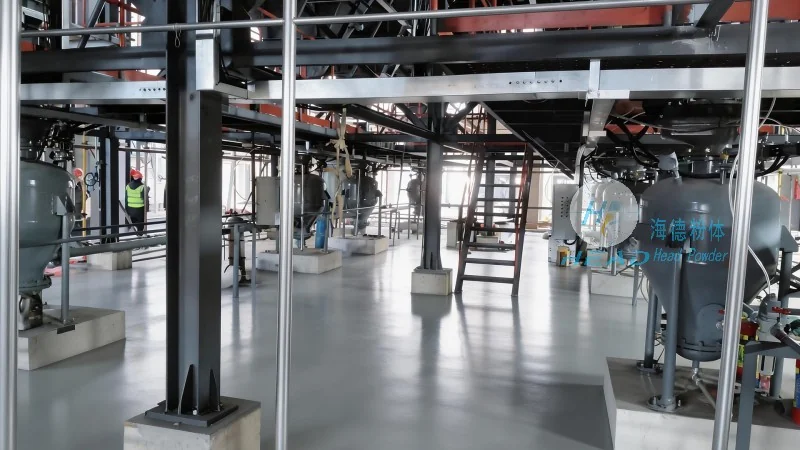
Understanding Negative Pressure Dilute Phase Powder Conveying
Negative pressure dilute phase powder conveying is a method used to transport dry powders and particulate materials through a pipeline system under a reduced pressure environment. Unlike positive pressure systems that force material through the pipeline, negative pressure systems create a vacuum or reduced pressure at the discharge end, drawing the material from the source into the conveying line. This approach is particularly effective for transporting materials over long distances or in applications where dust control and energy efficiency are paramount.
Key Design Principles of Negative Pressure Dilute Phase Conveying
The success of a negative pressure dilute phase system relies on several core design principles that ensure efficient and reliable material transport. These principles include proper selection of the conveying line diameter, the use of appropriate air velocity to maintain material suspension, and the implementation of effective dust collection and filtration systems. The system must also account for the specific properties of the material being conveyed, such as particle size, density, and moisture content, to optimize performance and prevent blockages or system failures.
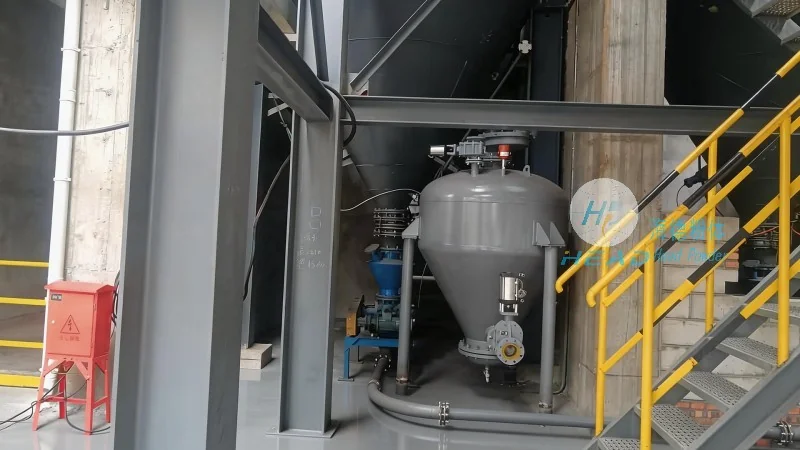
Components and Operational Flow
A typical negative pressure dilute phase powder conveying system consists of several key components. These include a material feeder to introduce the powder into the conveying line, a vacuum pump or fan to create the negative pressure, a conveying line that transports the material and air mixture, and a dust collector or filter to separate the material from the air at the discharge end. The operational flow begins with the material being fed into the line, where it is mixed with air to form a dilute suspension. The negative pressure generated by the vacuum pump draws this mixture through the pipeline, ensuring that the material is transported efficiently to the destination. At the discharge point, the material is separated from the air by the dust collector, and the cleaned air is then released back into the environment.
Advantages and Applications
Negative pressure dilute phase conveying offers several advantages over other powder handling methods. These include reduced energy consumption compared to positive pressure systems, lower material degradation due to less friction and impact, and improved safety by containing dust within the system. This technology is widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining, where the transport of fine powders is essential. For example, in the pharmaceutical industry, negative pressure systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high purity requirements, ensuring that the material remains uncontaminated during transport. In the food industry, such systems are employed to convey ingredients like flour, sugar, and spices, maintaining product quality and preventing cross-contamination.
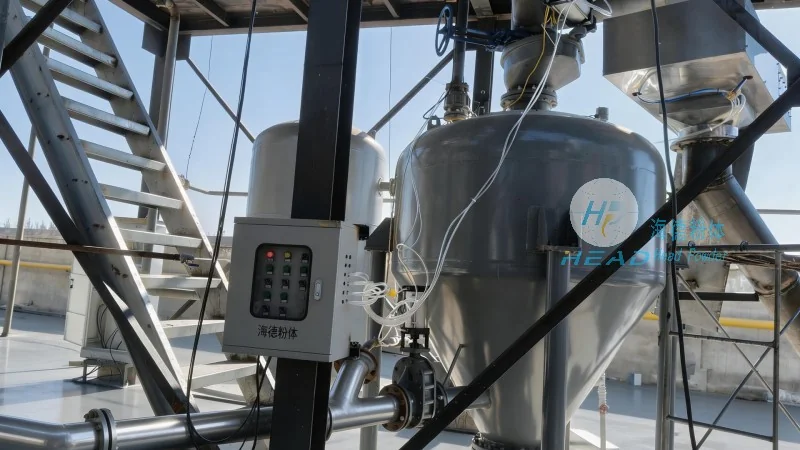
Design Considerations for Optimal Performance
Designing an effective negative pressure dilute phase conveying system requires careful consideration of several factors to ensure optimal performance and longevity. One critical factor is the selection of the appropriate conveying line diameter, which must be large enough to prevent excessive air velocity that could lead to material degradation or system wear. The air velocity within the line is another key parameter, typically ranging from 20 to 30 meters per second, depending on the material properties. Additionally, the system must incorporate adequate dust collection and filtration to prevent the release of fine particles into the environment, which is essential for compliance with environmental regulations and maintaining workplace safety.
Conclusion
Negative pressure dilute phase powder conveying is a sophisticated and efficient technology that plays a vital role in modern powder handling applications. By understanding its design principles and operational flow, industry professionals can select and implement systems that meet their specific material transport needs while ensuring safety, efficiency, and compliance with industry standards. As a leading provider of engineering solutions, HeadPowder continues to innovate in this field, offering tailored solutions that enhance productivity and reduce operational costs for its clients in Shandong and beyond.




