Tonne bag stainless steel powder conveying systems represent a specialized solution for the efficient and safe handling of bulk powders, particularly in industrial settings. These systems are engineered to manage the transportation of materials from large tonne bags into processing equipment or storage facilities. The design of such systems is critical to ensure reliability, durability, and compliance with industry standards, especially when dealing with materials that require high purity and resistance to contamination.
Design Principles of Stainless Steel Powder Conveying Systems
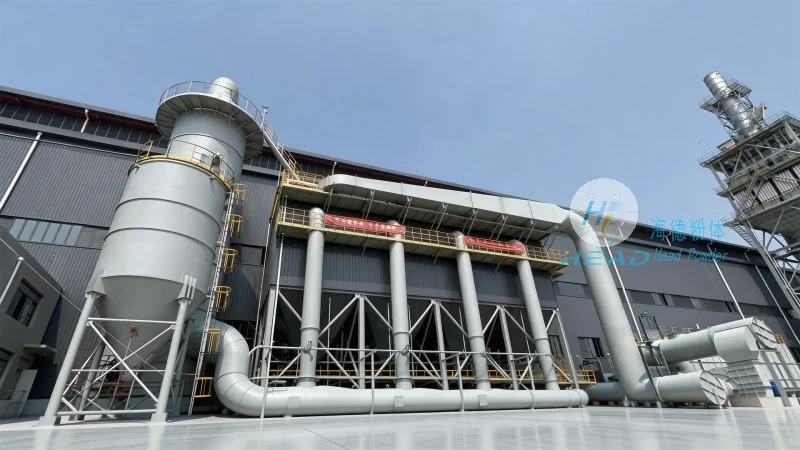
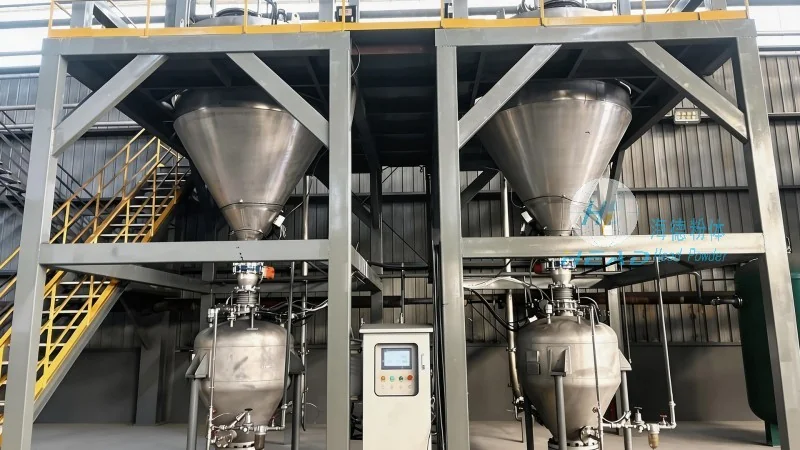
The core design principles of a tonne bag stainless steel powder conveying system revolve around several key elements. First, the system must be constructed from high-quality stainless steel components to prevent corrosion and maintain the integrity of the conveyed powder. Stainless steel is chosen for its non-reactive properties, ensuring that sensitive materials remain uncontaminated during transport. The system typically incorporates a hopper or receiving chamber that can accommodate the large tonne bags, often equipped with a discharge mechanism such as a valve or a lifting device to release the powder into the conveying line.
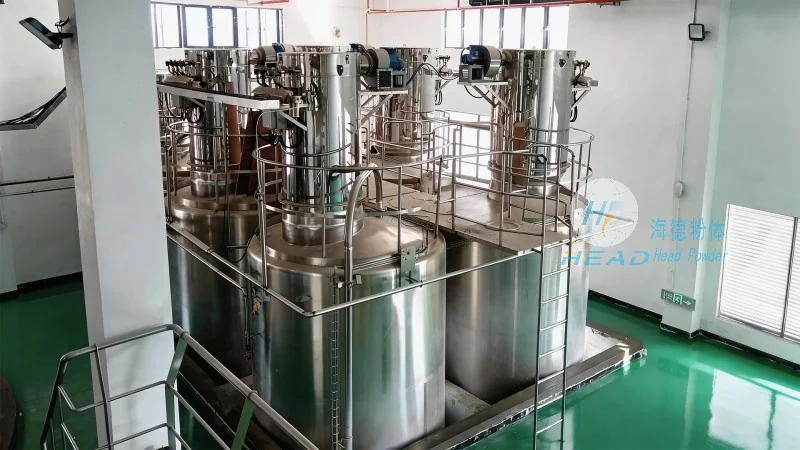
Conveying mechanisms are another critical aspect. Many systems use pneumatic or mechanical methods to move the powder. Pneumatic conveying, for instance, relies on air pressure to transport the material through a pipeline, while mechanical systems may employ screw conveyors or bucket elevators. The choice of mechanism depends on the powder's characteristics, such as density, flowability, and moisture content. Additionally, the system must include proper filtration and dust control measures to protect both the equipment and the environment from airborne particles.
Key Features and Advantages
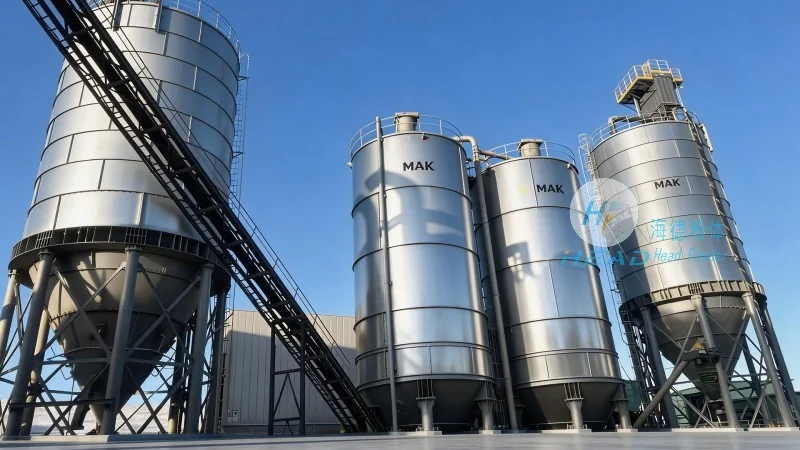
One of the primary advantages of tonne bag stainless steel powder conveying systems is their ability to handle large volumes of material efficiently. By eliminating manual handling of heavy tonne bags, these systems reduce labor costs and improve workplace safety. The stainless steel construction ensures long-term durability, minimizing maintenance and replacement costs over the system's lifespan. Furthermore, the enclosed design prevents dust emissions, making the operation more environmentally friendly and compliant with occupational health and safety regulations.
Application Scenarios
Tonne bag stainless steel powder conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and metal powders. In the pharmaceutical industry, for example, these systems are essential for handling active pharmaceutical ingredients (APIs) and excipients, where contamination control is paramount. In the food industry, they are used to transport ingredients like flour, sugar, and spices, ensuring that the product remains free from contaminants and maintains its quality. The chemical industry also benefits from these systems when handling reactive or hazardous powders, as the stainless steel construction provides a safe and secure environment.
Company Information
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized powder handling solutions. With operations based in Shandong, China, the company specializes in designing and manufacturing systems tailored to the unique needs of various industries. HeadPowder's expertise lies in creating efficient, reliable, and cost-effective powder conveying systems that meet the highest standards of quality and safety. The company's commitment to innovation and customer satisfaction has established it as a trusted partner in the powder handling sector.




