

What is a Catalyst Powder Material Handling System Equipment? What is Its Design Principle?
Catalyst powder material handling systems are critical components in industrial processes, particularly in chemical and pharmaceutical manufacturing. These systems are designed to efficiently transport, store, and manage catalyst powders, which are often used as key reagents in various chemical reactions. The proper design and operation of such systems are essential to ensure process efficiency, product quality, and safety. In this article, we will explore the fundamental aspects of catalyst powder material handling systems, including their design principles and the key factors that influence their performance.
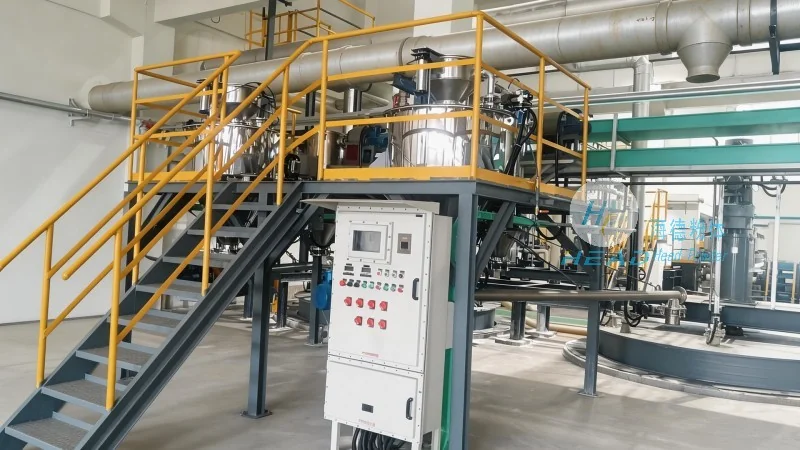
About HeadPowder: A Leading Provider of Material Handling Solutions
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier specializing in material handling equipment for powder and bulk materials. With a strong presence in China, particularly in Shandong, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient powder handling solutions. The company's expertise lies in designing customized systems that meet the specific needs of clients, ensuring optimal performance and compliance with industry standards.
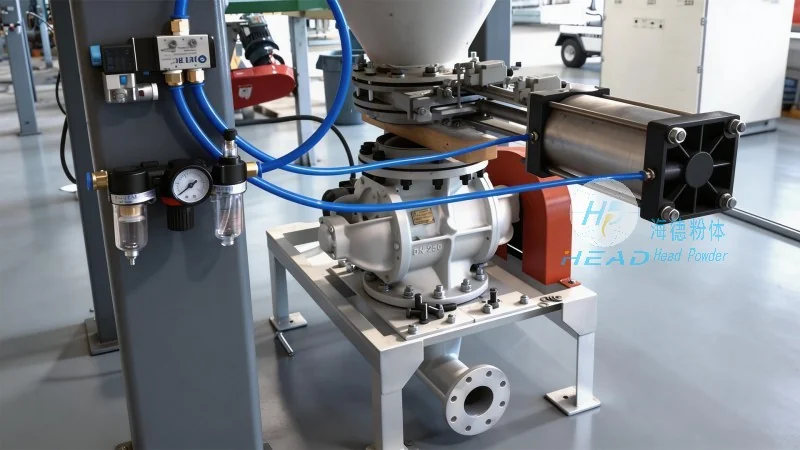
Design Principles of Catalyst Powder Material Handling Systems
The design of a catalyst powder material handling system involves several critical principles aimed at ensuring safety, efficiency, and reliability. First, the system must be designed to prevent dust generation and inhalation of fine particles, as catalyst powders can be hazardous if not handled properly. This is typically achieved through the use of enclosed conveying systems, such as pneumatic or mechanical conveyors, which minimize exposure to personnel. Second, the system must maintain consistent material flow and prevent segregation or agglomeration of the powder, which can affect the quality of the final product. This is achieved through the use of appropriate equipment, such as rotary valves, feeders, and mixers, which ensure uniform material distribution. Third, the system must be designed for easy maintenance and cleaning to prevent contamination and ensure long-term operation. This includes features like easy access to components, cleaning ports, and material discharge mechanisms.
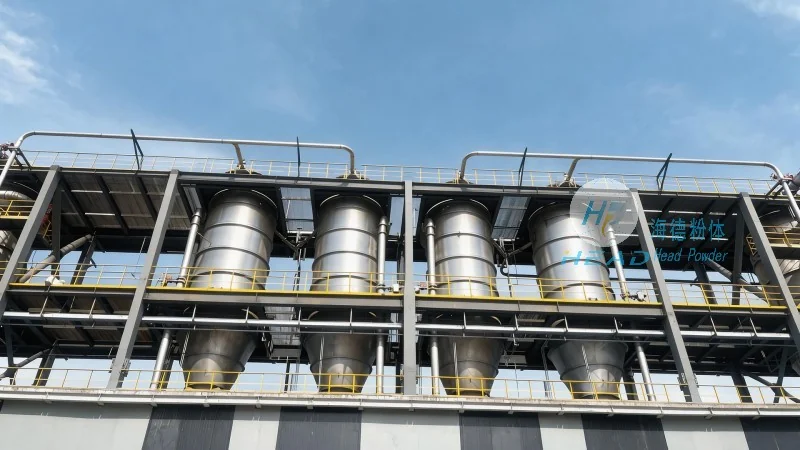
Key Components of a Catalyst Powder Material Handling System
A typical catalyst powder material handling system consists of several key components, each playing a crucial role in the overall operation. The primary components include: 1. Hopper or storage silo: This is the container where the catalyst powder is stored before being conveyed. It is designed to hold the material and provide a consistent feed to the conveyor system. 2. Conveying system: This is the core of the system, responsible for transporting the powder from the storage area to the processing equipment. Common types include pneumatic conveyors (using air pressure to move the material) and mechanical conveyors (using belts or screws to move the material). 3. Feeder: The feeder is used to control the flow rate of the powder from the hopper to the conveyor system, ensuring a consistent and controlled feed. 4. Diverter or rotary valve: This component is used to direct the material to the appropriate processing equipment or storage area, preventing backflow and ensuring proper material distribution. 5. Dust collection system: This is an essential safety feature that captures and filters the dust generated during the material handling process, ensuring a clean and safe working environment.
Applications and Benefits of Catalyst Powder Material Handling Systems
Catalyst powder material handling systems are widely used in various industries, including chemical manufacturing, pharmaceutical production, and petrochemical processing. The benefits of using such systems include improved process efficiency, reduced material waste, enhanced safety, and better product quality. By ensuring consistent material flow and preventing contamination, these systems help to maintain the integrity of the catalyst powder, which is critical for the success of the chemical reactions they are used in. Additionally, the use of enclosed systems reduces the risk of dust explosions and other safety hazards, making the operation safer for personnel.
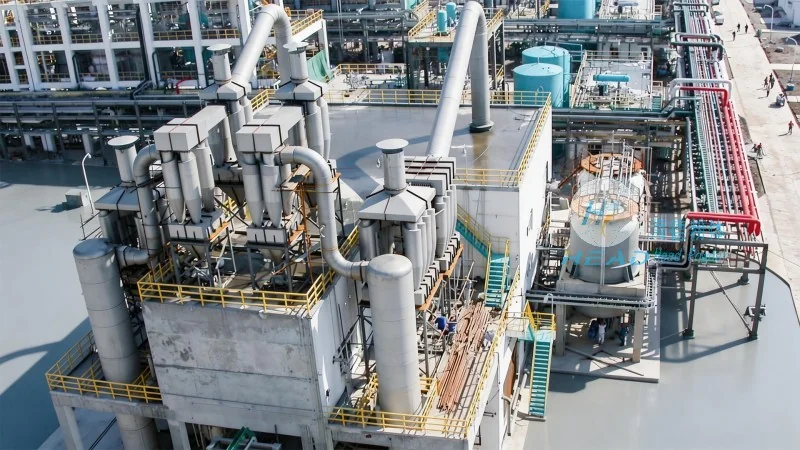
Conclusion and Contact Information
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers comprehensive solutions for catalyst powder material handling systems. With a focus on safety, efficiency, and reliability, the company's systems are designed to meet the specific needs of clients, ensuring optimal performance and compliance with industry standards. For more information or to discuss your material handling requirements, please contact HeadPowder at their address in Shandong, China.