HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and implementation of dense phase powder pneumatic conveying systems. These systems represent a sophisticated solution for the efficient and reliable transport of bulk powders over long distances or within complex industrial settings.
Understanding the Working Principle of Dense Phase Powder Pneumatic Conveying Systems
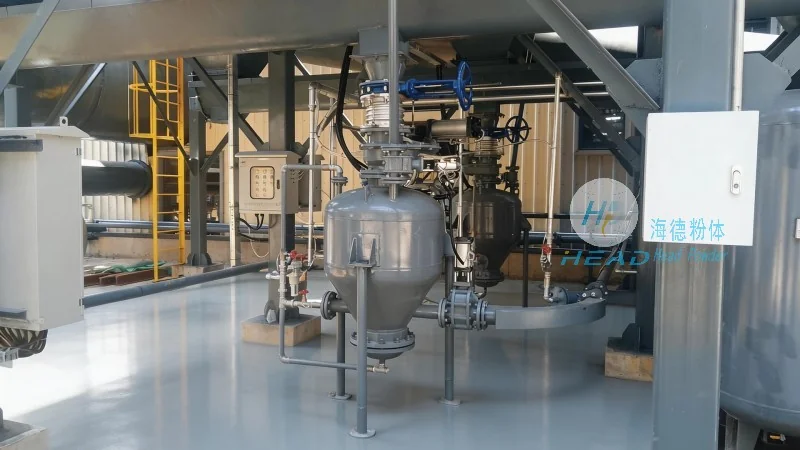
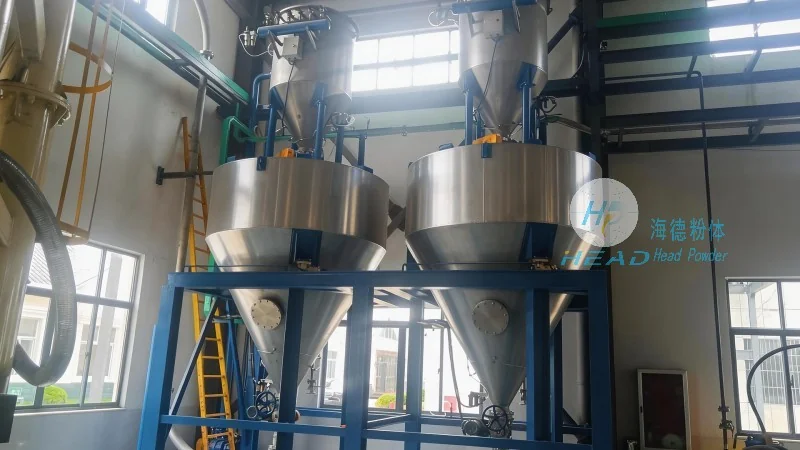
The core of dense phase powder pneumatic conveying lies in its ability to maintain a high concentration of powder within the conveying air stream. Unlike dilute phase systems that rely on low pressure and high air-to-powder ratios, dense phase systems operate under higher pressure conditions, typically using positive pressure or a combination of positive and negative pressure. This approach ensures that the powder particles remain suspended in a dense slurry-like mixture, minimizing the risk of particle segregation and blockages. The system typically comprises a hopper for material storage, a feeder to control the flow rate, a compressor or blower to generate the necessary pressure, and a pipeline network that transports the powder mixture to the destination. The air pressure is carefully regulated to maintain the optimal powder concentration, ensuring smooth and continuous operation. As the mixture travels through the pipeline, the high pressure helps to keep the particles in suspension, preventing them from settling and causing clogs. The destination equipment, such as a silo or processing unit, is equipped with a receiver to separate the powder from the air, often through a cyclone or filter system. This separation process is crucial for maintaining the purity of the conveyed material and ensuring the efficiency of the overall system.
Key Characteristics of Dense Phase Powder Pneumatic Conveying Systems
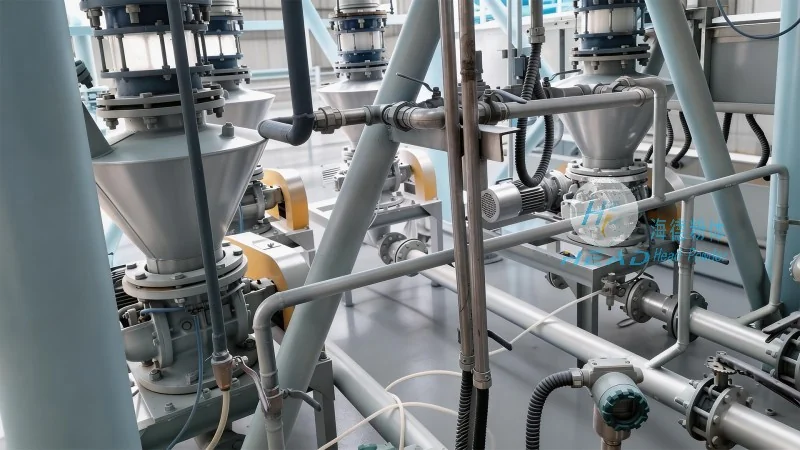
Dense phase powder pneumatic conveying systems are distinguished by several critical characteristics that make them ideal for demanding industrial applications. First, they offer high efficiency in material transport, capable of moving large volumes of powder over significant distances with minimal energy consumption compared to other methods like truck or rail transport. The high pressure operation ensures that the conveying velocity is sufficient to prevent particle settling, reducing the need for frequent maintenance and downtime. Second, these systems provide excellent adaptability to various powder types, including fine, cohesive, or abrasive materials, which are often challenging to handle with conventional conveying methods. The dense phase environment helps to maintain the integrity of the powder, preventing agglomeration or degradation during transport. Third, dense phase systems are designed to minimize dust emissions and environmental impact. By keeping the powder in a concentrated stream, the system reduces the amount of airborne particles, contributing to better workplace safety and compliance with environmental regulations. Additionally, the positive pressure operation can be integrated with dust collection systems, further enhancing air quality and operational safety. Fourth, the systems offer flexibility in layout and integration with existing industrial infrastructure. They can be configured to handle multiple material sources or destinations, and can be easily adapted to accommodate changes in production requirements or facility expansions. The modular design of dense phase systems allows for scalability, making them suitable for both small-scale operations and large-scale industrial plants. Finally, the reliability of dense phase conveying is enhanced by the use of robust components, such as high-quality compressors, durable pipelines, and advanced control systems. These components are engineered to withstand the high pressures and abrasive nature of the conveyed materials, ensuring long-term performance and reduced maintenance costs. Overall, the combination of efficiency, adaptability, and reliability makes dense phase powder pneumatic conveying an attractive solution for industries that require consistent and high-quality material transport.
Applications and Benefits in Industrial Settings
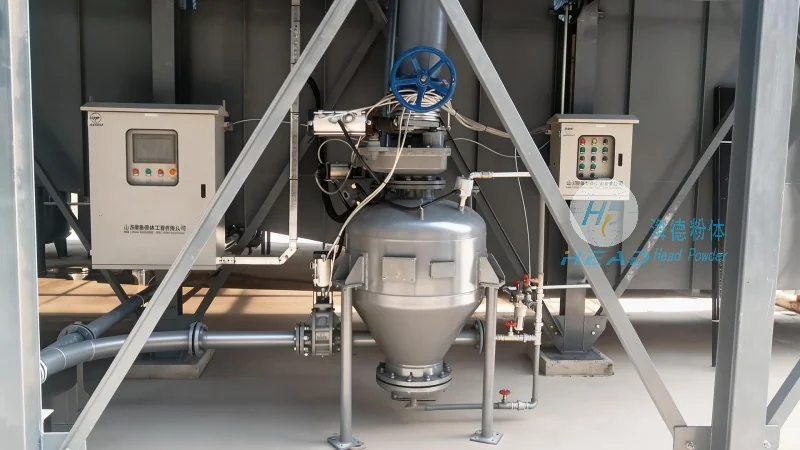
Dense phase powder pneumatic conveying systems are widely used across various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, for example, these systems are essential for transporting active pharmaceutical ingredients (APIs) and other sensitive powders, where contamination and particle degradation must be strictly avoided. The high pressure and controlled environment of dense phase conveying ensure that the powders remain pure and intact throughout the process. In the food industry, dense phase systems are used to transport ingredients like flour, sugar, and spices, maintaining their quality and preventing cross-contamination. The ability to handle cohesive and fine powders makes them ideal for food processing applications where hygiene and product integrity are paramount. In chemical manufacturing, dense phase conveying is used for transporting raw materials and intermediates, often in high-temperature or corrosive environments. The robust design of the systems allows them to withstand harsh conditions, ensuring safe and efficient material handling. In the mining sector, dense phase systems are employed to transport ore and other bulk materials from processing plants to storage facilities or for further processing. The high efficiency and reliability of these systems help to optimize mining operations and reduce transportation costs. The benefits of dense phase powder pneumatic conveying extend beyond individual applications, contributing to overall operational efficiency and cost savings. By eliminating the need for manual handling or traditional bulk transport methods, these systems reduce labor costs and minimize the risk of accidents or material loss. The consistent and reliable transport of powders also improves production throughput and reduces downtime, leading to increased profitability for industrial operations. Furthermore, the environmental benefits of reduced dust emissions and lower energy consumption make dense phase systems a sustainable choice for modern industry. In summary, dense phase powder pneumatic conveying systems offer a comprehensive solution for the efficient and safe transport of bulk powders, addressing the diverse needs of various industrial sectors while providing long-term operational advantages.




