HeadPowder, a leading provider of powder handling solutions, specializes in the design and manufacturing of advanced pneumatic conveying systems. This article focuses on the small bag quantitative feeding powder pneumatic conveying machine, exploring its operational principles and typical application scenarios. The company, Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China, and is dedicated to delivering efficient and reliable equipment for various industrial sectors.
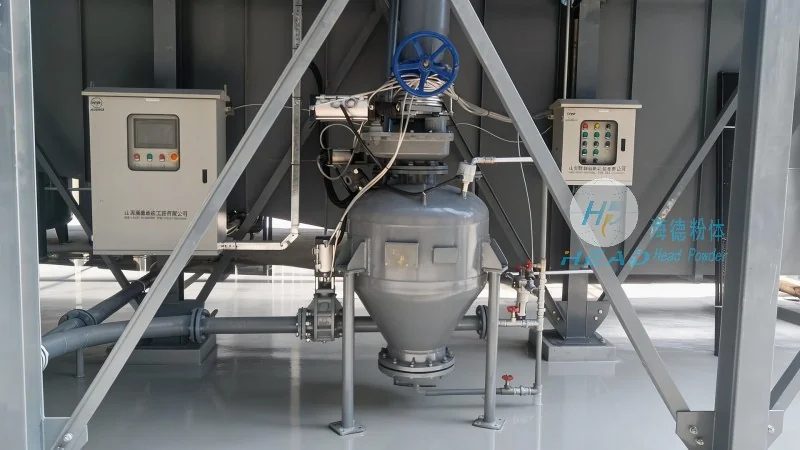
Overview of the Small Bag Quantitative Feeding Powder Pneumatic Conveying Machine
The small bag quantitative feeding powder pneumatic conveying machine is a specialized device designed to handle bulk powders with precision and efficiency. It is particularly suitable for applications where accurate dosing and controlled material transfer are critical. This system integrates a small bag feeding mechanism with a pneumatic conveying pipeline, enabling seamless and automated powder handling. The machine is engineered to minimize material loss, reduce contamination risks, and maintain consistent flow rates, making it ideal for industries such as pharmaceuticals, food processing, and chemical manufacturing.
Working Principle of the Machine
The core principle of the small bag quantitative feeding powder pneumatic conveying machine involves the controlled release of powder from a small bag into a pneumatic conveying system. The process typically begins with the placement of a small bag containing the powder into the feeding hopper. The machine then uses a mechanical or pneumatic mechanism to open the bag and release the material in measured quantities. The released powder is then drawn into the conveying pipeline by a vacuum or pressure source, depending on the system configuration. The machine is equipped with sensors and control systems to ensure precise dosing, preventing over or under feeding. This automated process eliminates manual handling, reducing human error and enhancing operational safety.
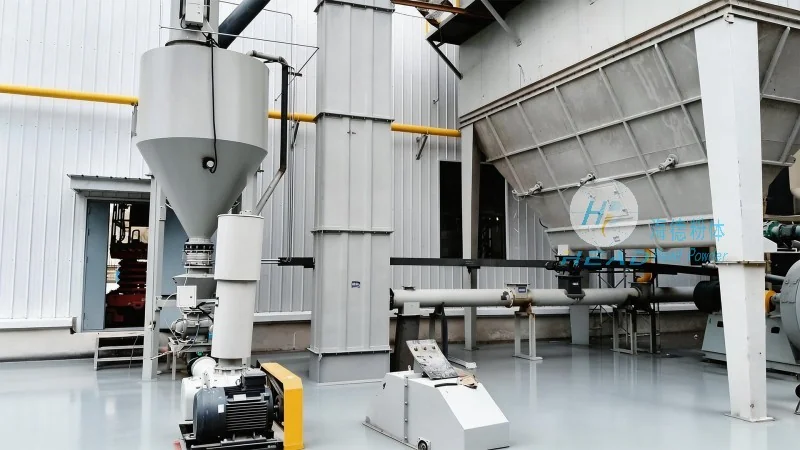
Key Components and Their Functions
The small bag quantitative feeding powder pneumatic conveying machine consists of several key components that work in tandem to achieve efficient operation. The primary components include the small bag feeding hopper, the bag opening mechanism, the pneumatic conveying pipeline, the air supply system, and the control unit. The small bag feeding hopper is designed to hold the small bags securely and facilitate easy access for the bag opening mechanism. The bag opening mechanism, which can be mechanical (e.g., a cutting blade) or pneumatic (e.g., a compressed air jet), is responsible for opening the bag and releasing the powder. The pneumatic conveying pipeline transports the powder from the hopper to the discharge point, using either vacuum or pressure to move the material. The air supply system provides the necessary airflow, and the control unit manages the entire process, including dosing, timing, and safety features. Each component is carefully engineered to ensure durability, reliability, and minimal maintenance requirements.
Working Scene Characteristics and Application Scenarios
The small bag quantitative feeding powder pneumatic conveying machine is well-suited for a variety of industrial applications where precise powder handling is essential. One common application is in the pharmaceutical industry, where the machine is used to transfer active pharmaceutical ingredients (APIs) and excipients with high accuracy, ensuring compliance with regulatory standards. In the food processing sector, the machine is ideal for handling food-grade powders such as sugar, flour, and spices, maintaining hygiene and preventing contamination. The chemical industry also benefits from this equipment, as it can handle various chemical powders, including catalysts and reagents, with precision. Additionally, the machine is suitable for use in research and development laboratories, where small-scale, controlled powder transfers are required. The working scene characteristics of this machine include its compact design, which allows for installation in limited spaces, and its ability to handle a wide range of powder types, from fine to coarse particles. The system is also designed for easy integration into existing production lines, minimizing downtime and enhancing overall operational efficiency.
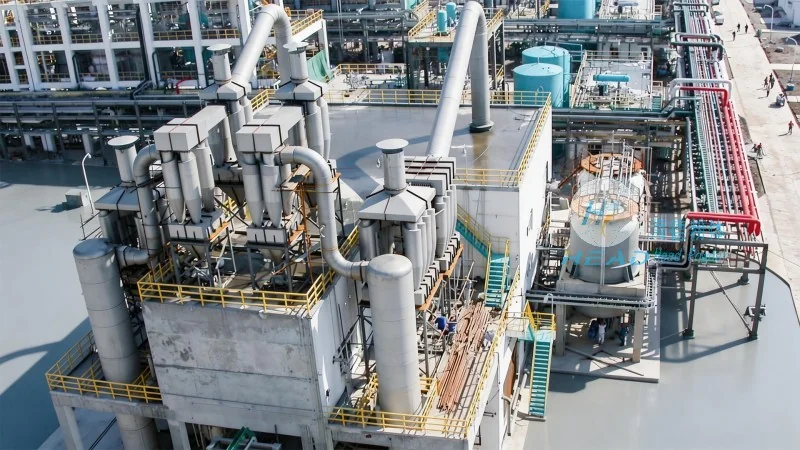
Advantages and Benefits of the Small Bag Quantitative Feeding Powder Pneumatic Conveying Machine
Implementing the small bag quantitative feeding powder pneumatic conveying machine offers several advantages and benefits for industrial operations. One of the key benefits is the high level of precision in powder dosing, which reduces material waste and improves product consistency. The automated process also increases operational efficiency by eliminating manual labor, allowing for continuous and uninterrupted production. Additionally, the machine minimizes contamination risks, as it prevents direct human contact with the powder and uses sealed systems to maintain hygiene standards. The compact design of the machine makes it suitable for installation in various environments, including production facilities with limited space. The system is also designed for easy maintenance, with accessible components that can be serviced quickly, reducing downtime and maintenance costs. Overall, the small bag quantitative feeding powder pneumatic conveying machine enhances productivity, improves product quality, and ensures compliance with industry regulations.
Conclusion
HeadPowder's small bag quantitative feeding powder pneumatic conveying machine is a reliable and efficient solution for precise powder handling in various industrial applications. The machine's operational principles, combined with its advanced components and design, make it an ideal choice for industries requiring accurate and controlled material transfer. With its ability to handle a wide range of powders and its compact design, the machine enhances operational efficiency and product quality. HeadPowder, as a leading manufacturer based in Shandong, China, continues to innovate and provide high-quality equipment that meets the evolving needs of the industry. The small bag quantitative feeding powder pneumatic conveying machine represents a significant advancement in powder handling technology, offering benefits such as precision, efficiency, and safety.




