HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems. This article focuses on the principle and working scene characteristics of a tonne bag quantitative feeding material pneumatic conveying system, highlighting its technical advantages and practical applications in various industrial settings.
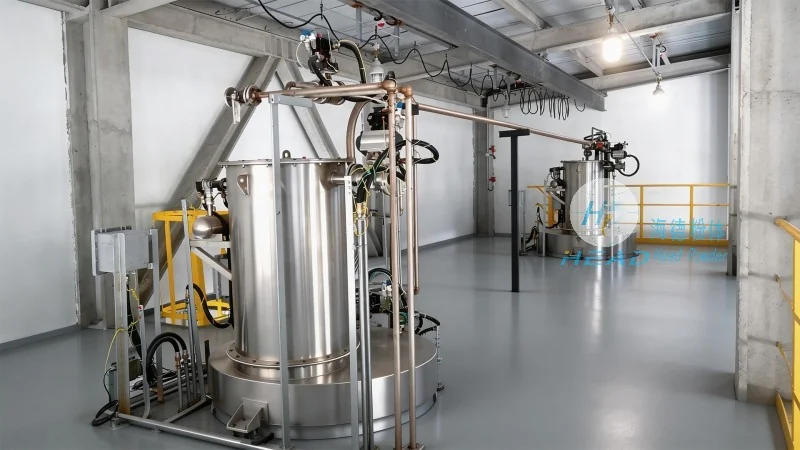
System Overview and Core Components
The tonne bag quantitative feeding material pneumatic conveying system is engineered to efficiently transfer bulk materials from storage containers, such as tonne bags, into processing equipment. The system integrates several key components that work in tandem to ensure precise material handling and consistent performance. These components typically include a feeding hopper, a rotary valve or feeder, a pneumatic conveying line, and a receiver or discharge unit. Each component plays a critical role in the overall operation, contributing to the system's reliability and efficiency.
Working Principle of the Pneumatic Conveying System
The fundamental principle of this system is the use of compressed air to transport bulk materials in a fluidized or suspended state. The process begins with the material being discharged from a tonne bag into a feeding hopper. The hopper is equipped with a rotary valve or feeder that controls the flow rate of the material into the conveying line. Compressed air is then introduced into the line, creating a pressure differential that propels the material through the pipeline. The material is carried as a slurry or suspension, ensuring minimal degradation and loss of product quality. The system's design allows for precise control over the feeding rate, which is crucial for maintaining consistent production processes.
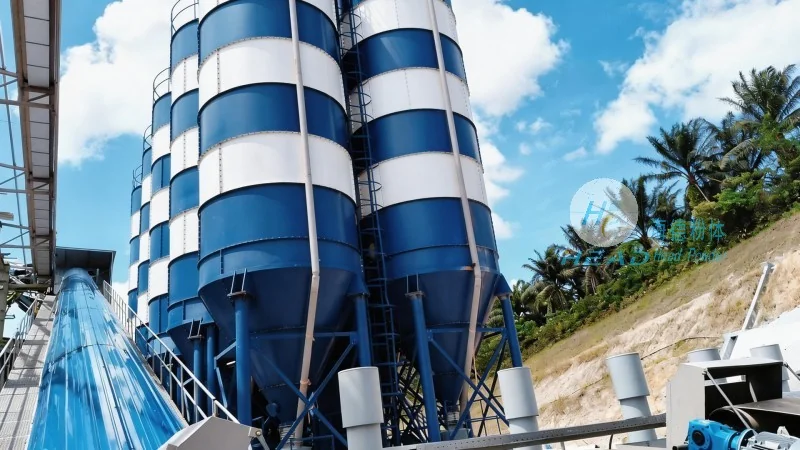
Key Technical Advantages
One of the primary advantages of the tonne bag quantitative feeding material pneumatic conveying system is its ability to handle a wide range of bulk materials, including powders, granules, and fine particles. The system is designed to minimize material degradation, dust generation, and product contamination, which is essential for industries where product quality is paramount. Additionally, the system offers high throughput and low maintenance requirements, making it a cost-effective solution for large-scale material handling operations. The quantitative feeding feature ensures that the exact amount of material is delivered to the processing equipment, reducing waste and improving operational efficiency.
Working Scene Characteristics and Applications
The tonne bag quantitative feeding material pneumatic conveying system is particularly well-suited for applications in the chemical, pharmaceutical, food, and mining industries. In these sectors, the system is used to transfer materials such as chemicals, powders, and minerals from storage to processing units. The system's ability to handle large volumes of material in a controlled manner makes it ideal for high-demand production environments. For example, in the chemical industry, the system can be used to feed raw materials into reactors or mixers, ensuring consistent batch processing. In the food industry, the system is used to transfer ingredients into processing lines, maintaining hygiene and product integrity. The system's flexibility and adaptability to different material types and process requirements make it a versatile solution for various industrial applications.
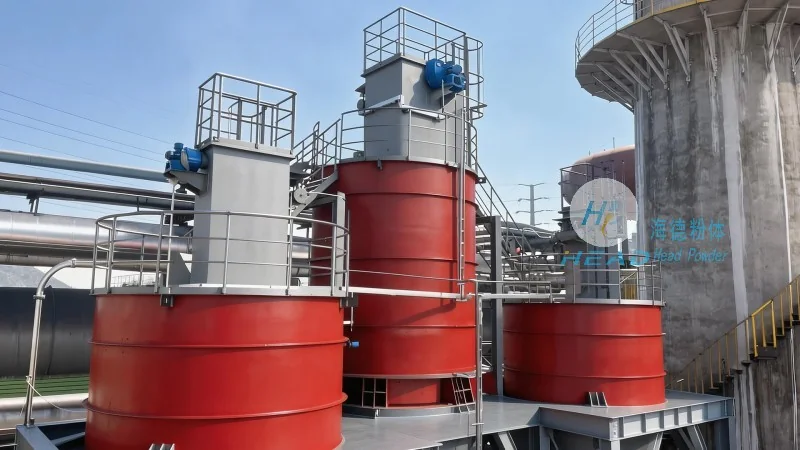
Operational Efficiency and Maintenance Considerations
The tonne bag quantitative feeding material pneumatic conveying system is designed for high operational efficiency, with features that minimize downtime and maximize productivity. The system's quantitative feeding mechanism allows for precise control over material input, reducing overfeeding or underfeeding that can impact process performance. The use of high-quality materials and components ensures long-term reliability and reduces the need for frequent maintenance. Regular maintenance, such as cleaning the conveying line and checking the performance of the rotary valve, is essential to maintain the system's efficiency. HeadPowder provides comprehensive maintenance services and support to ensure that the system operates at optimal levels, minimizing disruptions to production.
Conclusion
The tonne bag quantitative feeding material pneumatic conveying system is a sophisticated and efficient solution for bulk material handling in various industrial applications. By leveraging the principles of pneumatic conveying and precise quantitative feeding, the system offers numerous advantages, including high throughput, minimal material degradation, and improved operational efficiency. With its adaptability to different material types and process requirements, the system is a valuable asset for industries seeking reliable and cost-effective material handling solutions. HeadPowder, with its expertise in industrial engineering, continues to provide innovative solutions that meet the evolving needs of modern industrial operations.




