HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced air-lifted systems for handling micron powder materials. This article explores the fundamental principles behind these systems and highlights the key operational scenarios where they excel in material transport and processing.
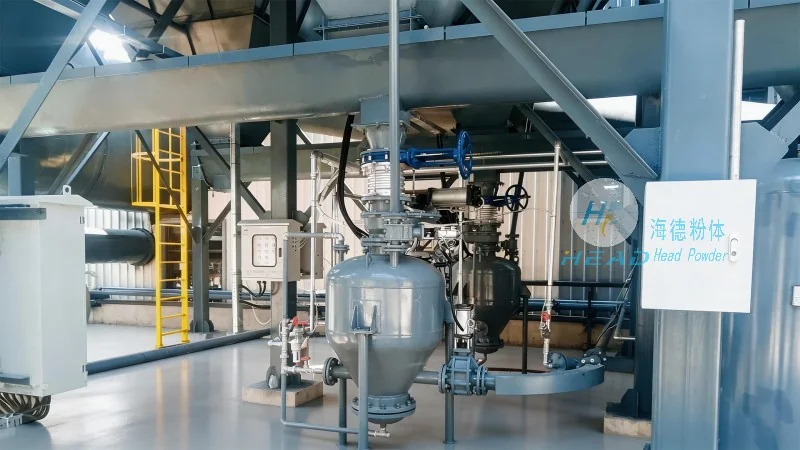
The Working Principle of Air-Lifted Micron Powder Transporters
At the core of air-lifted micron powder handling equipment is the utilization of air pressure and flow dynamics to move fine powders through a pipeline system. The process typically involves a blower or compressor that generates a high-velocity air stream, which draws the powder particles into the conveying line. The micron powder, characterized by its extremely fine particle size (often below 100 microns), requires specialized handling techniques due to its high surface area and potential for dust generation. The air-lifted system employs a Venturi or suction mechanism to create a negative pressure zone, effectively pulling the powder particles along with the air flow. This method ensures efficient and dust-free transport, minimizing product contamination and environmental impact.
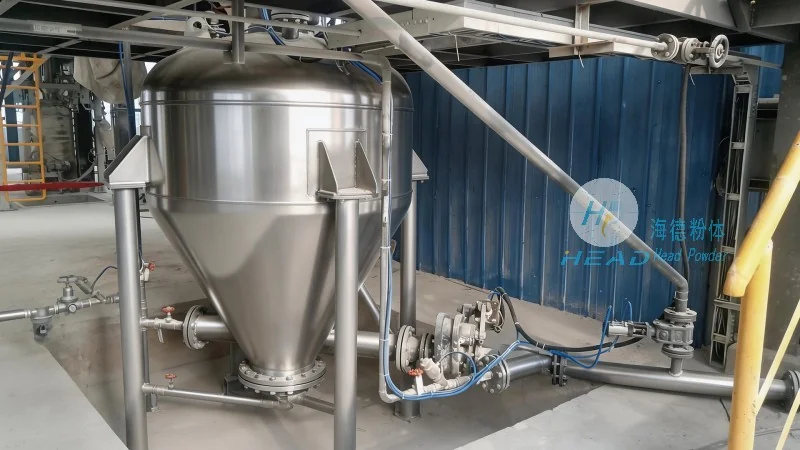
Key Features and Advantages of Micron Powder Air-Lifted Systems
HeadPowder's air-lifted micron powder transporters offer several distinct advantages over traditional mechanical conveying methods. Firstly, they eliminate the need for moving parts in contact with the powder, reducing wear and tear and extending equipment lifespan. Secondly, the system is highly flexible, allowing for vertical, horizontal, or inclined transport paths, making it suitable for complex facility layouts. Thirdly, air-lifted systems provide excellent control over particle flow, enabling precise dosing and batching for sensitive applications. Additionally, these systems are capable of handling abrasive or corrosive powders without compromising performance, thanks to the use of high-quality materials such as stainless steel or special coatings. The energy efficiency of air-lifted transport is also noteworthy, as the air flow can be optimized to minimize power consumption while maintaining optimal conveying rates.
Common Working Scenarios and Industry Applications
The versatility of air-lifted micron powder handling equipment makes it indispensable in various industrial sectors. In the pharmaceutical industry, for example, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements, ensuring that the powder remains free from contamination during transport. The food and beverage sector also benefits from air-lifted systems when handling fine powders like cocoa, sugar, or flavorings, where maintaining product quality and preventing cross-contamination is critical. In the chemical industry, the equipment is employed to convey reactive or hazardous powders, such as catalysts or pigments, with enhanced safety features that include explosion-proof designs and dust explosion suppression systems. Furthermore, in the mining and mineral processing industries, air-lifted transporters are used to move fine ore powders from processing plants to storage or further treatment facilities, improving operational efficiency and reducing labor costs.
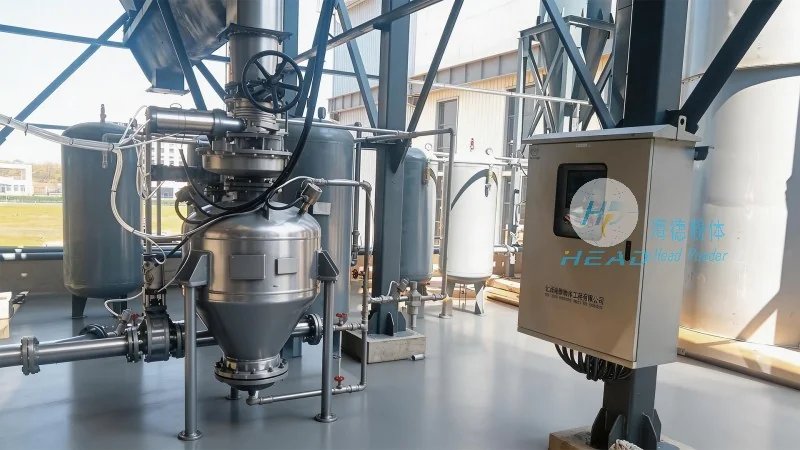
Customization and Integration Capabilities
HeadPowder understands that each industrial application has unique requirements, and thus offers customized air-lifted micron powder handling solutions tailored to specific needs. The company's engineering team works closely with clients to design systems that meet exact conveying capacities, particle size specifications, and environmental standards. Integration with existing production lines is seamless, as the air-lifted equipment can be connected to existing blower systems or control panels without major modifications. Additionally, HeadPowder provides comprehensive after-sales support, including maintenance services, spare parts availability, and technical assistance, ensuring that clients can rely on the equipment for long-term, reliable operation.




