

Stearic Acid Sodium Pneumatic Conveying: A Solution for Material Transport Beyond Distance Limits
Stearic acid sodium, a widely used chemical additive in various industries, often requires efficient and reliable transport methods to meet production demands. Traditional material handling systems may face limitations when dealing with long-distance or complex route requirements. This is where pneumatic conveying technology emerges as a superior solution, enabling seamless material transport while maintaining product integrity and operational efficiency.
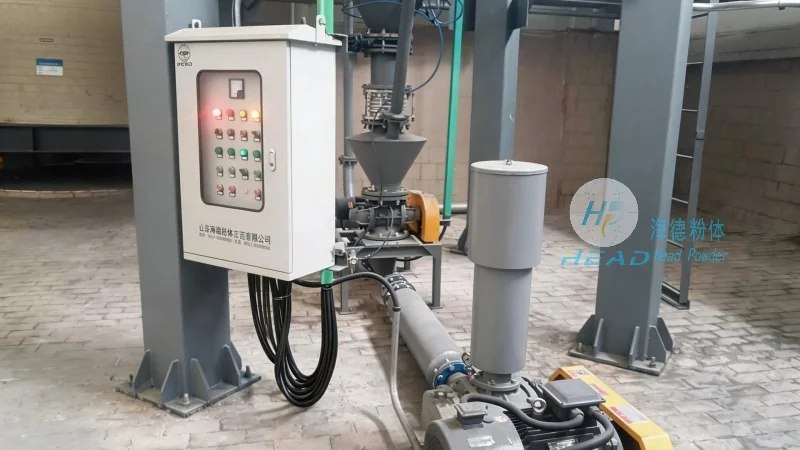
Understanding Pneumatic Conveying for Stearic Acid Sodium
Pneumatic conveying, also known as air conveying, utilizes a pressurized or vacuum system to transport bulk materials through a pipeline. For stearic acid sodium, which is typically in powder or granular form, this method offers several advantages over conventional methods like belt conveyors or bucket elevators. The primary benefit is the ability to transport materials over extended distances without the need for multiple transfer points, thus reducing operational complexity and maintenance costs.
HeadPowder Engineering: Pioneering Advanced Pneumatic Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and implementing customized pneumatic conveying systems tailored to the unique needs of stearic acid sodium applications. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for industries relying on consistent and high-quality material transport. The company’s expertise lies in integrating advanced technology with practical engineering solutions to ensure optimal performance and reliability.
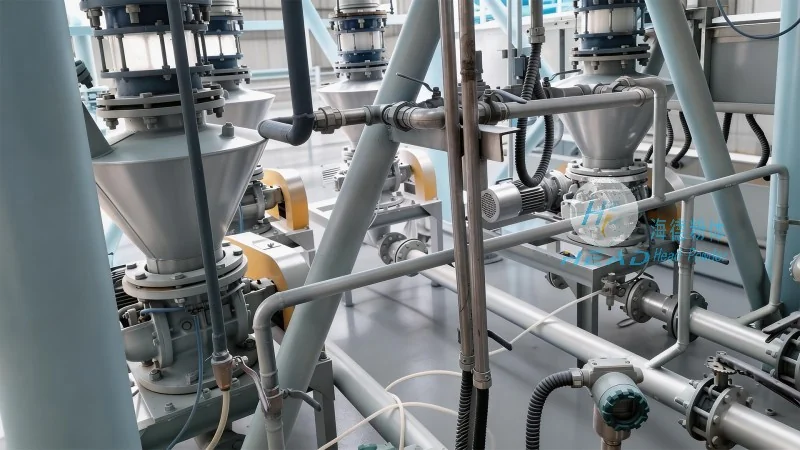
Key Features of HeadPowder's Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems for stearic acid sodium are engineered with precision to address the specific challenges of handling this chemical. Key features include:
- Flexible Pipeline Design: Customizable pipeline configurations that adapt to various site layouts and distance requirements, ensuring efficient material flow without bottlenecks.
- Advanced Air Control Systems: Sophisticated air pressure and flow control mechanisms that maintain consistent material velocity, preventing degradation or agglomeration of the stearic acid sodium particles.
- Material Compatibility: Materials are designed to be compatible with stearic acid sodium, minimizing the risk of contamination and ensuring product purity throughout the transport process.
- Energy Efficiency: Optimized air consumption and system design that reduces operational costs while maintaining high transport efficiency.
Benefits of Choosing HeadPowder's Pneumatic Conveying Solutions
Implementing HeadPowder's pneumatic conveying systems for stearic acid sodium offers numerous benefits for industrial operations. These include:
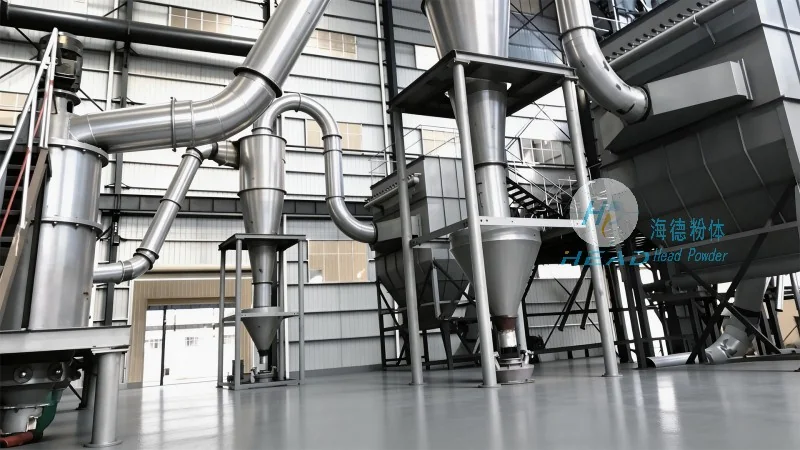
- Enhanced Product Integrity: The enclosed system prevents exposure to external contaminants, moisture, or air, preserving the quality and stability of the stearic acid sodium during transport.
- Increased Operational Efficiency: Reduced downtime due to fewer transfer points and lower maintenance requirements, leading to higher overall productivity.
- Cost-Effective Long-Distance Transport: Eliminates the need for additional equipment or infrastructure for long-distance material movement, providing a cost-effective solution for extended transport needs.
- Scalability and Adaptability: Systems can be easily scaled or modified to accommodate changes in production volume or operational requirements, ensuring long-term suitability.
Application Scenarios and Industry Impact
HeadPowder's pneumatic conveying solutions for stearic acid sodium are applied across various industries, including food processing, pharmaceuticals, and chemical manufacturing. In these sectors, the consistent and reliable transport of stearic acid sodium is crucial for maintaining production continuity and product quality. By leveraging HeadPowder's expertise, companies can achieve seamless material handling, reduce operational risks, and enhance overall production efficiency.
Conclusion and Future Outlook
As industries continue to demand more efficient and reliable material transport solutions, pneumatic conveying technology, particularly for specialized chemicals like stearic acid sodium, remains a critical advancement. Shandong HeadPowder Engineering Co., Ltd. stands at the forefront of this technology, providing innovative and tailored solutions that address the unique challenges of modern industrial operations. With a commitment to quality, innovation, and customer satisfaction, HeadPowder continues to be a key player in revolutionizing material handling for the stearic acid sodium market.