Bulk bag unloading station powder conveying machines are critical equipment in industries that handle bulk materials, such as chemicals, food, and pharmaceuticals. These systems are designed to efficiently transfer powders from bulk bags into storage silos or processing equipment. The operation of these machines involves several key steps and principles that ensure safe, reliable, and consistent material handling. This article will explore the detailed operation process and working principles of bulk bag unloading station powder conveying machines, highlighting the technology and components that make them effective.
Key Components of the Bulk Bag Unloading Station
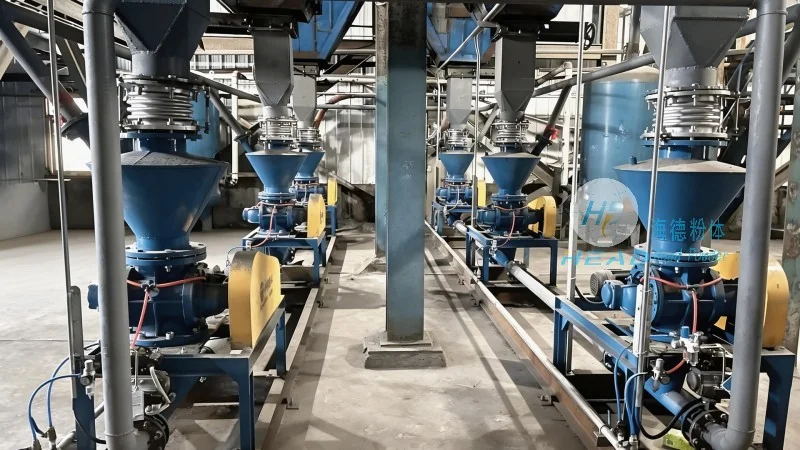
The bulk bag unloading station typically consists of several key components that work together to facilitate the powder transfer process. These components include the bulk bag support frame, the discharge valve, the conveyor system, and the dust collection system. The bulk bag is placed on the support frame, which is designed to hold the bag securely during the unloading process. The discharge valve is located at the bottom of the bag and is used to control the flow of material out of the bag. The conveyor system, often a screw or pneumatic conveyor, transports the material from the bag to the storage silo or processing equipment. The dust collection system is essential for maintaining a clean and safe working environment by capturing and filtering airborne particles.
Operation Process of the Bulk Bag Unloading Station
The operation process of a bulk bag unloading station powder conveying machine begins with the placement of the bulk bag onto the support frame. The bag is then secured in place, and the discharge valve is opened to allow the material to flow out of the bag. The conveyor system is activated, and the material is transported from the bag to the receiving container or silo. The speed of the conveyor can be adjusted to control the flow rate of the material. The dust collection system is also activated during this process to capture any airborne particles and prevent contamination. Once the bulk bag is empty, the discharge valve is closed, and the bag is removed from the support frame. The entire process is typically automated, with the machine controlling the flow rate and ensuring that the material is transferred safely and efficiently.
Working Principle of the Powder Conveying System
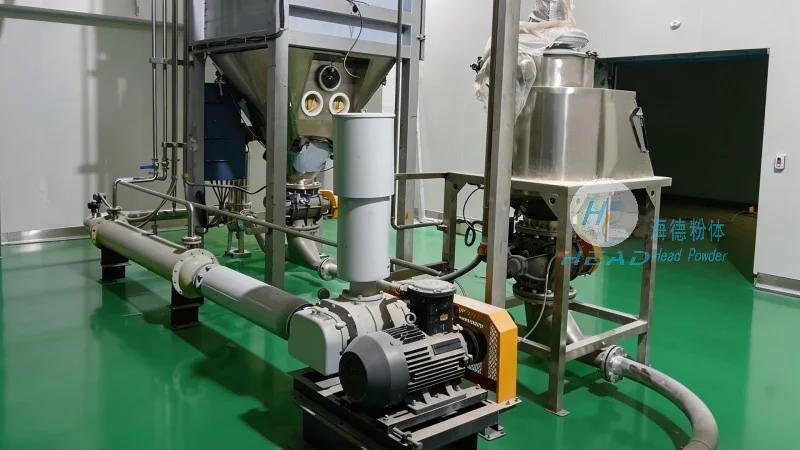
The working principle of the bulk bag unloading station powder conveying machine is based on the principles of mechanical and pneumatic conveying. The screw conveyor, for example, uses a rotating screw to push the material forward, while the pneumatic conveyor uses compressed air to move the material through a pipeline. The choice of conveying system depends on the properties of the material, such as its density, flowability, and moisture content. The discharge valve is controlled by a motor or pneumatic actuator, which opens and closes the valve to regulate the flow of material. The dust collection system uses a filter to capture the airborne particles and a fan to draw air through the filter, ensuring that the air is clean before it is released back into the environment.
Advantages of Using Bulk Bag Unloading Station Powder Conveying Machines
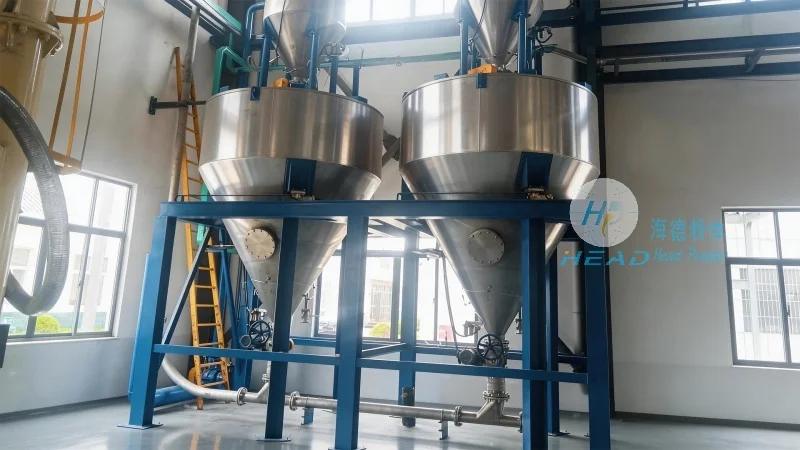
Bulk bag unloading station powder conveying machines offer several advantages over traditional manual unloading methods. These machines are designed to handle large quantities of material efficiently and safely, reducing the risk of accidents and improving productivity. The automated operation of these machines reduces the need for manual labor, which can be costly and time-consuming. The dust collection system also helps to maintain a clean and safe working environment, reducing the risk of respiratory problems and other health issues. Additionally, these machines are designed to be durable and reliable, with low maintenance requirements, which can help to reduce operating costs.
Conclusion
Bulk bag unloading station powder conveying machines are essential equipment for industries that handle bulk materials. These machines are designed to efficiently and safely transfer powders from bulk bags into storage silos or processing equipment. The operation process involves several key steps, including the placement of the bulk bag, the opening of the discharge valve, the activation of the conveyor system, and the operation of the dust collection system. The working principle of these machines is based on mechanical and pneumatic conveying, with the choice of system depending on the properties of the material. The advantages of using these machines include increased efficiency, reduced labor costs, improved safety, and lower maintenance requirements. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. provides high-quality bulk bag unloading station powder conveying machines that meet the needs of various industries.




