HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and supply of advanced powder handling systems. The company's core product, the powder conveying equipment for dust collection stations, plays a crucial role in modern industrial applications by ensuring efficient and reliable material transport. This equipment is essential for maintaining the performance and safety of dust collection systems, which are critical in industries such as cement, chemical, and food processing.
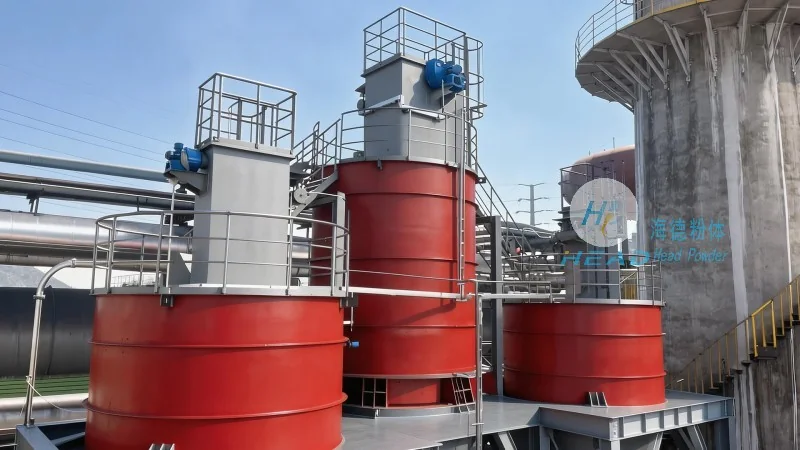
The operation process of the powder handling equipment in dust collection stations typically begins with the collection of airborne particles. As dust is generated during industrial processes, it is captured by the dust collection system and deposited into a hopper or storage bin. The powder handling equipment then takes over, utilizing various technologies like pneumatic conveying, mechanical conveying, or a combination of both to transport the collected powder from the storage area to the desired processing or disposal location. The system ensures that the powder is moved without causing re-entrainment or loss, maintaining the integrity of the material and preventing contamination.
Working principle of the equipment involves several key components that work in tandem to achieve efficient powder transport. The primary components include a hopper or feeder that controls the flow of powder, a conveying line (either pneumatic or mechanical), and a control system that regulates the operation. In pneumatic conveying systems, compressed air is used to create a flow that moves the powder through the pipeline. The air pressure and flow rate are carefully controlled to ensure that the powder is transported at the optimal velocity, minimizing particle degradation and system wear. Mechanical conveying systems, on the other hand, use positive displacement pumps or screw conveyors to move the powder, which is particularly effective for bulk materials and high-temperature applications.
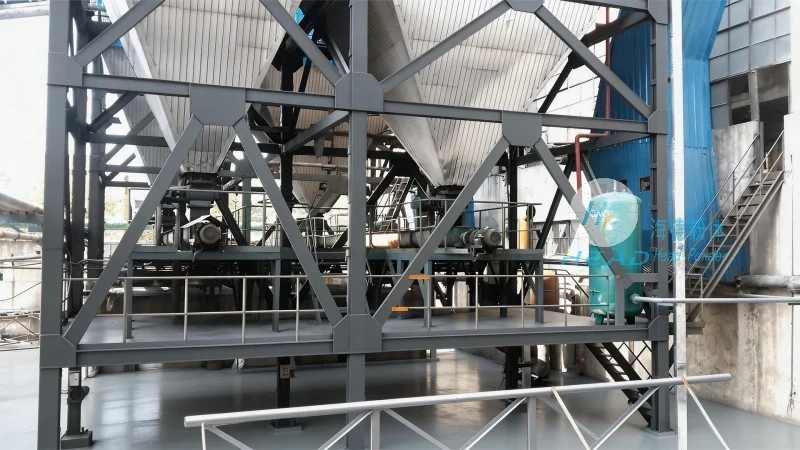
The control system is a critical element in the operation, as it monitors and adjusts the flow rate, pressure, and other parameters to maintain consistent performance. Sensors and feedback mechanisms are integrated into the system to detect any deviations, such as blockages or pressure drops, and automatically adjust the operation to prevent system failures. This ensures that the powder handling equipment operates smoothly and reliably, even under varying load conditions.
HeadPowder's expertise lies in customizing these systems to meet the specific needs of each client. The company considers factors such as the type of powder, particle size, moisture content, and the distance to be covered when designing the system. By optimizing the conveying velocity, line diameter, and air pressure, the equipment can achieve high efficiency and low energy consumption. For example, in cement plants, the powder handling equipment is designed to transport raw materials and finished products efficiently, while in chemical plants, it handles reactive powders with precision and safety.
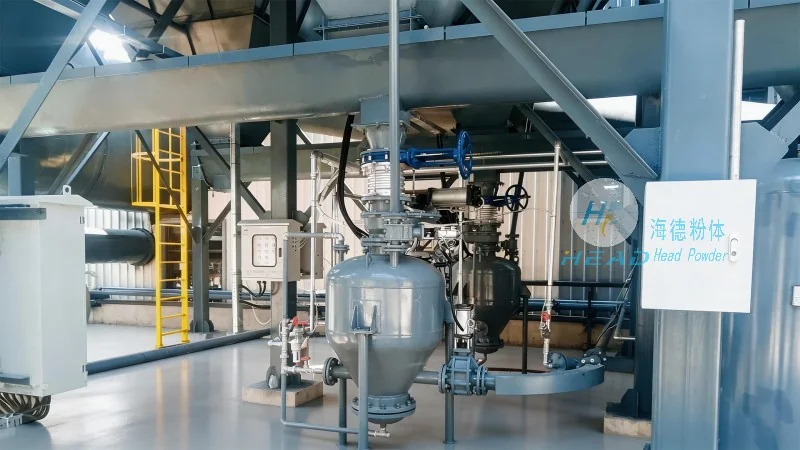
The equipment's design also emphasizes safety and maintenance. The use of robust materials and components ensures that the system can withstand the harsh conditions of industrial environments. Regular maintenance is facilitated by easy access to components, allowing for quick inspections and repairs. This reduces downtime and increases the overall lifespan of the equipment, providing long-term value to the client.
In conclusion, the powder handling equipment in dust collection stations is a sophisticated system that combines advanced technology with careful engineering to ensure efficient material transport. HeadPowder's commitment to quality and innovation has made their systems a trusted choice in various industries. By understanding the operation process and working principle of this equipment, users can appreciate the importance of reliable powder handling in maintaining the performance and safety of dust collection systems.




