The copper mine sand powder conveying system is a specialized industrial equipment designed to efficiently transport and handle copper mine sand and other fine powders. As a critical component in copper mining operations, this system ensures the smooth flow of materials from extraction sites to processing facilities, minimizing downtime and optimizing production efficiency. The system is engineered to handle the unique challenges posed by copper mine sand, such as high moisture content, abrasive properties, and varying particle sizes, making it an essential tool for modern mining operations.
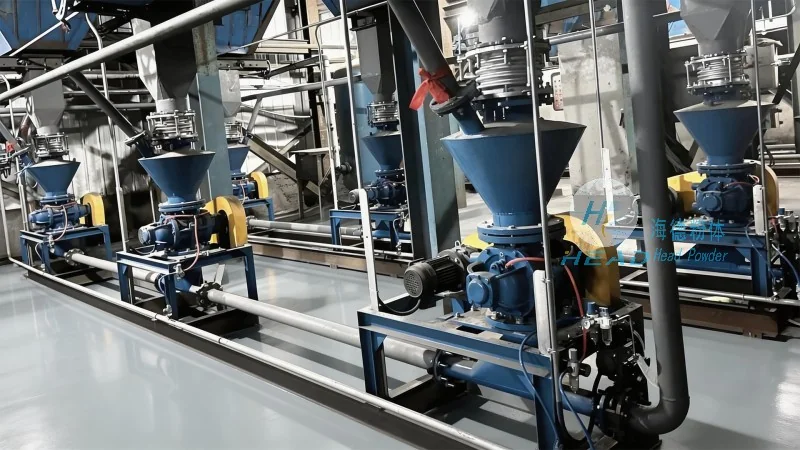
Key Components and Their Functions
The copper mine sand powder conveying system typically consists of several key components, each playing a vital role in the overall operation. The primary components include a hopper for material storage, a conveyor belt or screw conveyor for horizontal transport, a vertical lift mechanism for vertical movement, and a dust collection system to maintain air quality. The hopper is designed to hold a large volume of copper mine sand, allowing for continuous feeding into the system. The conveyor belt or screw conveyor ensures that the material is moved horizontally with minimal friction, while the vertical lift mechanism, often a bucket elevator or pneumatic conveyor, transports the material vertically to higher levels of the processing plant. The dust collection system is integrated to capture and filter airborne particles, ensuring a safe and clean working environment.
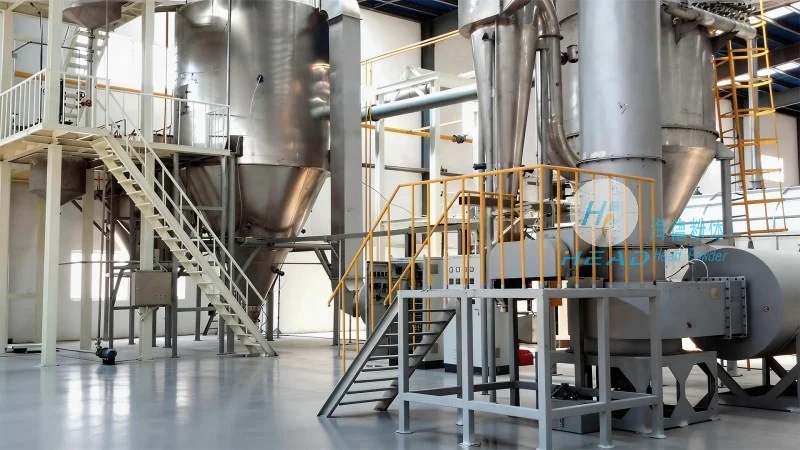
Operation Process: Step-by-Step Overview
The operation of the copper mine sand powder conveying system follows a systematic process, starting with material intake and ending with material delivery to the processing unit. The process begins when copper mine sand is fed into the hopper from the mine or storage area. The material then flows into the conveyor belt or screw conveyor, which transports it horizontally to the vertical lift section. The vertical lift mechanism then elevates the material to the desired height, where it is discharged into the processing equipment. Throughout this process, the system is equipped with sensors and controls to monitor flow rates, pressure, and other critical parameters, ensuring consistent and reliable operation. The dust collection system operates continuously to capture any particles that may be released during the conveying process, preventing air pollution and maintaining compliance with environmental regulations.
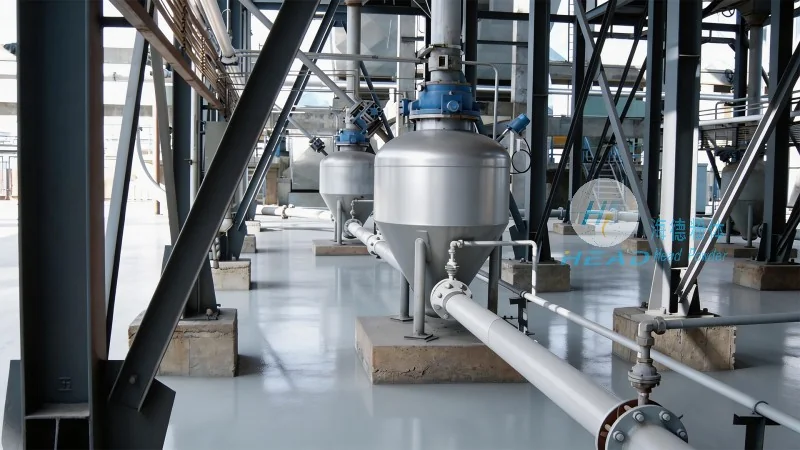
Working Principle: How the System Transfers Copper Mine Sand
The working principle of the copper mine sand powder conveying system is based on mechanical energy and material properties. The system utilizes gravity and mechanical force to move the copper mine sand from the hopper to the processing unit. The horizontal conveyor uses friction between the material and the conveyor surface to move the sand forward, while the vertical lift mechanism uses buckets or air pressure to lift the material upward. The dust collection system employs filtration and ventilation to remove airborne particles, ensuring that the air in the processing area remains clean. The entire system is controlled by a programmable logic controller (PLC), which coordinates the operation of all components and adjusts parameters based on real-time feedback from sensors. This integrated control system ensures that the conveying process is efficient, safe, and environmentally responsible.
Advantages of the Copper Mine Sand Powder Conveying System
Implementing a copper mine sand powder conveying system offers several advantages for mining operations. First, it significantly reduces labor costs by automating the material handling process, eliminating the need for manual loading and unloading. Second, the system minimizes material loss and contamination, as the enclosed design prevents dust and debris from escaping. Third, the system improves production efficiency by ensuring a continuous and consistent flow of copper mine sand to the processing unit, reducing downtime caused by material shortages or blockages. Additionally, the system enhances safety by reducing the risk of accidents associated with manual handling of heavy or abrasive materials. The use of advanced materials and engineering in the construction of the system ensures durability and long-term reliability, making it a cost-effective investment for mining companies.
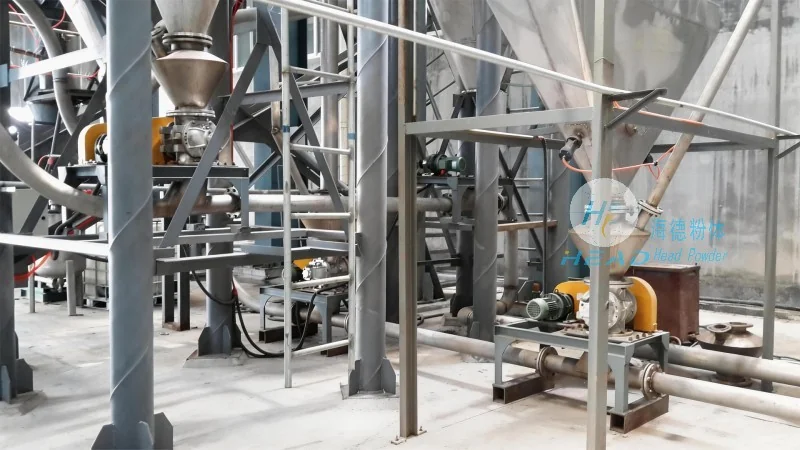
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of industrial conveying systems, including copper mine sand powder conveying equipment. With a strong focus on innovation and quality, headpowder has established itself as a trusted partner for mining and processing industries worldwide. The company's expertise in material handling technology, combined with its commitment to customer satisfaction, has enabled it to deliver high-performance conveying systems that meet the unique needs of each client. Headpowder's facilities are located in Shandong, China, where the company leverages advanced manufacturing techniques and a skilled workforce to produce reliable and efficient equipment. The company's products are designed to be adaptable to various mining conditions and processing requirements, ensuring that clients receive solutions tailored to their specific operational needs.




