Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for various industrial applications. Our company is dedicated to providing efficient and reliable solutions for material handling, particularly in the processing of agricultural byproducts like rice husk. The rice husk powder pneumatic conveying system is a key product that exemplifies our commitment to innovation and quality in material transport technology.
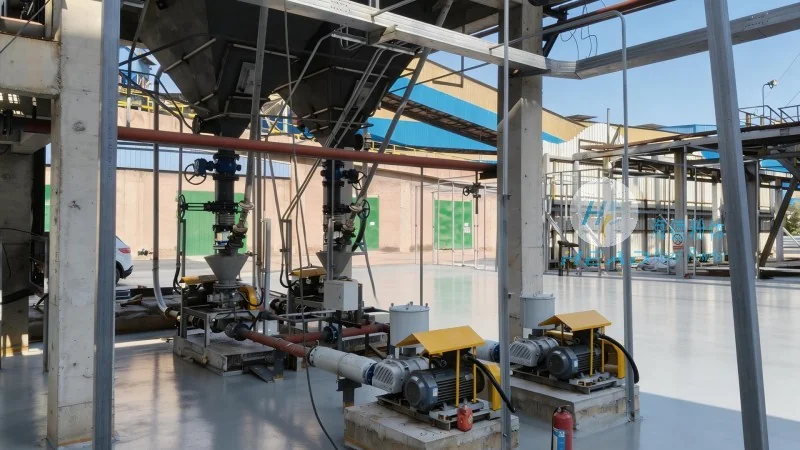
Introduction to the Rice Husk Powder Pneumatic Conveying System
The rice husk powder pneumatic conveying system is engineered to handle the transportation of rice husk powder from storage silos or processing units to downstream equipment such as boilers, pelletizers, or storage facilities. This system utilizes compressed air or vacuum to move the fine powder through a network of pipes, ensuring a clean, dust-free, and efficient transfer process. The system is designed to meet the specific demands of rice husk processing industries, offering high capacity, low maintenance, and environmental friendliness.
Working Principle of the Pneumatic Conveying System
The core principle of the rice husk powder pneumatic conveying system is based on the physics of fluid dynamics and particle movement. In a typical positive pressure system, compressed air is introduced into the material feed point, creating a pressure differential that propels the rice husk powder through the pipeline. The air and powder mixture travels at high velocity, maintaining the powder in a suspended state to prevent clogging and ensure smooth flow. The system may also incorporate a negative pressure (vacuum) design, where a vacuum pump creates a suction force to draw the powder from the source to the destination. Both systems rely on carefully designed components, including feeders, pipelines, separation units, and control valves, to achieve optimal performance.
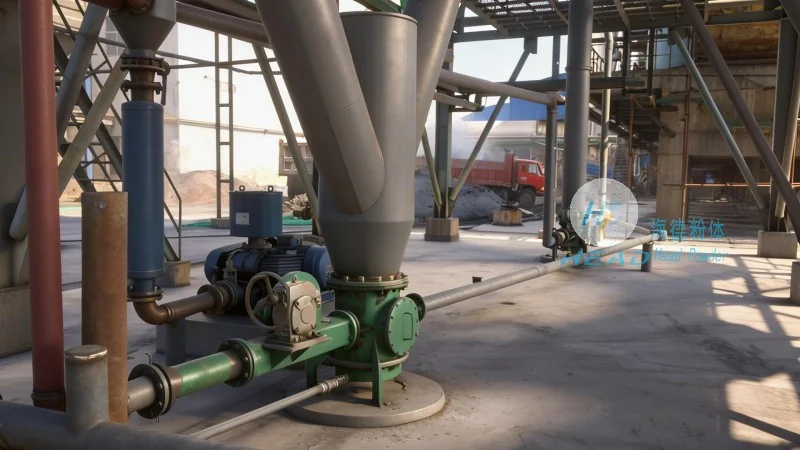
Step-by-Step Operation Process
The operation of the rice husk powder pneumatic conveying system follows a systematic sequence to ensure consistent and reliable material transport. The process begins with the loading of rice husk powder into the storage silo or hopper. An automatic feeder then measures and discharges the powder into the conveying line. Compressed air is supplied to the system, either through a blower or a compressed air line, to generate the necessary pressure or vacuum. The powder is then conveyed through the pipeline network to the target location. At the receiving end, a separator or cyclone separates the powder from the air, allowing the powder to be deposited into a collection bin or directly into the next processing unit. The system is equipped with control panels that monitor pressure, flow rate, and other parameters, enabling real-time adjustments to maintain optimal operation.
Key Components and Their Functions
The rice husk powder pneumatic conveying system consists of several critical components that work in tandem to ensure efficient operation. The primary components include: 1. **Feeder**: A device that accurately measures and discharges the rice husk powder into the conveying line, maintaining a consistent flow rate. 2. **Compressor or Vacuum Pump**: Provides the necessary air pressure or vacuum to move the powder through the system. 3. **Conveying Pipeline**: A network of pipes, typically made of stainless steel or other corrosion-resistant materials, to transport the powder. 4. **Separator/Cyclone**: A device that separates the powder from the air at the receiving end, preventing dust accumulation and ensuring clean air discharge. 5. **Control System**: An automated system that monitors and controls the pressure, flow, and other operational parameters to optimize performance and prevent system failures.
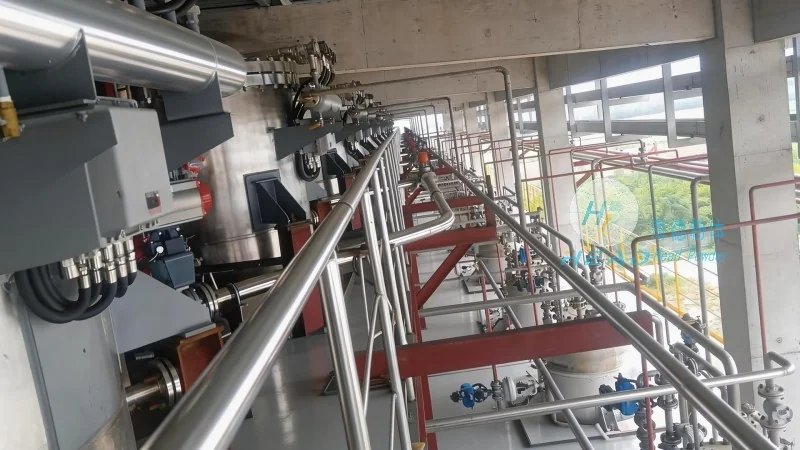
Advantages of the Rice Husk Powder Pneumatic Conveying System
Implementing a rice husk powder pneumatic conveying system offers numerous advantages for industrial applications. Firstly, it provides a dust-free and clean transfer process, which is essential for maintaining a safe and healthy working environment in rice husk processing facilities. Secondly, the system offers high capacity and continuous operation, allowing for efficient handling of large volumes of powder. Thirdly, it minimizes material loss and contamination, as the powder is enclosed within the pipeline system. Additionally, the system reduces labor costs by automating the material transport process and eliminates the need for manual handling. Finally, the system is designed for low maintenance, with easy access to components for inspection and replacement, ensuring long-term reliability and cost-effectiveness.
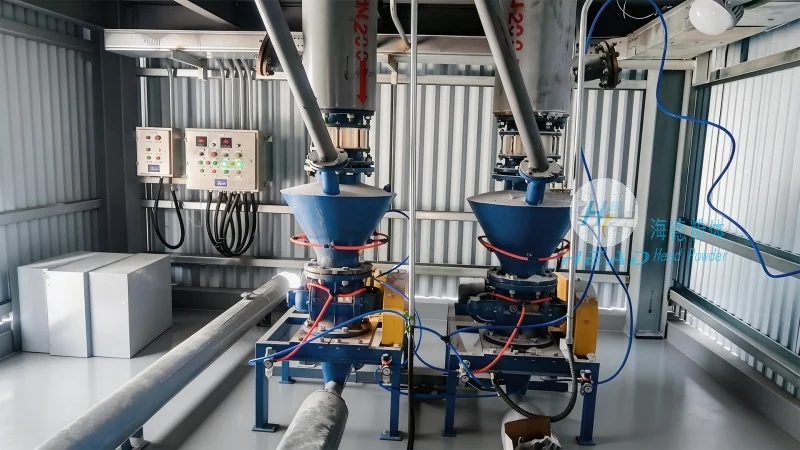
Applications and Industries
The rice husk powder pneumatic conveying system is widely used in various industries that process agricultural byproducts and require efficient material handling. The primary applications include: 1. **Energy Production**: Transporting rice husk powder to boilers for combustion in power plants or heating systems. 2. **Pelletization**: Conveying rice husk powder to pelletizing machines to produce biomass pellets for fuel or animal feed. 3. **Storage and Distribution**: Moving rice husk powder from processing units to storage silos or distribution centers. 4. **Industrial Processing**: Handling rice husk powder in other industrial processes that require fine powder transport, such as chemical or pharmaceutical applications.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive range of rice husk powder pneumatic conveying systems that are designed to meet the specific needs of rice husk processing industries. By leveraging advanced technology and engineering expertise, our systems provide efficient, reliable, and environmentally friendly material handling solutions. The operation process and working principle of these systems ensure optimal performance, minimal maintenance, and high productivity, making them an ideal choice for industrial applications. With our headquarters in Shandong, China, we are committed to delivering high-quality products and services that enhance the efficiency and sustainability of our clients' operations.




