

HeadPowder Pneumatic Phosphate Powder Conveying System: The Efficiency Engine for Phosphate Powder T
The HeadPowder Pneumatic Phosphate Powder Conveying System represents a cutting-edge solution designed to optimize the transportation of phosphate powder in industrial settings. As a key component in mineral processing and material handling, this system addresses the challenges associated with handling fine, dusty materials like phosphate powder, ensuring efficient, reliable, and safe operation. By leveraging pneumatic conveying technology, the system offers a robust alternative to traditional methods, such as belt conveyors or bucket elevators, which often struggle with material segregation, dust generation, and operational inefficiencies.
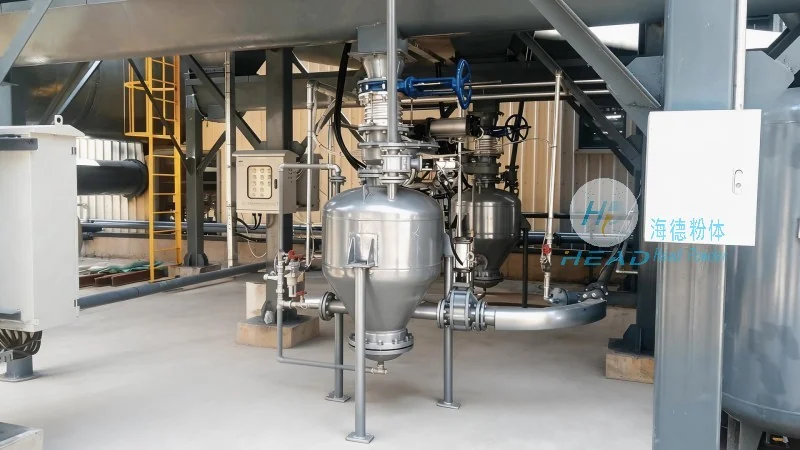
Key Features and Technical Advantages
At the core of the HeadPowder system is its advanced pneumatic conveying technology, which utilizes air pressure to transport phosphate powder through a network of pipes. This method eliminates the need for mechanical components that can cause wear and tear, reducing maintenance costs and extending the system's lifespan. The system is engineered with precision to handle varying particle sizes and moisture content, ensuring consistent performance even with fluctuating material characteristics. Additionally, the design incorporates features like air filtration and dust collection, minimizing environmental impact and maintaining compliance with industrial safety standards. The HeadPowder system is also scalable, allowing it to be customized to meet the specific needs of different production scales, from small-scale operations to large industrial facilities.
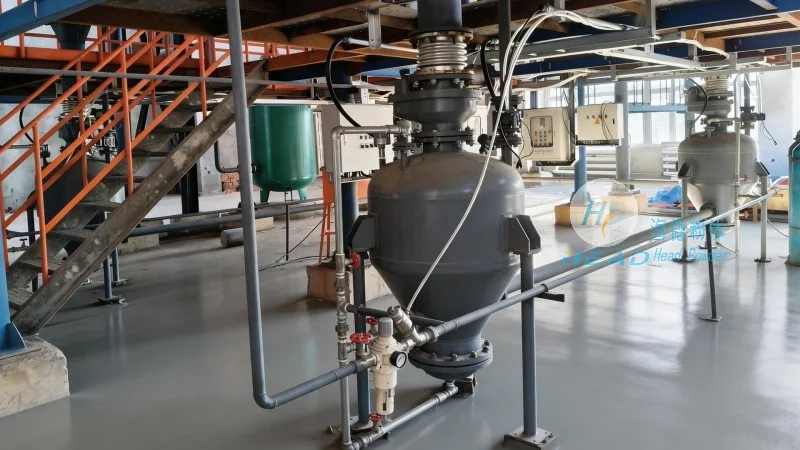
Efficiency and Performance in Phosphate Powder Handling
One of the primary benefits of the HeadPowder Pneumatic Phosphate Powder Conveying System is its ability to enhance operational efficiency. By streamlining the transport process, the system reduces downtime and increases overall productivity. The pneumatic conveying method allows for continuous, unidirectional flow of material, eliminating the need for manual intervention or frequent system stops. This results in a more stable and predictable production cycle, which is crucial for maintaining consistent output quality. Furthermore, the system's ability to handle high volumes of phosphate powder without compromising on speed or accuracy makes it an ideal choice for industries that require rapid material transfer, such as fertilizer manufacturing and chemical processing.
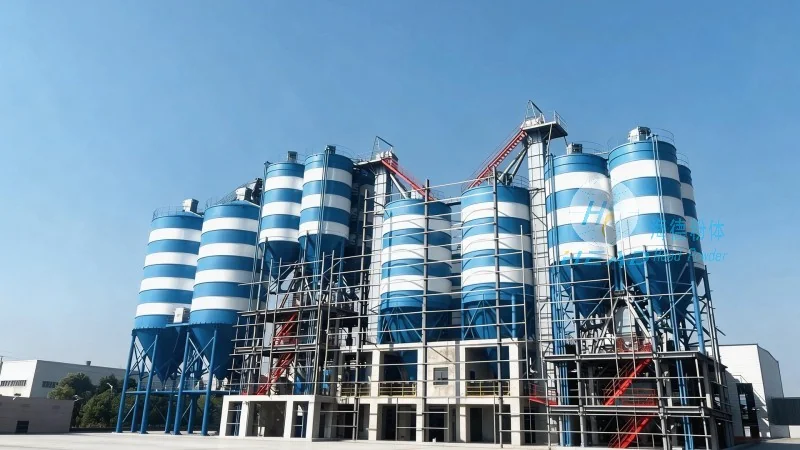
Reliability and Safety in Industrial Applications
Reliability and safety are paramount in industrial material handling, and the HeadPowder system excels in both areas. The pneumatic design minimizes the risk of material spillage or leakage, which is a common issue with traditional conveyor systems. The system is equipped with advanced sensors and control mechanisms that monitor pressure, flow, and material levels in real-time, providing immediate alerts in case of anomalies. This proactive approach to monitoring ensures that any potential issues are addressed promptly, preventing costly production interruptions. Additionally, the system's low maintenance requirements and durable construction contribute to long-term operational reliability, making it a cost-effective solution for businesses looking to invest in sustainable and efficient material handling infrastructure.
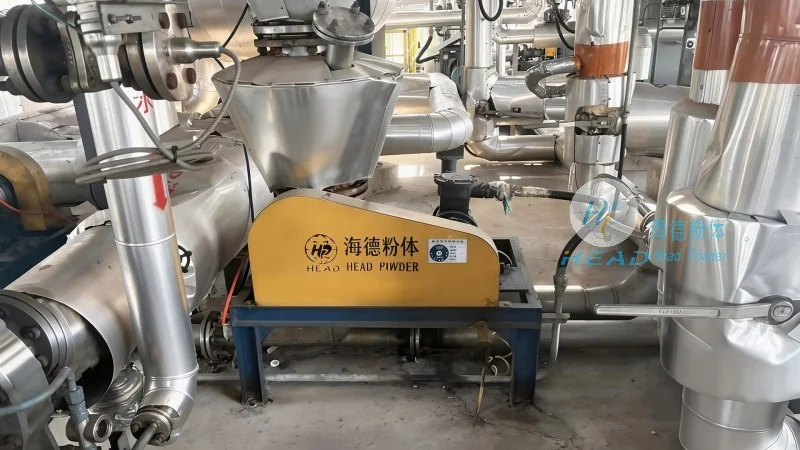
Customization and Scalability for Diverse Industrial Needs
Shandong HeadPowder Engineering Co., Ltd., the manufacturer of the system, understands that industrial applications vary widely in terms of scale, material properties, and operational requirements. To address these diverse needs, the company offers customized solutions tailored to each client's specific situation. The HeadPowder system can be configured with different components, such as rotary valves, airlocks, and dust collectors, to optimize performance for specific applications. Whether it's a small-scale phosphate processing plant or a large-scale fertilizer production facility, the system can be scaled to meet the demands of the operation. The company's expertise in engineering and material handling allows them to provide comprehensive support, from system design and installation to ongoing maintenance and technical assistance. This commitment to customization and scalability ensures that clients receive a solution that is not only efficient but also adaptable to future growth and evolving industry demands.