

Application of Pneumatic Conveying Technology in Bicarbonate of Soda Transportation Design Optimizat
HeadPowder, a leading engineering firm based in Shandong, China, specializes in optimizing material handling solutions, particularly in the application of pneumatic conveying technology for the transportation of sodium bicarbonate. This article explores how advanced pneumatic conveying systems enhance the efficiency, safety, and reliability of bicarbonate of soda (baking soda) transportation processes.
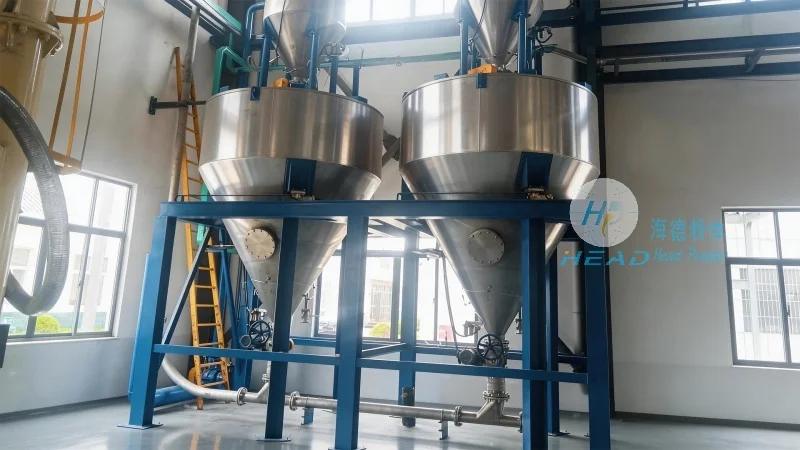
Understanding Pneumatic Conveying Technology
Pneumatic conveying, or air-powered transport, is a method of moving bulk materials through a pipeline using compressed air or other gases. Unlike traditional mechanical systems like screw conveyors or belt conveyors, pneumatic systems offer several advantages for handling delicate or abrasive materials such as sodium bicarbonate. The technology involves transporting material in a sealed system, which minimizes dust exposure, reduces product contamination, and provides better control over flow rates and pressure. This makes it ideal for applications where product integrity and environmental safety are critical.
Key Advantages of Pneumatic Conveying for Bicarbonate of Soda
When applied to bicarbonate of soda transportation, pneumatic conveying systems offer distinct benefits that traditional methods may not provide. First, the sealed pipeline design prevents dust from escaping into the environment, ensuring compliance with environmental regulations and protecting workers from respiratory hazards. Second, the gentle handling of the material reduces product degradation, such as clumping or particle breakage, which is crucial for maintaining the quality of sodium bicarbonate used in various industries, including food, pharmaceuticals, and chemical manufacturing. Third, the system allows for precise control over the flow rate and pressure, enabling seamless integration with downstream processes like packaging or mixing. This level of control minimizes waste and optimizes production throughput.
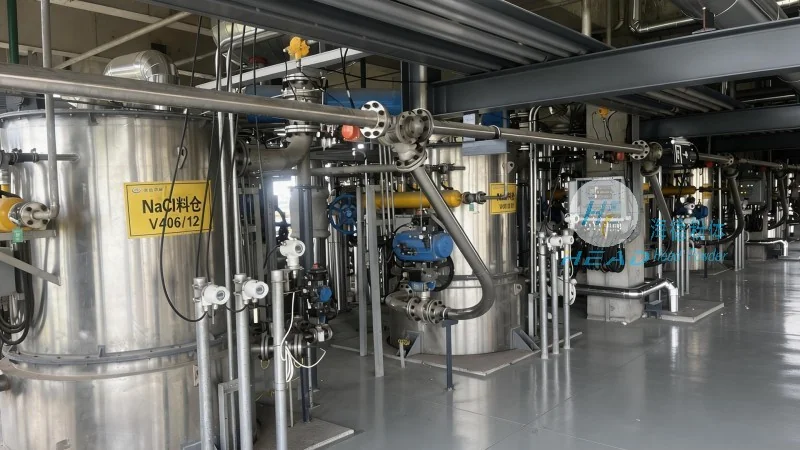
Design Optimization Strategies for Bicarbonate of Soda Transportation
Optimizing the design of pneumatic conveying systems for bicarbonate of soda involves several key considerations. The selection of appropriate pipeline materials is critical, as sodium bicarbonate can be corrosive to certain metals. Stainless steel or specialized coatings are often used to prevent material degradation and ensure long-term system durability. Additionally, the system layout must be carefully planned to minimize pressure drops and energy consumption. This includes selecting the right type of conveying air (e.g., positive or negative pressure systems) and ensuring proper pipeline sizing to maintain efficient material transport. HeadPowder engineers employ advanced computational fluid dynamics (CFD) and material flow analysis to model and optimize these systems, ensuring that the final design meets both performance and cost objectives.
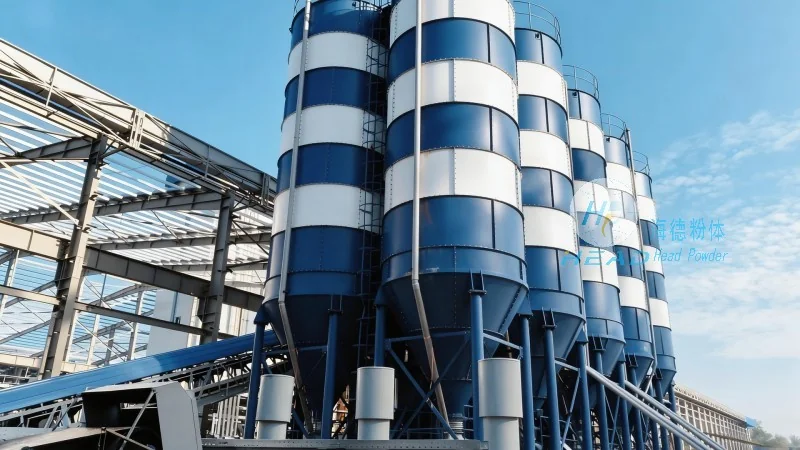
Enhancing Safety and Operational Efficiency
Another critical aspect of optimizing bicarbonate of soda transportation is enhancing safety and operational efficiency. Pneumatic conveying systems can be equipped with safety features such as pressure relief valves, dust collection systems, and automated shutdown mechanisms to prevent accidents and ensure compliance with occupational health and safety standards. Moreover, the integration of sensors and control systems allows for real-time monitoring of system performance, enabling proactive maintenance and reducing downtime. By leveraging these technologies, companies can achieve higher productivity while maintaining a safe working environment.
Conclusion
HeadPowder's expertise in pneumatic conveying technology provides a comprehensive solution for optimizing bicarbonate of soda transportation. By combining advanced engineering, material handling knowledge, and a commitment to safety and efficiency, the company helps clients improve their operational performance and reduce costs. With a focus on tailored solutions that meet specific industry requirements, HeadPowder continues to be a trusted partner in the design and implementation of effective material handling systems for sodium bicarbonate and other bulk materials.