

[Efficient and Clean: The Air-Flow Conveying Technology for Powdered Milk Transport]
For the dairy industry, ensuring the efficient and hygienic transport of powdered milk is paramount. Traditional methods often struggle with maintaining cleanliness and preventing contamination, which can compromise product quality and safety. This is where air-flow conveying technology emerges as a superior solution, offering a clean, efficient, and reliable method for handling powdered milk. In this article, we delve into the benefits and applications of air-flow conveying systems, highlighting how they enhance the overall efficiency of powdered milk transport processes.
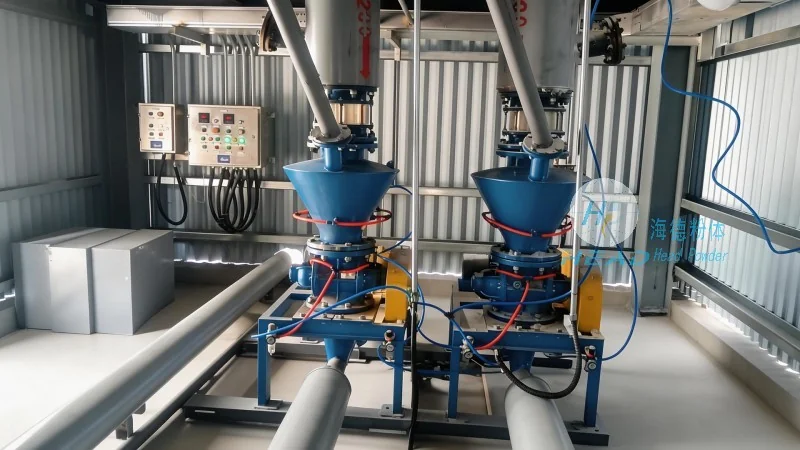
Understanding Air-Flow Conveying Technology
Air-flow conveying, also known as pneumatic conveying, utilizes compressed air to transport bulk materials like powdered milk through a system of pipes. Unlike mechanical systems that rely on moving parts and direct contact, air-flow conveying operates through a closed pipeline network, minimizing the risk of contamination and ensuring a hygienic environment. This technology is particularly well-suited for sensitive products such as powdered milk, which require strict adherence to sanitary standards.
The Advantages of Air-Flow Conveying for Powdered Milk
One of the primary benefits of air-flow conveying is its ability to maintain a high level of cleanliness. By eliminating direct contact between the product and equipment, the risk of cross-contamination is significantly reduced. This is crucial in the dairy industry, where product purity and safety are non-negotiable. Additionally, air-flow conveying systems are highly efficient, capable of transporting large volumes of powdered milk over long distances with minimal energy consumption. The technology also offers flexibility in system design, allowing for integration with existing production lines and easy expansion as production needs grow.
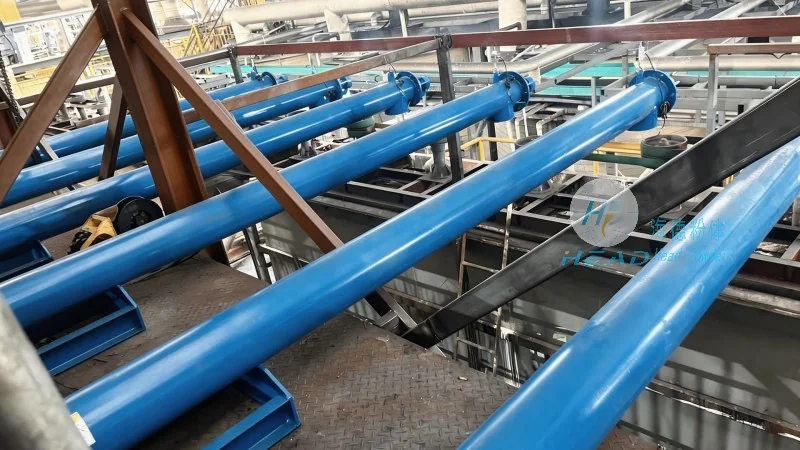
How Air-Flow Conveying Enhances Efficiency
Efficiency in powdered milk transport is critical for optimizing production workflows and reducing operational costs. Air-flow conveying systems achieve this through several key mechanisms. First, the continuous flow of air ensures consistent and uniform movement of the powder, preventing clogging and ensuring a steady supply to downstream processes. Second, the closed system design minimizes material loss and waste, improving overall material handling efficiency. Furthermore, the technology allows for real-time monitoring and control, enabling operators to adjust conveying parameters dynamically to meet varying production demands. These factors collectively contribute to a more streamlined and efficient production process.
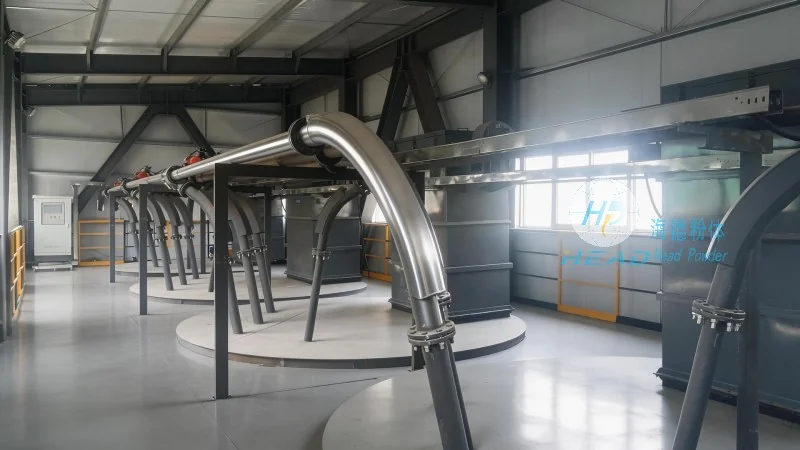
Shandong HeadPowder Engineering Co., Ltd.: Your Partner in Clean and Efficient Powdered Milk Transport
At Shandong HeadPowder Engineering Co., Ltd., we specialize in providing advanced air-flow conveying solutions tailored to the unique needs of the dairy industry. As a leading manufacturer based in China, we combine cutting-edge technology with decades of industry experience to deliver systems that meet the highest standards of hygiene and performance. Our team of experts works closely with clients to design and implement customized air-flow conveying systems that enhance efficiency while ensuring the safety and quality of powdered milk products. With our headquarters in Shandong, China, we are well-positioned to serve clients globally, offering comprehensive support from system design to installation and maintenance.
Conclusion: The Future of Powdered Milk Transport
As the dairy industry continues to evolve, the demand for efficient and hygienic transport solutions remains high. Air-flow conveying technology has proven to be a game-changer in this regard, offering a clean, reliable, and efficient method for handling powdered milk. By choosing a trusted partner like Shandong HeadPowder Engineering Co., Ltd., businesses can ensure that their powdered milk transport processes are optimized for both performance and safety. With our expertise and commitment to quality, we are dedicated to helping the dairy industry achieve its goals of efficiency, hygiene, and product excellence.