

What is Coal Ash Pneumatic Conveying, Classification and Applications of Pneumatic Conveying
Coal ash, a byproduct of coal combustion in power plants and industrial facilities, poses significant handling challenges due to its fine particle size and abrasive nature. Pneumatic conveying offers an efficient solution for transporting coal ash from storage or processing areas to disposal sites or further treatment facilities. This method leverages air pressure to move materials through pipelines, providing a dust-free and continuous operation compared to traditional mechanical methods.
What is Pneumatic Conveying?
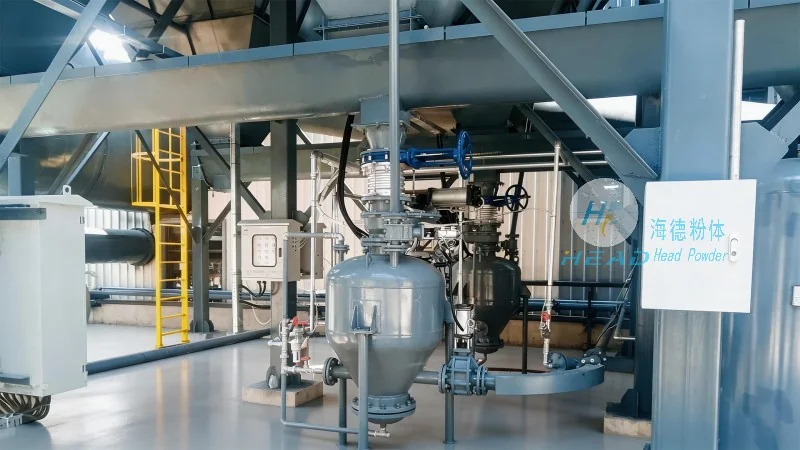
Pneumatic conveying is a technology that uses compressed air or vacuum to transport bulk materials, such as powders and granules, through a closed system of pipes. It is widely used in various industries, including power generation, cement production, and chemical processing, for its ability to handle materials with high moisture content or corrosive properties. The system typically consists of a material feed hopper, a conveyor line, and a discharge point, with air being introduced to create a flow that carries the material along the pipeline.
Coal Ash Pneumatic Conveying: Key Considerations
When applying pneumatic conveying to coal ash, several factors must be considered to ensure optimal performance and system longevity. These include the ash's particle size distribution, moisture content, and abrasiveness, as well as the required conveying distance and flow rate. The choice of conveying system—whether pressure or vacuum—depends on these characteristics and the specific application requirements. For example, pressure systems are suitable for short to medium distances and high flow rates, while vacuum systems are better for longer distances or when the material is located at a higher elevation than the discharge point.
Classification of Pneumatic Conveying Systems
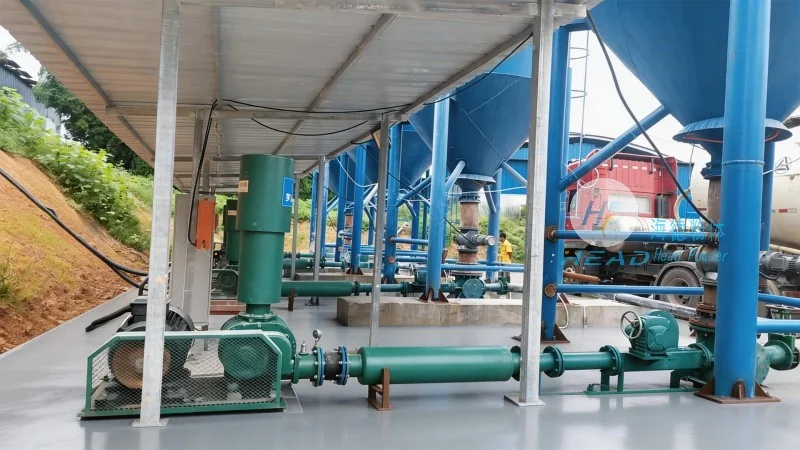
Pneumatic conveying systems are broadly classified into two main types: pressure and vacuum. Pressure systems operate by forcing air into the pipeline, creating a positive pressure that pushes the material forward. These systems are commonly used for short to medium conveying distances and can handle high material loads. Vacuum systems, on the other hand, use a vacuum pump to create a negative pressure that pulls the material into the pipeline. They are ideal for longer distances or when the material is located at a higher elevation than the discharge point.
Applications of Pneumatic Conveying in Coal Ash Handling
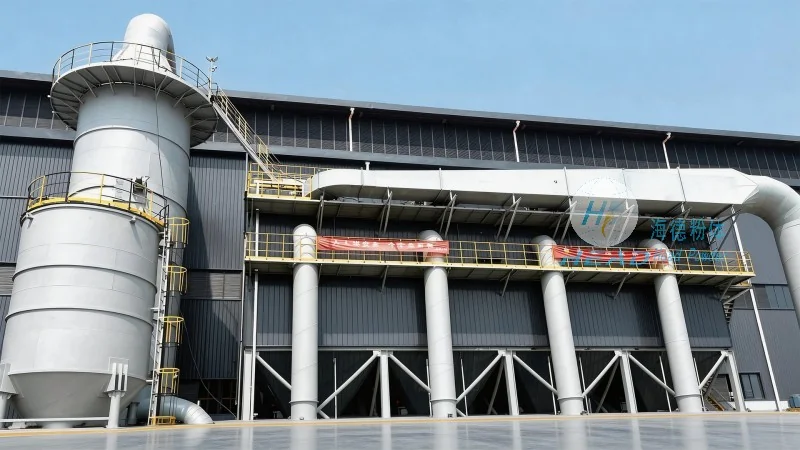
Coal ash pneumatic conveying is employed in several critical applications within power plants and related industries. One primary use is transporting bottom ash and fly ash from boiler ash hoppers to storage silos or disposal sites. This process ensures that ash is removed efficiently without exposing workers to dust or requiring extensive manual handling. Additionally, the system can be integrated with ash treatment processes, such as dewatering or recycling, where the ash is conveyed to processing units for further use or disposal. The ability to handle large volumes of ash at a consistent rate makes pneumatic conveying a preferred choice for maintaining operational efficiency in coal-fired power plants.
Advantages of Pneumatic Conveying for Coal Ash
Compared to traditional mechanical conveying methods, such as belt conveyors or bucket elevators, pneumatic conveying offers several advantages for coal ash handling. First, it provides a dust-free operation, which improves workplace safety and reduces the risk of respiratory issues for personnel. Second, the system is compact and can be installed in confined spaces, making it suitable for retrofitting into existing power plant infrastructure. Third, pneumatic conveying allows for continuous and automated material transport, reducing labor costs and minimizing downtime. Finally, the technology can handle abrasive materials like coal ash without significant wear on the equipment, extending the system's lifespan and reducing maintenance costs.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the unique needs of coal ash handling. With years of experience in the industry, the company has developed expertise in optimizing conveying systems for efficiency, reliability, and safety. By leveraging advanced engineering and material selection, HeadPowder ensures that its systems meet the demanding requirements of modern power plants and industrial facilities. The company's commitment to quality and customer satisfaction has made it a trusted partner for coal ash management solutions worldwide.