What is a Dust-Free Closed Material Handling System? And What Are Its Design Principles?
Release time:2026-09-15 00:03:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Understanding dust-free closed material handling systems is crucial for industries that operate in cleanroom environments or require strict contamination control. These systems are engineered to transport materials without exposing them to external contaminants or releasing particles into the surrounding air. The design principles behind such systems focus on maintaining a sealed environment, minimizing particle generation, and ensuring efficient material flow while adhering to stringent cleanliness standards.
Key Components and Design Principles
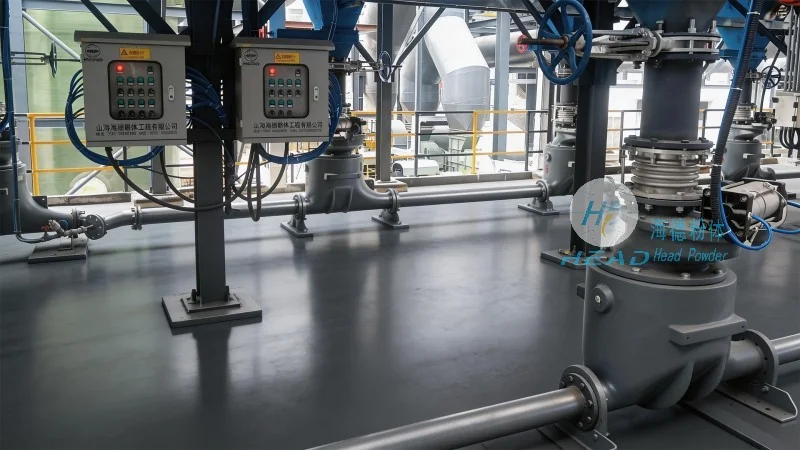
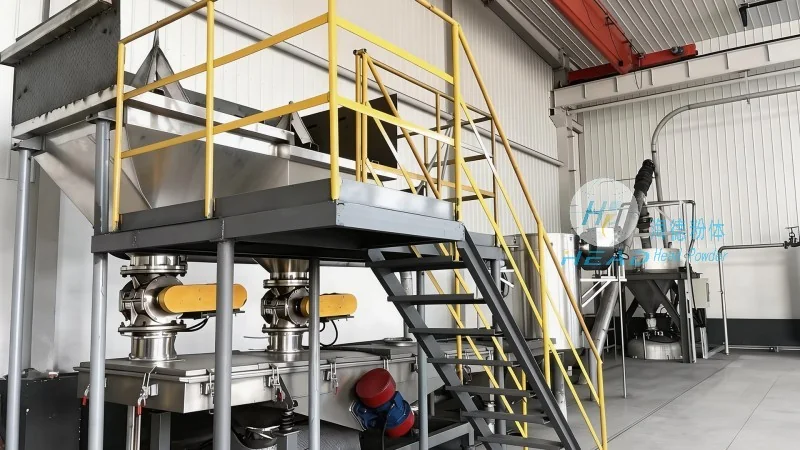
The core components of a dust-free closed material handling system typically include enclosed conveyor belts, sealed hoppers, and integrated filtration units. The design principle of containment is paramount, as it prevents dust and particulate matter from escaping into the workspace. Additionally, these systems often incorporate positive pressure or negative pressure control to maintain air quality within the system. The materials used for construction, such as stainless steel or specialized plastics, are chosen for their resistance to corrosion and ease of cleaning. Sealing mechanisms, like O-rings and gaskets, are critical to prevent leaks and maintain the integrity of the closed system. The design also considers the type of material being handled—whether it's powders, granules, or bulk materials—and tailors the system accordingly to ensure smooth and efficient transport without generating dust.
The Role of Material Handling in Cleanroom Environments
In industries like pharmaceuticals, electronics manufacturing, and food processing, maintaining a clean environment is non-negotiable. Dust-free closed material handling systems play a vital role in ensuring that the production process remains contamination-free. By keeping materials enclosed and the transport process sealed, these systems prevent cross-contamination and protect sensitive products from airborne particles. The design principles also address the need for scalability and adaptability, allowing the system to handle varying volumes of material while maintaining consistent cleanliness. Furthermore, the integration of sensors and monitoring systems helps in real-time tracking of material flow and contamination levels, enhancing overall process control.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in designing and manufacturing dust-free closed material handling systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries requiring high standards of cleanliness and efficiency. HeadPowder's systems are engineered to meet the specific needs of clients, offering customizable solutions that align with their operational requirements. The company's headquarters is located in Shandong, China, where it leverages advanced technology and skilled expertise to develop cutting-edge material handling equipment. By adhering to international standards and leveraging years of industry experience, HeadPowder ensures that its products deliver reliable performance and long-term value to its customers.




