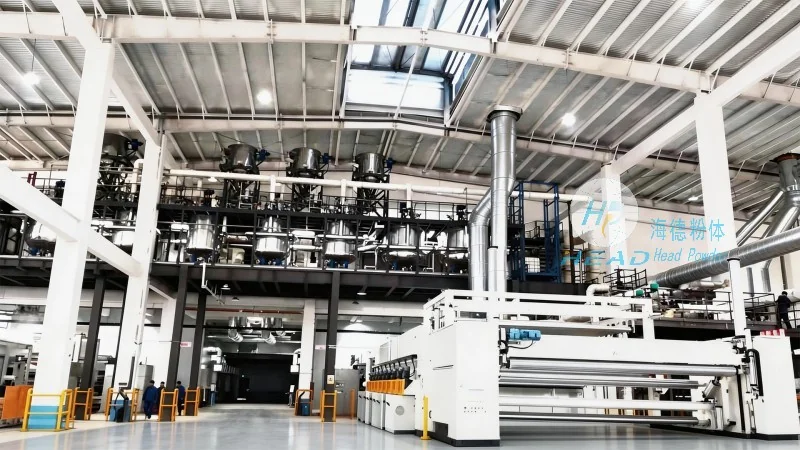
Red sugar powder conveying systems are essential for the efficient handling and transportation of red sugar in industrial settings. These systems are designed to ensure smooth and reliable movement of the powder from storage to processing or packaging areas. Understanding the equipment and its underlying design principles is crucial for optimizing production processes and maintaining product quality.
Introduction to Red Sugar Powder Conveying Systems
Red sugar, also known as brown sugar, is a popular sweetener with a rich, molasses flavor. Its granular or powdered form requires specialized equipment for safe and efficient handling. The red sugar powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is engineered to address the unique challenges of transporting this type of material. This system integrates various components to achieve seamless material flow, ensuring minimal product degradation and operational efficiency.
Key Components of the Conveying System
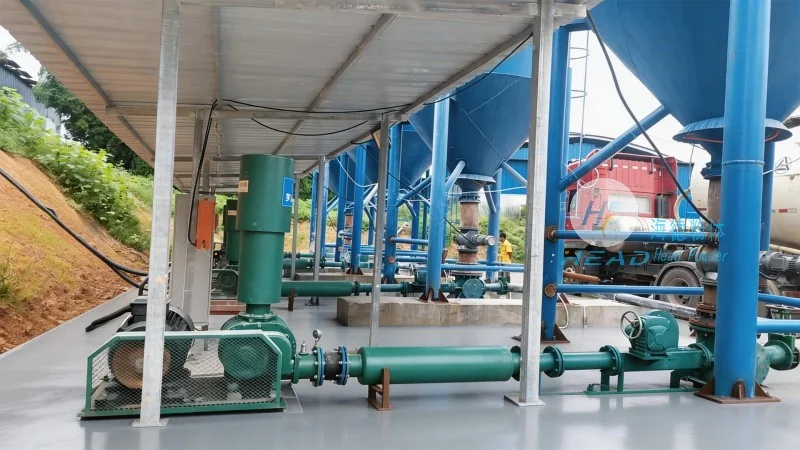
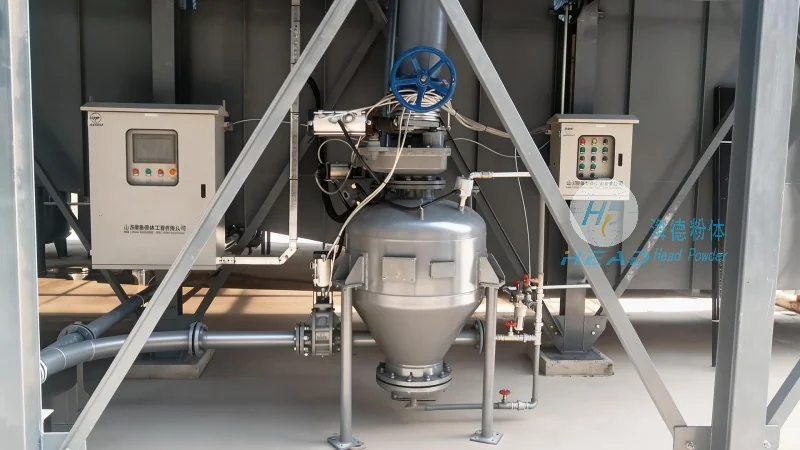
The core components of the red sugar powder conveying system include feeders, conveyors, and control systems. The feeder is responsible for uniformly feeding the red sugar powder into the conveyor, preventing blockages and ensuring consistent flow rates. The conveyor itself, often a pneumatic or mechanical type, transports the powder through the system. Control systems monitor and regulate the operation, adjusting speed and pressure as needed to maintain optimal performance. Each component is carefully designed to handle the specific properties of red sugar, such as its moisture content and particle size.
Design Principles for Optimal Performance
The design of the red sugar powder conveying system is guided by several key principles to ensure reliability and efficiency. First, the system must minimize product contamination and degradation. This is achieved through materials that are non-reactive with the sugar and sealed systems to prevent moisture absorption. Second, energy efficiency is a critical consideration. The design incorporates low-friction components and optimized airflow to reduce energy consumption while maintaining high throughput. Third, scalability and adaptability are essential for industrial applications. The system is built to accommodate varying production volumes and can be easily integrated with existing processing lines. These principles collectively ensure that the conveying system operates smoothly and meets the demands of modern red sugar production.
Application in Red Sugar Processing
In the red sugar processing industry, the conveying system plays a vital role in streamlining operations. From raw material storage to final packaging, the system ensures that red sugar powder is moved safely and efficiently. The equipment is particularly useful in large-scale production facilities where manual handling is impractical and can lead to product loss or contamination. By automating the conveying process, manufacturers can improve productivity, reduce labor costs, and enhance product consistency. The system's design also allows for easy integration with other processing equipment, such as mixers and packaging machines, creating a seamless production line.
Advantages of the HeadPowder Conveying System
Shandong HeadPowder Engineering Co., Ltd. has developed a comprehensive solution for red sugar powder conveying that offers several advantages over traditional methods. The system's modular design allows for easy installation and maintenance, reducing downtime and operational costs. The use of advanced materials and engineering ensures long-term durability and reliability. Additionally, the system is designed to meet international safety and quality standards, providing peace of mind to manufacturers. The company's expertise in powder handling technology has led to a product that is both effective and user-friendly, making it a preferred choice for red sugar producers worldwide.
Conclusion and Future Outlook
Red sugar powder conveying systems are indispensable in the modern red sugar industry, and the design principles behind them are critical to their success. The equipment from Shandong HeadPowder Engineering Co., Ltd. exemplifies the integration of advanced technology and practical design, offering manufacturers a reliable solution for their material handling needs. As the industry continues to evolve, the importance of efficient and safe conveying systems will only grow, making such equipment essential for maintaining competitiveness and product quality. By understanding the components and principles of these systems, manufacturers can make informed decisions to optimize their operations and ensure long-term success in the red sugar market.




