

Working Principle and Features of Dust Gas-Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced dust gas-pneumatic conveying equipment. This article delves into the working principle and key features of such systems, highlighting their efficiency and versatility in material handling applications.
Introduction to Dust Gas-Pneumatic Conveying Systems
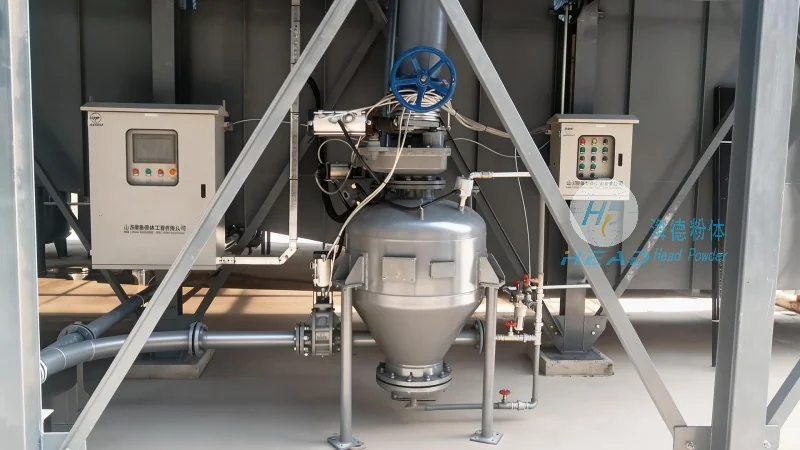
Dust gas-pneumatic conveying systems are essential in industries dealing with fine powders and granular materials. These systems utilize compressed air or gas to transport particles from one location to another, offering a dust-free and efficient alternative to traditional methods like belt conveyors or bucket elevators. HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a prominent provider of such equipment, known for its robust and reliable designs tailored to various industrial needs.
The Working Principle of Dust Gas-Pneumatic Conveying Machines
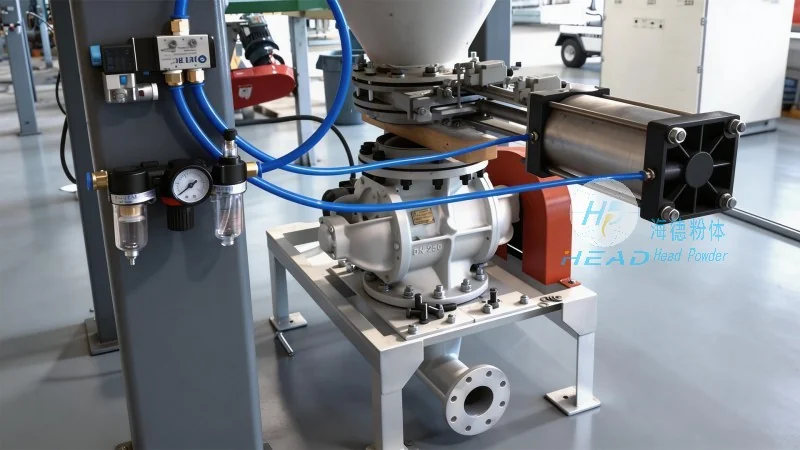
The core of a dust gas-pneumatic conveying system lies in its ability to use air flow to move material. Typically, the process involves a blower or compressor that generates high-pressure air. This air is then introduced into a pipeline, where it creates a low-pressure zone that draws the material into the system. The material is carried along the pipeline by the air stream, often in a dilute phase (where particles are suspended in the air) or a dense phase (where particles are more concentrated). The system may include components like inlets, cyclones for separation, and discharge points to control the flow and ensure proper material handling. The working principle is based on the principle of fluidization, where the air flow suspends the particles, allowing them to be transported over long distances without the need for mechanical contact, which minimizes wear and reduces the risk of contamination.
Key Features of Dust Gas-Pneumatic Conveying Equipment
HeadPowder's dust gas-pneumatic conveying machines are designed with several distinct features that enhance their performance and suitability for diverse applications. Firstly, they offer high efficiency in material transport, capable of moving large volumes of fine powders over significant distances with minimal energy consumption. The systems are also highly flexible, allowing for changes in the layout or direction of material flow without major modifications. Additionally, these machines are known for their dust control capabilities, as the enclosed system prevents dust from escaping into the environment, making them ideal for applications where air quality is a concern. Another notable feature is their ability to handle a wide range of materials, from abrasive powders to delicate particles, without causing degradation or damage. The equipment is also designed for easy maintenance, with accessible components that simplify routine checks and repairs. Furthermore, the systems are often equipped with advanced control systems that allow for precise regulation of air pressure, flow rate, and material feed, ensuring consistent and reliable operation. These features collectively make dust gas-pneumatic conveying equipment a preferred choice in industries such as pharmaceuticals, food processing, chemicals, and mining.
Applications and Benefits in Industrial Settings
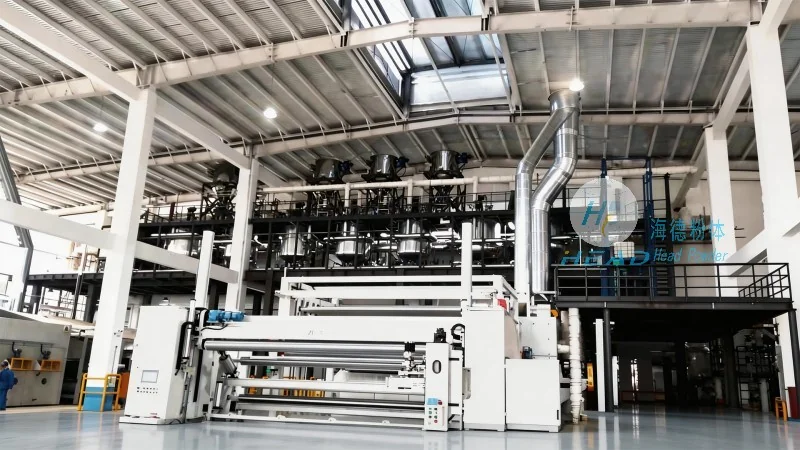
The versatility of dust gas-pneumatic conveying systems makes them indispensable in various industrial settings. In the pharmaceutical industry, for example, they are used to transport sensitive powders while maintaining strict hygiene standards. In food processing, they help in moving ingredients without cross-contamination, ensuring product safety. The chemical industry benefits from their ability to handle corrosive or hazardous materials safely, while the mining sector uses them to transport ore and other minerals efficiently. The primary benefits of these systems include reduced labor costs due to automated material handling, lower operational costs compared to traditional methods, and improved safety by eliminating manual handling of powders. Moreover, the enclosed design minimizes environmental impact by preventing dust emissions, aligning with modern sustainability goals. HeadPowder Engineering Co., Ltd. continues to innovate in this field, offering customized solutions that meet the specific requirements of each client, ensuring optimal performance and reliability.