Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions. Our company specializes in the design, manufacturing, and installation of silo bulk material conveying systems, which are essential for efficient material transport in various industrial applications. This article will explore the working principle and key features of these systems, highlighting how they enhance operational efficiency and reliability in material handling processes.
Overview of Silo Bulk Material Conveying Systems
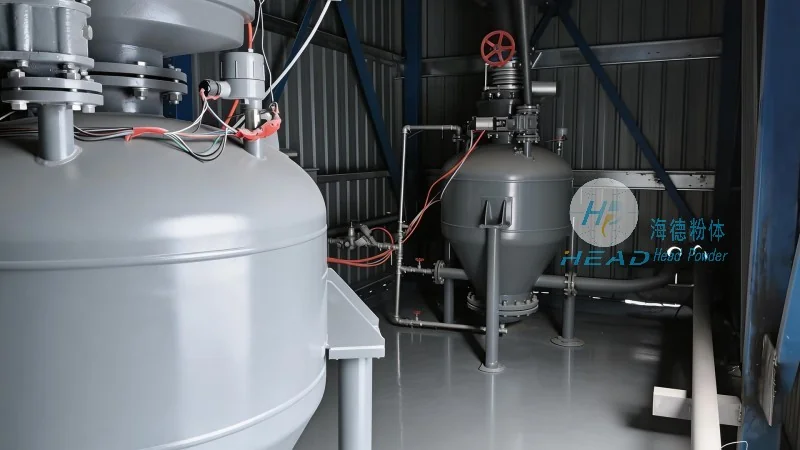
Silo bulk material conveying systems are engineered to transport powders, granules, and other bulk materials from storage silos to processing units, packaging lines, or other destinations within a facility. These systems are commonly used in industries such as food processing, pharmaceuticals, chemicals, and mining, where the safe and efficient movement of bulk materials is critical to operational success. The systems typically consist of a silo, a conveying mechanism (e.g., pneumatic or mechanical), and control components that ensure smooth and controlled material flow.
The Working Principle of Bulk Material Conveying Equipment
The core working principle of silo bulk material conveying systems revolves around the method of material transport. There are primarily two types of systems: pneumatic conveying and mechanical conveying. Pneumatic systems use air or other gases to move materials through a pipeline, while mechanical systems employ rotating components like screws or belts to transport materials. In pneumatic systems, material is drawn from the silo into a hopper and then propelled through the pipeline by compressed air. The air flow creates a negative pressure that pulls the material along, ensuring consistent and controlled transport. Mechanical systems, on the other hand, utilize screw conveyors or bucket elevators that physically move the material through the system. The choice of system depends on factors such as material characteristics, distance, and required flow rate.
Key Features and Advantages of Silo Bulk Material Conveying Systems
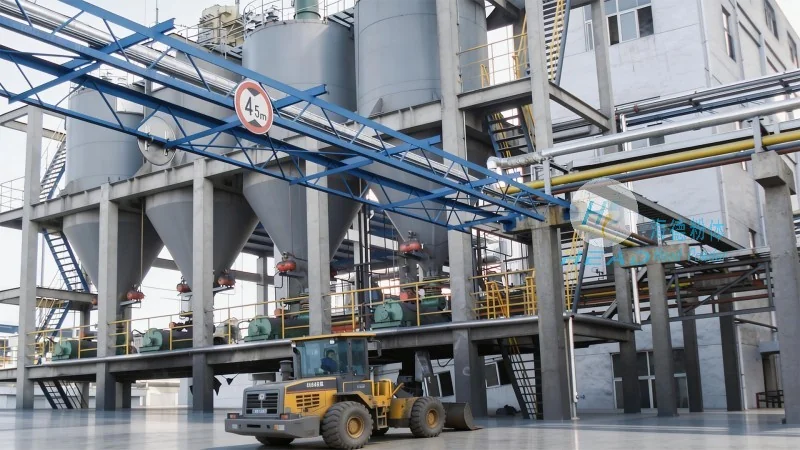
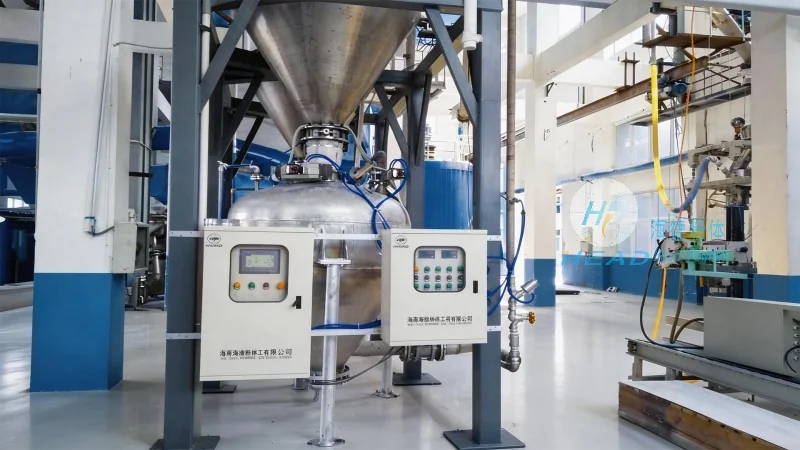
HeadPowder's silo bulk material conveying systems are designed with several key features that enhance performance and reliability. One of the primary advantages is their high efficiency in material transport, as they can handle large volumes of bulk materials with minimal downtime. The systems are also highly flexible, allowing for adjustments in flow rate and direction to accommodate varying production needs. Another important feature is their ability to maintain material integrity, preventing contamination or degradation during transport. This is particularly critical in industries like food and pharmaceuticals, where product quality is paramount. Additionally, these systems are equipped with advanced control systems that provide real-time monitoring and adjustment, ensuring optimal operation and reducing the risk of system failures.
Reliability and Durability in Industrial Applications
Reliability is a critical factor in bulk material handling, and HeadPowder's systems are built to withstand the demands of industrial environments. The components are constructed from high-quality materials, such as stainless steel and corrosion-resistant alloys, which ensure long-term durability and resistance to wear and tear. The systems are also designed with safety features, including pressure relief valves and emergency shut-off mechanisms, to prevent accidents and protect personnel. Regular maintenance and quality control measures are integral to the system's performance, ensuring that it operates at peak efficiency over its service life.
Customization and Integration with Existing Facilities
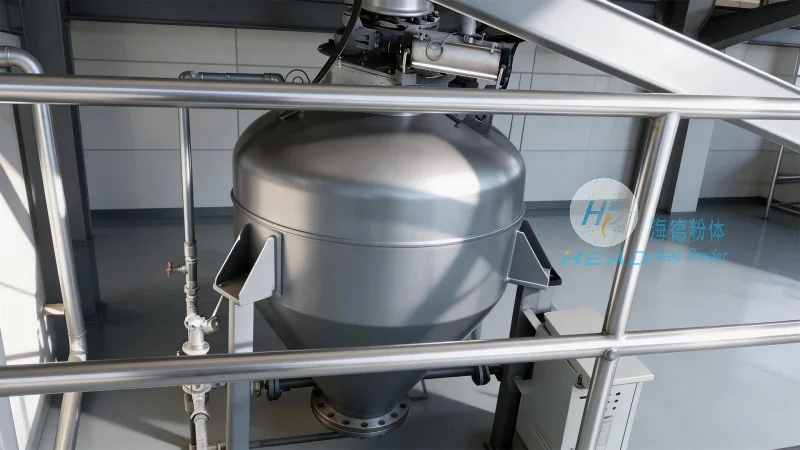
HeadPowder understands that each industrial facility has unique requirements, and our silo bulk material conveying systems are customizable to meet specific needs. We work closely with clients to design systems that integrate seamlessly with existing infrastructure, minimizing disruptions during installation. The systems can be tailored to handle a wide range of materials, from fine powders to coarse granules, and can be scaled to accommodate varying production capacities. Our team of engineers provides comprehensive support, from initial design and planning to installation and commissioning, ensuring that the system meets all operational and safety standards.
Conclusion
In conclusion, silo bulk material conveying systems are essential for efficient and reliable material handling in various industrial sectors. HeadPowder Engineering Co., Ltd. offers advanced solutions that combine innovative technology with robust design, providing customers with systems that enhance productivity, reduce costs, and ensure product quality. By understanding the working principles and key features of these systems, industries can make informed decisions to optimize their material transport processes and achieve long-term operational success.




