At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and implementation of efficient rice material conveying systems. These systems are crucial for the smooth operation of rice processing facilities, ensuring that raw rice is transported from storage to processing stages with minimal loss and maximum efficiency. Our expertise lies in understanding the unique properties of rice, such as its light weight, tendency to clump, and susceptibility to breakage, which require specialized equipment to handle effectively.
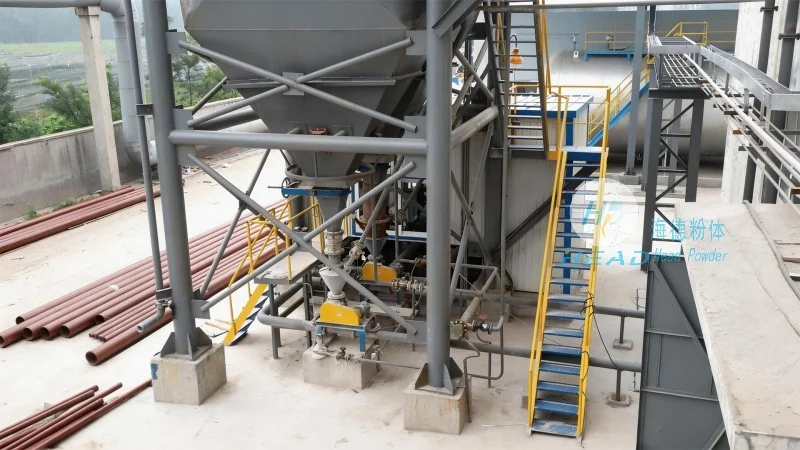
The working principle of rice material conveying systems typically involves a combination of mechanical components designed to move rice in a controlled manner. Common components include hoppers, feeders, conveyors (like belt conveyors, screw conveyors, or pneumatic conveyors), and control systems. The process begins with the rice being fed from storage bins or silos into a hopper. From there, a feeder regulates the flow of rice into the conveyor system. Belt conveyors are often used for horizontal or slight incline transport, while screw conveyors are suitable for vertical or inclined movement. Pneumatic conveyors, or air-based systems, use air pressure to transport rice in a closed pipeline, which is particularly effective for preventing contamination and maintaining product quality.
Key to the efficiency of these systems is the control mechanism. Modern rice conveying systems are equipped with sensors and control panels that monitor flow rates, pressure, and temperature. This allows for real-time adjustments to maintain optimal conditions, preventing issues like overloading or material blockages. The control system ensures that the conveying process is consistent and reliable, which is essential for maintaining the quality of the rice throughout the handling process.
One of the primary features of our rice material conveying systems is their ability to handle the delicate nature of rice. Unlike heavier bulk materials, rice requires equipment that minimizes impact and friction. This is achieved through the use of smooth, non-abrasive surfaces on conveyor belts and the design of screw conveyors with gradual inclines to prevent rice from breaking or being crushed. Additionally, the systems are designed to minimize dust generation, which is important for maintaining a clean and safe working environment in rice processing plants.
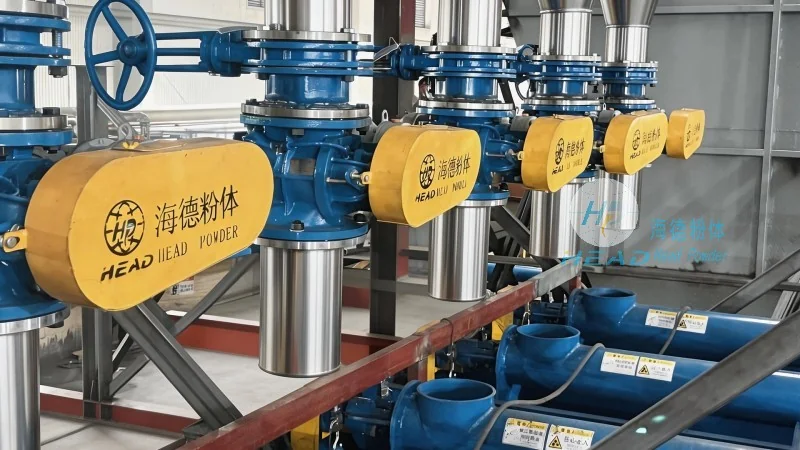
Another important feature is the flexibility of the conveying systems. They can be customized to fit the specific layout and requirements of a rice processing facility. Whether the facility is a small-scale operation or a large industrial plant, our systems can be scaled to meet the needs. The modular design allows for easy integration with existing equipment and future expansion as the business grows.
Efficiency is a critical characteristic of our rice material conveying systems. By reducing the time and labor required to move rice through the processing line, these systems increase overall productivity. The use of automated control systems minimizes human intervention, leading to more consistent results and reduced operational costs. Furthermore, the systems are designed to minimize material loss, which is crucial for maintaining profitability in rice processing.
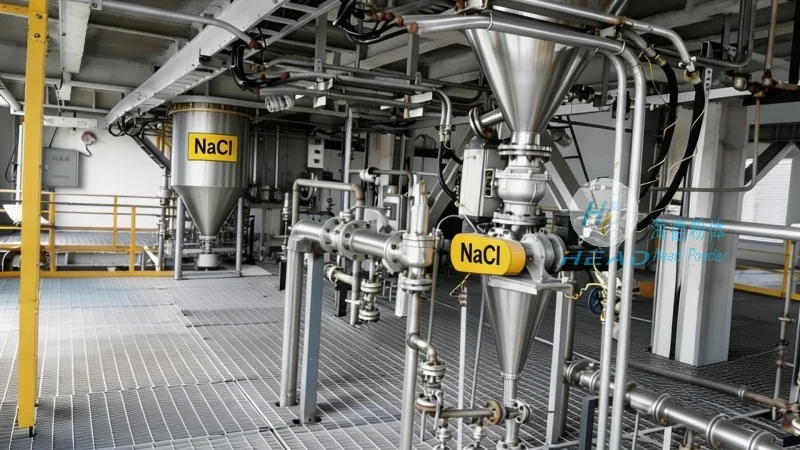
Reliability is another key feature that sets our systems apart. We use high-quality components and robust construction to ensure that the equipment operates continuously without frequent breakdowns. Regular maintenance and quality control measures are implemented to keep the systems in optimal condition. This reliability is essential for maintaining the smooth operation of rice processing facilities, especially during peak production periods.
At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing solutions that meet the specific needs of our clients. Our rice material conveying systems are designed to be not only efficient and reliable but also environmentally friendly. The use of energy-efficient motors and the reduction of material waste contribute to a more sustainable operation. We also prioritize the safety of our clients' operations, ensuring that all systems comply with relevant safety standards and regulations.
In conclusion, the working principle and features of rice material conveying systems are tailored to the unique requirements of rice handling. By combining advanced technology with careful design, these systems ensure that rice is transported safely and efficiently from storage to processing. At HeadPowder, we continue to innovate and improve our systems to meet the evolving needs of the rice processing industry, providing our clients with the best possible solutions for their material handling challenges.




