Positive pressure blown pneumatic conveying systems represent a sophisticated method for transporting bulk materials through a pipeline using compressed air. This technology is widely utilized across various industries due to its efficiency, flexibility, and ability to handle a diverse range of materials. The fundamental principle behind this system involves generating a positive pressure within the conveying line, which propels the material forward by creating a pressure differential between the inlet and outlet.
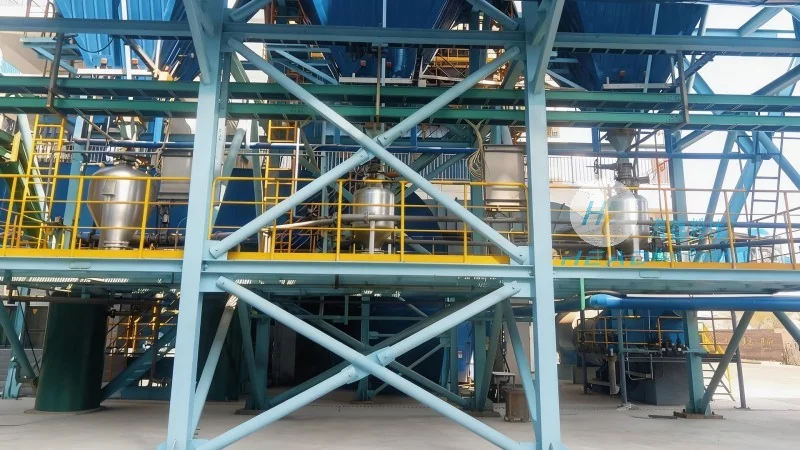
Principle of Positive Pressure Blown Pneumatic Conveying
The core mechanism of positive pressure systems relies on the injection of high-pressure air or gas into the material stream at the inlet. This pressurized air mixes with the bulk material, forming a dense, homogeneous mixture known as a "slurry" or "conveying stream." The pressure differential between the high-pressure inlet and the lower-pressure outlet drives the material along the pipeline. The velocity of the air and the density of the material mixture determine the conveying capacity and efficiency. Key components include the material hopper, air compressor, pressure regulator, and the conveying pipeline itself. The system operates by first loading the material into the hopper, then activating the air compressor to generate the necessary pressure. As air is introduced into the material, the mixture is forced through the pipeline to the discharge point. The pressure is maintained throughout the system to ensure consistent material flow, minimizing the risk of clogging or material degradation.
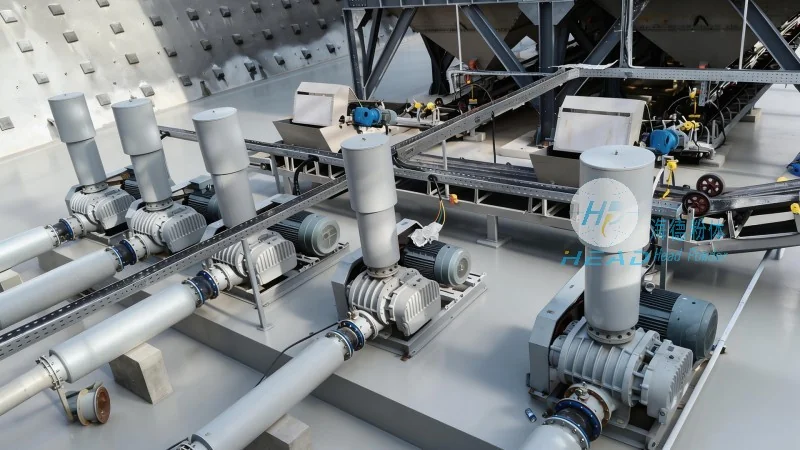
Working Scene Characteristics and Applications
Positive pressure blown pneumatic conveying is particularly suited for applications where materials need to be transported over long distances or through complex layouts. Its ability to handle abrasive or sensitive materials makes it ideal for industries such as food processing, pharmaceuticals, chemicals, and minerals. The system is commonly used in scenarios where traditional gravity or mechanical conveying methods are impractical due to the nature of the material or the layout of the facility. For instance, in food processing plants, positive pressure systems are used to transport powders like flour, sugar, or spices from storage silos to processing lines without the risk of contamination or material degradation. In pharmaceutical manufacturing, the system ensures that sensitive active ingredients are handled hygienically and efficiently, maintaining the integrity of the product. In chemical plants, it can transport powders like pigments, catalysts, or reagents with minimal risk of cross-contamination or dust exposure. The flexibility of the system allows for easy integration into existing production lines, and its compact design makes it suitable for both new installations and retrofitting in existing facilities.
Advantages and Considerations in Operational Scenarios
One of the primary advantages of positive pressure blown pneumatic conveying is its ability to handle a wide variety of materials, including fine powders, granules, and even wet or sticky substances. The high-pressure air ensures that the material is fully suspended and transported without the need for additional mechanical components like screws or belts. This reduces maintenance costs and increases operational reliability. Another key benefit is the system's efficiency in terms of energy consumption, as the compressed air can be recycled and reused within the system, minimizing waste. However, operational considerations must be taken into account, such as the need for proper air filtration to prevent dust accumulation in the system and the importance of regular maintenance to ensure consistent performance. The system's design must also account for the specific properties of the material being conveyed, such as its density, flowability, and potential for caking or agglomeration. In addition, the pressure levels required may vary depending on the distance and complexity of the conveying path, necessitating careful engineering and sizing of the components.
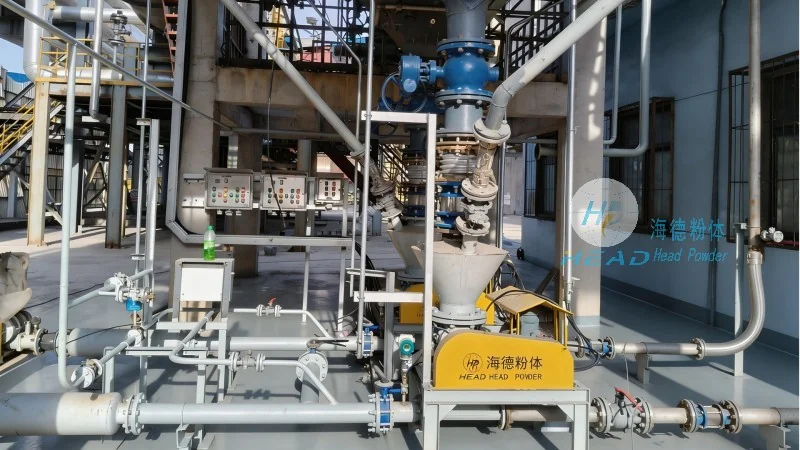
About HeadPowder Engineering and Their Expertise
HeadPowder Engineering, a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing positive pressure blown systems tailored to the unique needs of various industries. With a strong presence in Shandong, China, the company leverages over years of experience in the field to deliver high-quality, reliable equipment. HeadPowder Engineering's team of engineers and technicians work closely with clients to understand their specific material handling challenges and develop customized solutions that optimize performance and efficiency. The company's commitment to quality and innovation ensures that their systems meet the highest industry standards, providing long-term value and operational excellence. By partnering with HeadPowder Engineering, businesses can benefit from expert guidance and support throughout the entire process, from initial design and installation to ongoing maintenance and troubleshooting. This collaborative approach helps ensure that the chosen pneumatic conveying system is perfectly suited to the client's operational requirements and contributes to overall productivity and cost savings.




