Intelligent bulk bag unloading powder handling equipment represents a sophisticated solution designed to streamline the process of handling and transferring bulk powders from bulk bags. This equipment is engineered to enhance efficiency, safety, and accuracy in industrial applications where bulk powders are commonly used. The system integrates advanced technologies to automate the unloading, conveying, and storage of powders, making it an essential asset for industries such as pharmaceuticals, food processing, chemicals, and more. By understanding the operation process and working principle of this equipment, users can appreciate its role in optimizing material handling workflows.
Key Components and Their Functions
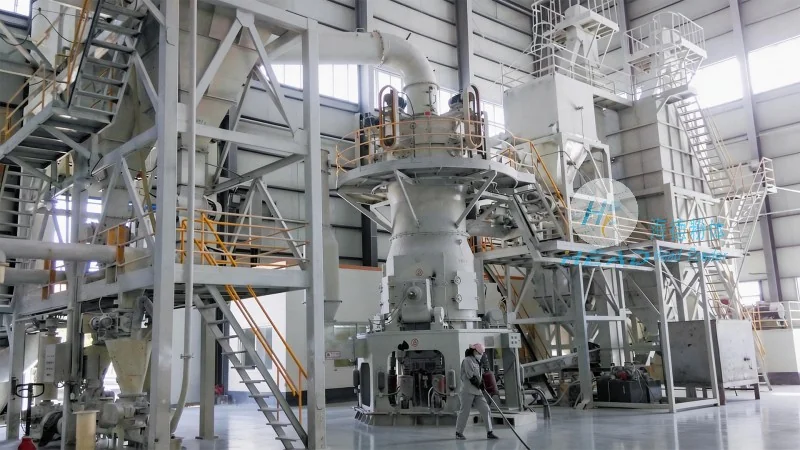
The intelligent bulk bag unloading powder handling system consists of several critical components that work in tandem to achieve efficient operation. The primary components include the bulk bag lifting and support mechanism, the powder discharge valve, the conveying system (such as pneumatic or mechanical conveyors), and the storage or processing equipment. Each component plays a vital role in ensuring the smooth and safe transfer of powders. For instance, the bulk bag lifting mechanism securely holds the bag in place, preventing it from tipping or shifting during the unloading process. The discharge valve controls the flow of powder from the bag, allowing for precise regulation of the discharge rate. The conveying system then transports the powder to the desired destination, whether it be a storage silo, processing unit, or other equipment. The integration of these components ensures a seamless workflow from bag unloading to final use.
Operation Process: Step-by-Step Guide
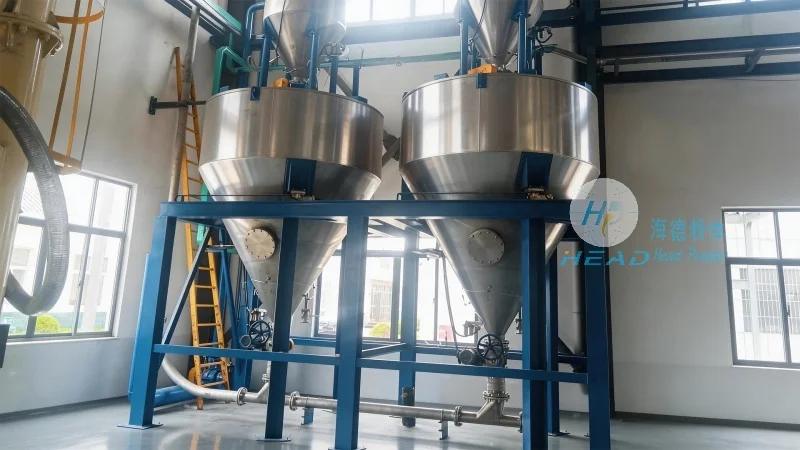
The operation of the intelligent bulk bag unloading powder handling equipment follows a systematic sequence of steps. The process begins with the placement of the bulk bag onto the lifting frame. The lifting mechanism then secures the bag, ensuring stability during the unloading phase. Next, the discharge valve is activated, allowing the powder to flow out of the bag. Simultaneously, the conveying system is engaged, which may involve air pressure or mechanical force to move the powder through the system. The powder is then directed to the storage or processing equipment, where it is either stored for later use or transferred to the next stage of production. Throughout the process, sensors and controls monitor the flow rate, pressure, and other parameters to maintain optimal performance. The system is designed to stop automatically if any anomalies are detected, such as blockages or overfilling, ensuring safety and preventing material loss. This step-by-step operation ensures that the equipment operates efficiently and reliably, minimizing downtime and maximizing productivity.
Working Principle: How It Works
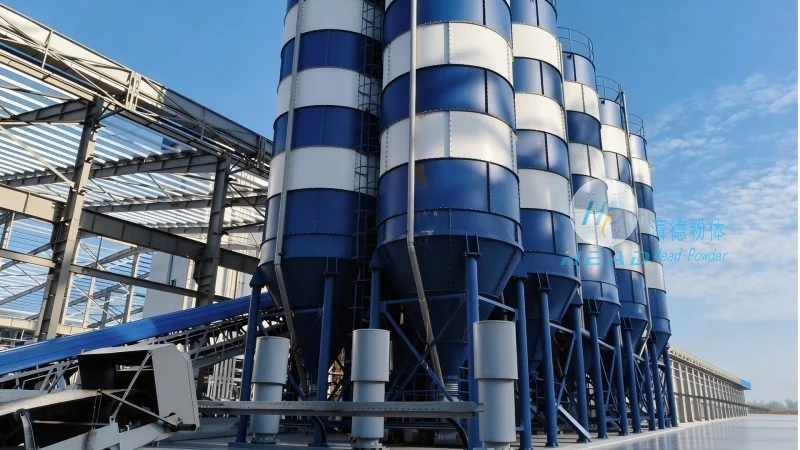
The working principle of the intelligent bulk bag unloading powder handling equipment is based on a combination of mechanical, pneumatic, and control technologies. The core of the system is the bulk bag unloading mechanism, which uses a combination of lifting and discharge valves to extract the powder from the bag. The lifting frame supports the bag, while the discharge valve controls the flow of powder. The conveying system, typically a pneumatic conveyor, uses air pressure to move the powder from the bag to the storage or processing equipment. The control system, often integrated with sensors, monitors the entire process and adjusts parameters as needed to maintain optimal performance. For example, if the powder flow rate is too high, the system can reduce the air pressure to regulate the flow. Similarly, if the storage silo is nearly full, the system can pause the unloading process to prevent overfilling. This integrated approach ensures that the equipment operates efficiently and safely, adapting to changing conditions in real-time. The working principle also emphasizes safety features, such as automatic shut-off in case of blockages or overpressure, to protect both the equipment and personnel.
Benefits and Applications
The intelligent bulk bag unloading powder handling equipment offers numerous benefits to industrial operations. One of the primary advantages is increased efficiency, as the automated process reduces the need for manual labor and minimizes downtime. The system also enhances safety by eliminating the risk of manual handling of heavy or hazardous bulk bags. Additionally, the precise control of powder flow ensures accurate dosing, which is critical in applications such as pharmaceutical manufacturing where consistency is paramount. The equipment is versatile and can handle a wide range of powders, including fine powders, granules, and bulk materials. It is commonly used in industries such as pharmaceuticals, food processing, chemicals, and agriculture. The system's ability to integrate with existing production lines makes it a cost-effective solution for upgrading material handling processes. Overall, the intelligent bulk bag unloading powder handling equipment is a valuable asset for any industry that relies on bulk powders, providing a reliable and efficient solution for handling and transferring these materials.
Conclusion
In conclusion, the intelligent bulk bag unloading powder handling equipment is a sophisticated and efficient solution for managing bulk powders in industrial settings. By understanding its operation process and working principle, users can appreciate how this equipment enhances productivity, safety, and accuracy in material handling workflows. The integration of advanced components and control systems ensures that the equipment operates reliably and adapts to changing conditions. As a result, it is an essential tool for industries that require consistent and safe handling of bulk powders. The equipment's design and functionality make it a valuable investment for any business looking to optimize its material handling processes and improve overall operational efficiency.




