High-pressure bin pumps are critical components in modern material handling and bulk material transport systems, designed to efficiently and reliably move powders, granules, and other bulk materials over long distances with minimal pressure loss. This article provides a detailed overview of the operation process and working principles of high-pressure bin pump equipment, highlighting its key features, operational steps, and technical advantages. The information is presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in bulk material handling solutions.
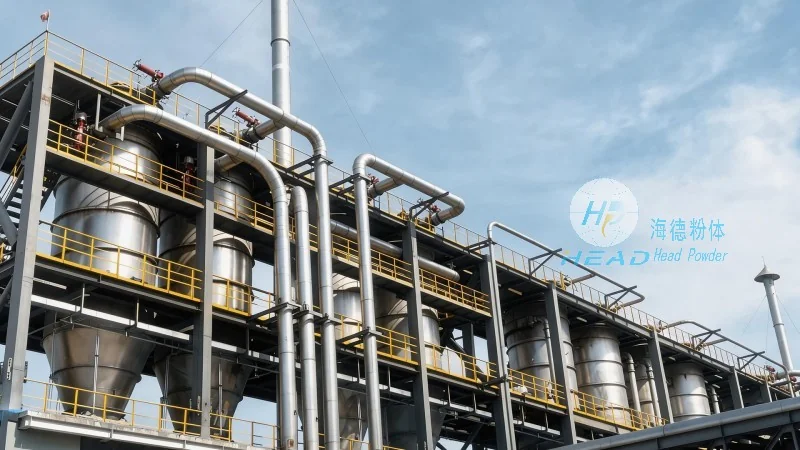
Overview of High-Pressure Bin Pump Systems
High-pressure bin pumps, also known as pressure bins or pneumatic conveying systems, are engineered to handle a wide range of bulk materials, including cement, coal, minerals, and chemicals. These systems operate by creating a pressure differential between the material storage bin and the discharge point, enabling the material to be transported through pipelines under pressure. The core components of a typical high-pressure bin pump system include a storage bin, a pump unit, conveying pipelines, and a control system. The pump unit is responsible for generating the necessary pressure to move the material, while the pipelines ensure the material is transported to the desired location. The control system monitors and regulates the operation of the pump and other components to ensure safe and efficient material handling.
Key Components and Their Functions
The high-pressure bin pump system consists of several key components, each playing a vital role in the overall operation. The storage bin, or hopper, is where the bulk material is stored before being conveyed. It is typically equipped with a feeding mechanism, such as a rotary valve or a gate valve, to control the flow of material into the pump. The pump unit, which is the heart of the system, generates the pressure required to move the material. It is usually a positive displacement pump, such as a diaphragm pump or a piston pump, that can handle high pressures and abrasive materials. The conveying pipelines are made of durable materials, such as stainless steel or polyethylene, to withstand the pressure and wear from the material being transported. The control system includes sensors, valves, and a control panel that monitor the pressure, flow rate, and other parameters to ensure the system operates within safe limits.
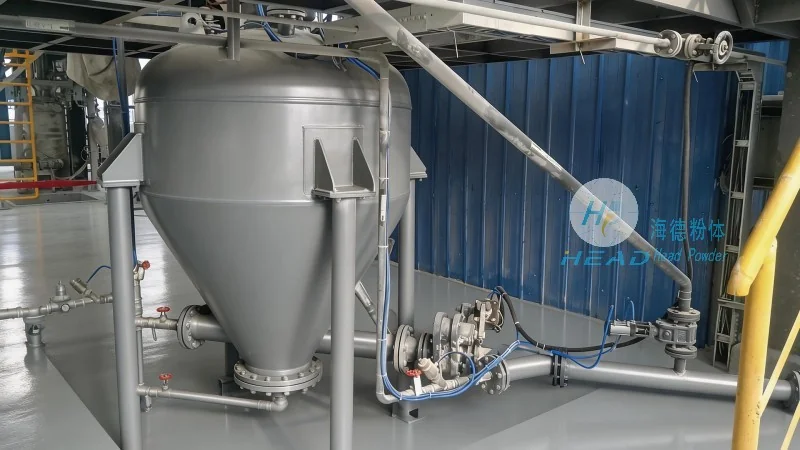
Operation Process of High-Pressure Bin Pump Equipment
The operation of a high-pressure bin pump system involves several steps, each designed to ensure the material is transported efficiently and safely. The process begins with the material being fed into the storage bin from a hopper or a silo. The feeding mechanism controls the flow rate of the material into the pump, ensuring a consistent supply. The pump unit then generates the necessary pressure to move the material through the conveying pipelines. As the material is pushed through the pipelines, it is mixed with a small amount of air or gas, which helps to reduce friction and prevent blockages. The material is then discharged at the end of the pipeline, where it is collected in a receiving bin or a storage tank. The control system continuously monitors the pressure and flow rate, adjusting the pump speed or feeding rate as needed to maintain optimal operation. The entire process is automated, with the control system ensuring that the system operates smoothly and without interruption.
Working Principle of High-Pressure Bin Pump Systems
The working principle of a high-pressure bin pump system is based on the principles of fluid dynamics and pressure differential. The system operates by creating a pressure difference between the inlet and outlet of the pump. The pump unit draws material from the storage bin and compresses it, increasing the pressure. The high-pressure material is then forced through the conveying pipelines to the discharge point. The pressure differential ensures that the material moves continuously through the system, without the need for additional energy input. The system is designed to handle a wide range of materials, from fine powders to coarse granules, and can transport materials over long distances with minimal pressure loss. The use of positive displacement pumps ensures that the material is moved at a consistent rate, regardless of the pressure or flow rate.
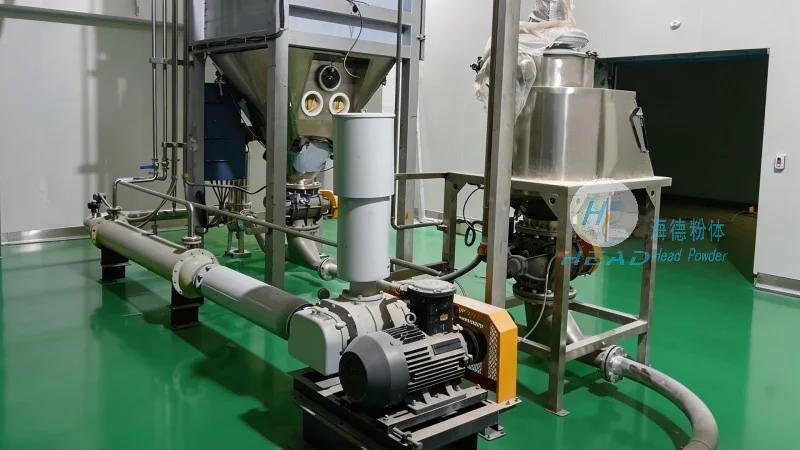
Advantages of High-Pressure Bin Pump Equipment
High-pressure bin pump systems offer several advantages over traditional material handling methods, such as belt conveyors or bucket elevators. The primary advantage is the ability to transport materials over long distances with minimal pressure loss, which reduces the need for additional pumping stations. The system is also highly efficient, with low energy consumption and minimal maintenance requirements. The use of positive displacement pumps ensures that the material is moved at a consistent rate, which improves the overall productivity of the system. Additionally, the system is flexible and can be easily integrated with other equipment, such as storage bins or processing units. The high-pressure bin pump system is also safe and reliable, with built-in safety features that prevent overpressure and material blockages.
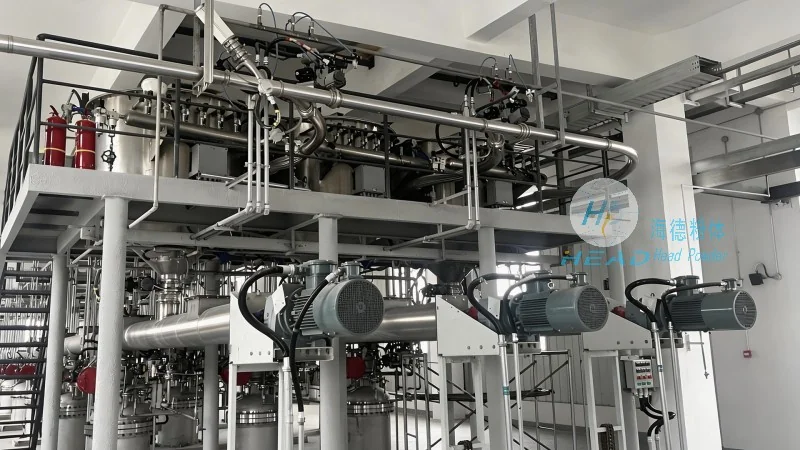
Applications of High-Pressure Bin Pump Systems
High-pressure bin pump systems are widely used in various industries, including cement, coal, minerals, and chemicals. They are commonly used to transport materials from storage bins to processing units, such as cement mills or coal crushers. The system is also used in the food and pharmaceutical industries to transport powders and granules, where hygiene and safety are critical. The high-pressure bin pump system is also used in the construction industry to transport cement and other building materials to job sites. The system's ability to handle a wide range of materials and its flexibility make it an ideal solution for various material handling applications.
Conclusion
High-pressure bin pump equipment is a critical component in modern material handling systems, offering efficient and reliable transport of bulk materials over long distances. The operation process and working principles of these systems are based on the principles of fluid dynamics and pressure differential, with key components working together to ensure optimal performance. The advantages of high-pressure bin pump systems, including efficiency, flexibility, and safety, make them a preferred choice for various industries. Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of high-pressure bin pump systems, providing customized solutions to meet the specific needs of clients. With its commitment to quality and innovation, the company is a leading provider of bulk material handling solutions in China.




