The ash tank material conveying system is a critical piece of industrial equipment designed to efficiently transport bulk materials, particularly in power plants and waste management facilities. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality solutions that ensure reliable and safe material handling. This article delves into the operation process and working principle of such systems, highlighting the key aspects that make them indispensable in modern industrial operations.
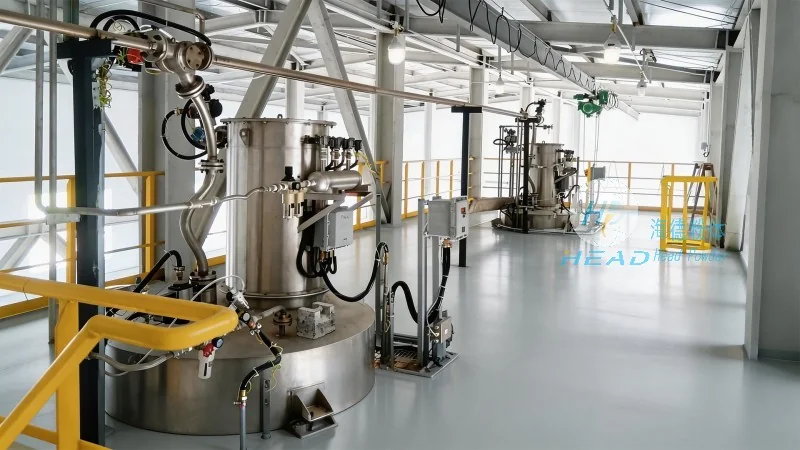
Overview of the Ash Tank Material Conveying System
The ash tank material conveying system, also known as an ash handling system, is engineered to manage the transportation of ash and other solid waste materials from their source to disposal or processing sites. These systems are typically integrated into larger industrial setups, such as thermal power plants, where the efficient removal of ash is essential for maintaining operational efficiency and environmental compliance. The system comprises several interconnected components, including ash tanks, conveyor belts, pumps, and control systems, all working in harmony to achieve seamless material transfer.
Key Components and Their Roles
Each component of the ash tank material conveying system plays a vital role in the overall operation. The ash tank, often a large, cylindrical container, serves as the primary storage unit for the material. It is designed to withstand high temperatures and corrosive substances, ensuring durability and safety. The conveyor system, which may include belt conveyors, screw conveyors, or pneumatic conveyors, is responsible for moving the material from the tank to the next stage of processing. Pumps, particularly slurry pumps, are used to transport liquid or semi-liquid ash, while control systems monitor and regulate the entire process, ensuring optimal performance and preventing malfunctions.
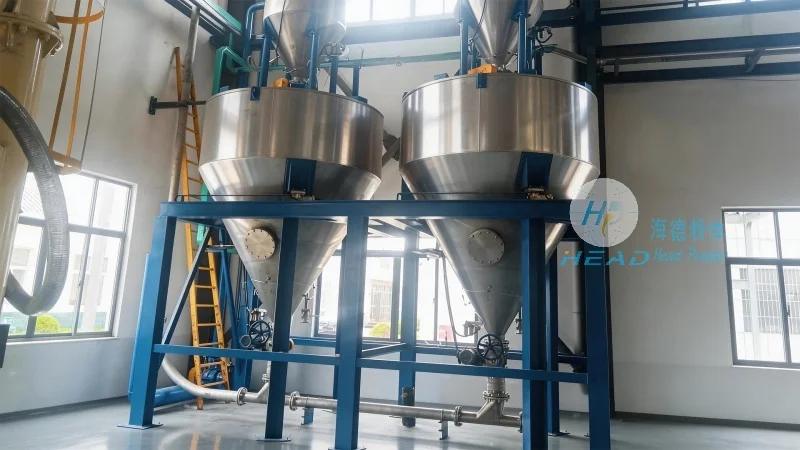
Operation Process: Step-by-Step Execution
The operation of the ash tank material conveying system follows a systematic sequence of steps. Initially, the ash is collected and deposited into the ash tank. Once the tank reaches a certain level, the control system activates the conveyor system, which begins to transport the material. The conveyor may move the ash to a processing unit, a storage facility, or directly to disposal sites. The process is continuous, with the system operating 24/7 to maintain a steady flow of material. Regular maintenance checks are performed to ensure all components are functioning correctly, minimizing downtime and maximizing efficiency.
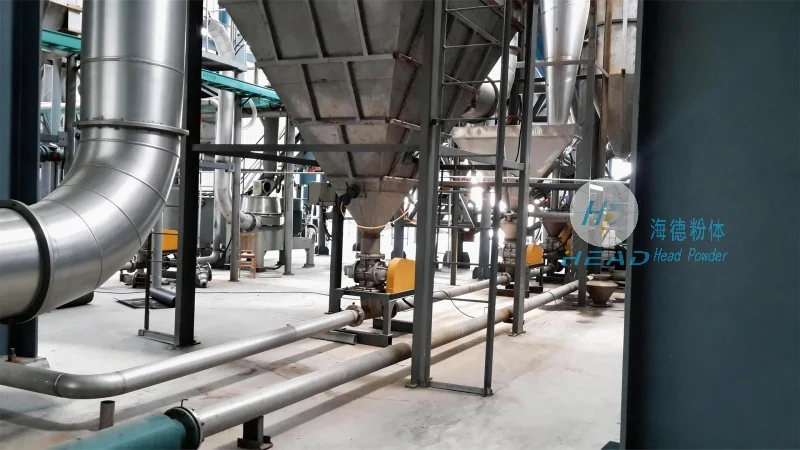
Working Principle: Mechanism and Technology
The working principle of the ash tank material conveying system is based on mechanical and hydraulic systems that work together to move the material. For solid ash, belt conveyors use friction to pull the material along a path, while screw conveyors use rotating screws to push the material forward. In cases where the ash is in a slurry form, pneumatic conveyors use air pressure to transport the material through pipes. The control system uses sensors and feedback mechanisms to adjust the speed and direction of the conveyor, ensuring precise control over the material flow. This integrated approach allows for efficient and reliable material handling, even in challenging conditions.
Company Information and Contact Details
Shandong HeadPowder Engineering Co., Ltd. is a reputable manufacturer based in Shandong, China, dedicated to providing advanced industrial solutions. With years of experience in the field, the company specializes in designing and manufacturing high-quality ash tank material conveying systems tailored to the specific needs of its clients. The company's commitment to quality, safety, and innovation has made it a trusted partner in the industrial sector. For more information about their products and services, please contact the company at their address in Shandong, China.




