HeadPowder, a prominent manufacturer headquartered in Shandong, China, specializes in the development and production of advanced fertilizer pneumatic conveying systems. These systems are engineered to efficiently transport bulk fertilizers, offering significant advantages over traditional mechanical conveyors such as reduced maintenance costs, lower energy consumption, and the ability to handle materials with high moisture or abrasive characteristics. The system is tailored to meet the specific demands of the agricultural and industrial sectors, providing a flexible and efficient solution for material handling in fertilizer processing and distribution.
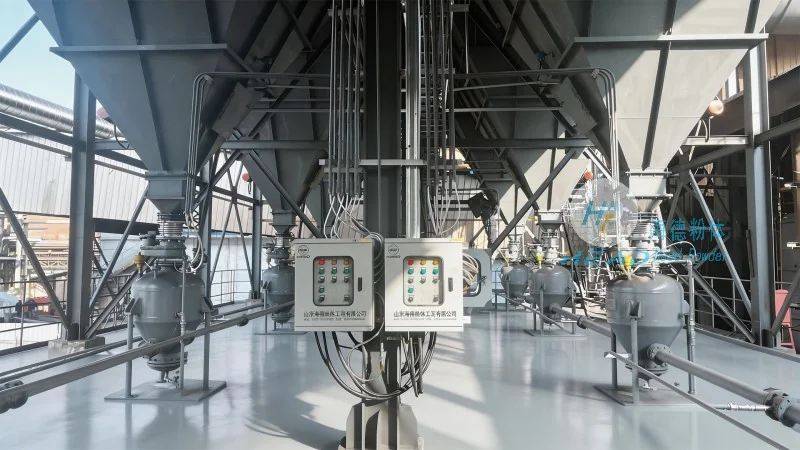
Overview of Fertilizer Pneumatic Conveying Systems
At the heart of our product line is the fertilizer pneumatic conveying system, a technology that utilizes air pressure to move bulk materials through a pipeline network. This method provides several key benefits, including reduced material degradation, lower operational costs, and enhanced safety compared to mechanical systems. The system is designed to handle a wide variety of fertilizer types, from granular to powdered forms, and can be customized to accommodate different flow rates and distances. By leveraging air as the conveying medium, the system minimizes the need for physical contact with the material, ensuring consistent quality and preventing contamination.
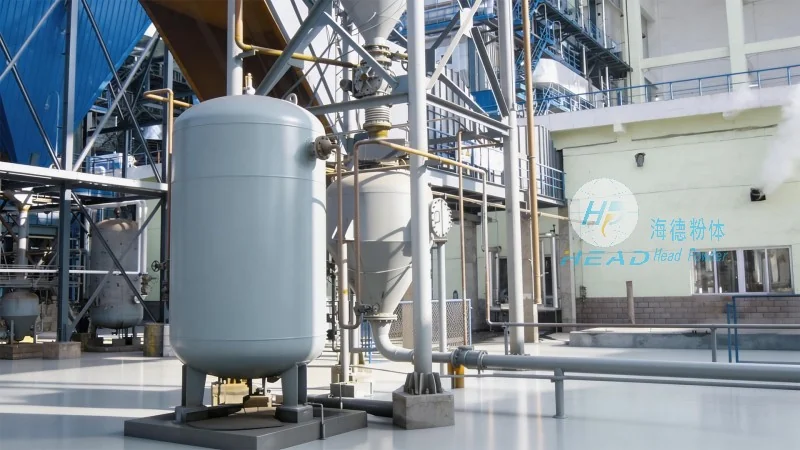
Structural Components and Working Principle
The fertilizer pneumatic conveying system comprises several critical components, each contributing to the overall functionality. The primary components include the material hopper, which stores the fertilizer; the air compressor, responsible for generating the necessary air pressure; the pipeline system, which transports the material; and the control unit, which regulates the flow and pressure. The working principle involves feeding the fertilizer into the hopper, where it is then drawn into the pipeline by the air flow generated by the compressor. The air and material mixture travels through the pipeline to the discharge point, where the material is separated from the air and collected. This process is continuous and can be adjusted to handle varying material volumes and flow rates, ensuring optimal performance under different operational conditions. The system can operate in both positive and negative pressure modes, allowing flexibility in the layout and design of the conveying network.
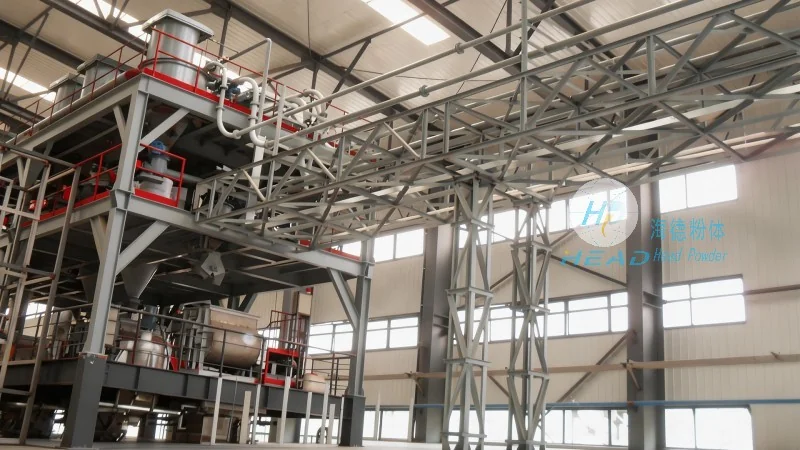
Key Features and Technical Advantages
Our fertilizer pneumatic conveying systems are equipped with several features that enhance their performance and reliability. One of the primary advantages is the ability to handle a wide range of fertilizer types, including those with high moisture content or corrosive properties, without causing material degradation or blockages. The system offers high conveying capacities, enabling the transport of large quantities of material over long distances with minimal loss. Additionally, the design incorporates advanced control systems that provide real-time monitoring of pressure, flow, and material levels, allowing operators to adjust the system parameters as needed. This ensures consistent performance and reduces downtime, making it an ideal choice for continuous production environments. The system also features energy-efficient air compressors and optimized pipeline designs, further reducing operational costs and environmental impact.
Applications in Fertilizer Industry
The fertilizer pneumatic conveying system is widely utilized in various stages of the fertilizer production and distribution process. In the manufacturing plant, it is used to transport raw materials from storage to processing units, and to move finished products from the production line to packaging areas. During the distribution phase, the system efficiently transports bulk fertilizers to storage facilities or directly to farms, ensuring timely delivery and reducing handling costs. The system's ability to handle different fertilizer formulations, such as nitrogen-based, phosphorus-based, or complex compound fertilizers, makes it suitable for a variety of applications. It is particularly effective in handling granular fertilizers, which are commonly used in agricultural applications, and can be adapted to handle powdered or liquid fertilizers with appropriate modifications. The system's flexibility allows it to be integrated into existing production lines or used as a standalone solution for material handling needs.
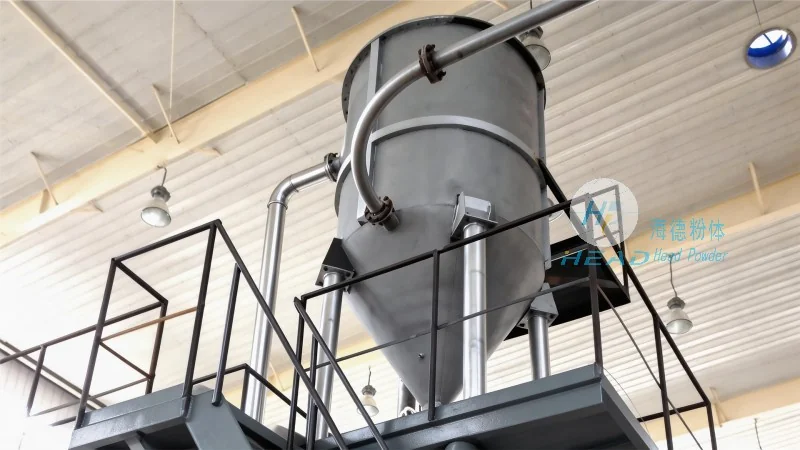
Installation and Maintenance Considerations
Proper installation and regular maintenance are crucial for the long-term performance and reliability of the fertilizer pneumatic conveying system. During installation, it is essential to ensure that the pipeline is properly aligned and supported to prevent sagging or damage. The air compressor and other components should be placed in a well-ventilated area to prevent overheating and ensure optimal performance. Regular maintenance includes checking the air filter, cleaning the pipeline, and inspecting the material hopper for any blockages or wear. The system's control unit should be checked regularly to ensure that all sensors and controls are functioning correctly. By following these guidelines, the system can operate efficiently for many years, providing consistent performance and minimizing the risk of breakdowns. Additionally, our team provides comprehensive installation and maintenance services to ensure that the system is set up correctly and remains in optimal condition throughout its operational life.




