The tonne bag quantitative feeding powder material handling system is a specialized equipment designed for efficient and precise material transfer in industrial applications. This system is particularly valuable in sectors that require large-scale handling of bulk powders, such as chemical, food, and pharmaceutical industries. The system's primary function is to automate the process of feeding and transporting powder materials from tonne bags to processing units, ensuring consistent and accurate dosing while maintaining operational safety and efficiency.
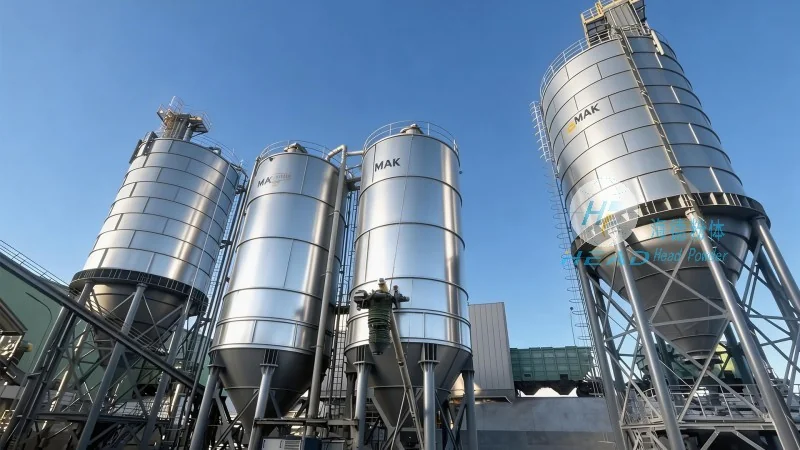
System Overview and Key Components
The tonne bag quantitative feeding system typically consists of several integrated components that work in harmony to achieve its objectives. The core elements include a tonne bag discharging mechanism, a quantitative feeding hopper, a conveyor system, and a control unit. Each component is engineered to handle the specific challenges of bulk powder handling, such as preventing material bridging, ensuring uniform flow, and maintaining hygiene standards. The tonne bag discharging unit is designed to safely open and empty the bag contents into the feeding hopper. This component often incorporates features like a bag clamp or a sealing system to prevent dust emission and ensure complete material extraction. The quantitative feeding hopper is equipped with a flow control valve and a weight measurement device, which allows for precise control over the amount of material dispensed. The conveyor system then transports the material to the processing equipment, ensuring a smooth and continuous flow. The control unit, often integrated with sensors and automation technology, monitors the entire process, adjusts parameters as needed, and provides real-time feedback on the system's performance.
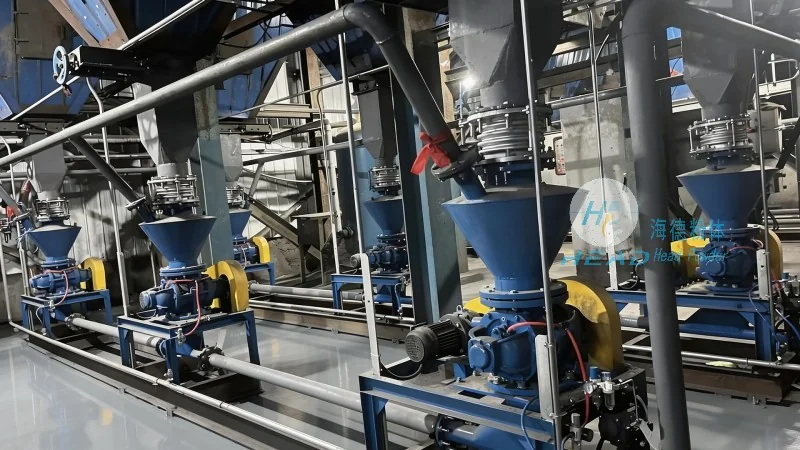
Working Principle of the Tonne Bag Quantitative Feeding System
The operation of the tonne bag quantitative feeding system follows a systematic sequence that ensures accurate and reliable material handling. Initially, the tonne bag is positioned over the discharging unit, which secures the bag and prepares it for emptying. The system then activates the discharge mechanism, which may involve a combination of air pressure, vibration, or mechanical agitation to facilitate material flow from the bag into the feeding hopper. As the material enters the hopper, the flow control valve regulates the rate of discharge, ensuring that the material is fed at a consistent and controlled pace. Simultaneously, the weight measurement device within the hopper continuously monitors the mass of material being added, allowing the system to adjust the flow rate in real-time to achieve the desired quantity. Once the target weight is reached, the control unit signals the system to stop the discharge. The conveyor system then transports the measured material to the downstream processing equipment, completing the feeding cycle. This closed-loop control system ensures high accuracy in material dosing, minimizing waste and optimizing production efficiency.
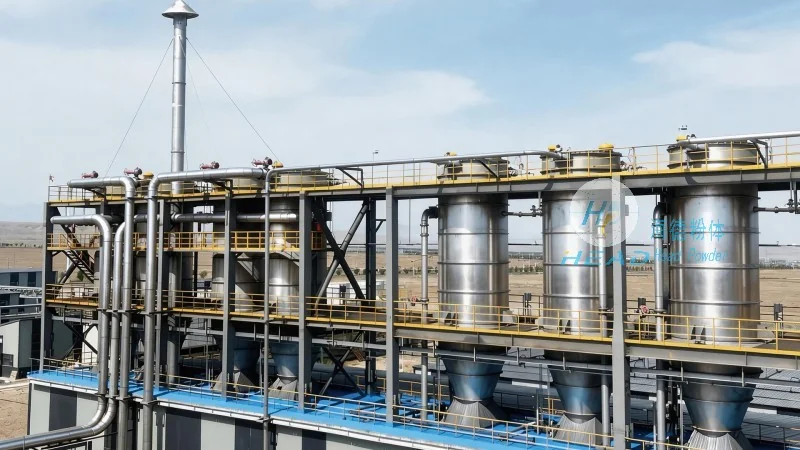
Advantages and Applications of the Tonne Bag Quantitative Feeding System
The tonne bag quantitative feeding system offers several advantages that make it an ideal choice for industrial applications. One of the key benefits is its ability to handle large volumes of bulk powders with high precision, reducing the risk of over or under-dosing. This accuracy is crucial in industries where material consistency directly impacts product quality, such as in the production of pharmaceuticals or food products. Additionally, the system enhances operational efficiency by automating the material handling process, reducing the need for manual intervention and labor costs. The design of the system also prioritizes safety and hygiene, with features like dust containment and easy cleaning, which are essential in industries with strict regulatory requirements. The system's versatility allows it to be adapted to various material types and processing requirements, making it suitable for a wide range of applications. In the chemical industry, for example, it can handle reactive powders with controlled dosing to prevent hazardous reactions. In the food industry, it ensures that ingredients are added in precise amounts to maintain product consistency and safety standards. Overall, the tonne bag quantitative feeding system provides a reliable and efficient solution for bulk powder handling, contributing to improved productivity and product quality in industrial settings.
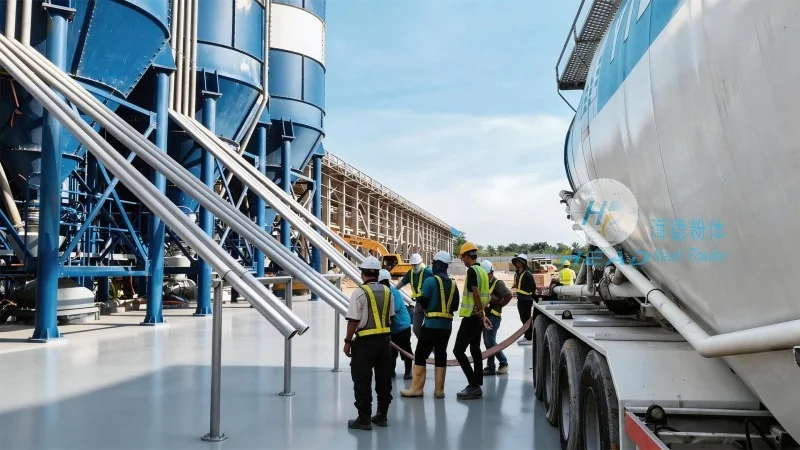
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in the design and production of advanced powder handling equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry, providing solutions tailored to the specific needs of various sectors. HeadPowder's expertise lies in developing customized systems that meet the unique requirements of clients, ensuring optimal performance and reliability. The company's products are engineered with precision and durability in mind, reflecting its dedication to delivering high-quality solutions. HeadPowder operates from China, leveraging local manufacturing capabilities and industry expertise to serve global markets effectively. The company's focus on customer satisfaction and technical excellence has earned it a reputation for providing reliable and efficient powder handling solutions that enhance operational efficiency and product quality for its clients.




