Calcined ash, a byproduct of industrial processes such as coal combustion in power plants, requires efficient and reliable transport methods for handling and disposal. Pneumatic conveying systems have emerged as a preferred solution due to their ability to handle fine powders like calcined ash with minimal dust generation and high operational efficiency. This article explores the various types of pneumatic conveying systems designed for calcined ash, their key characteristics, and the diverse applications where they are utilized.
Types of Pneumatic Conveying Systems for Calcined Ash
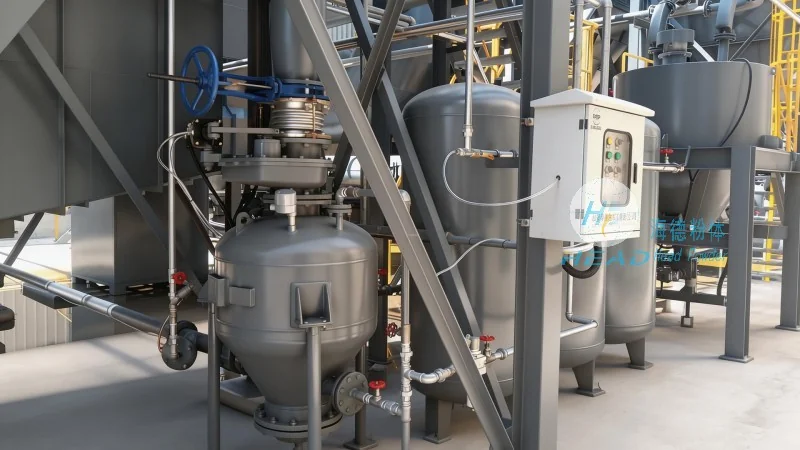
There are primarily two main categories of pneumatic conveying systems used for calcined ash: dilute-phase and dense-phase systems. Each type offers distinct advantages based on the material properties and operational requirements.
Dilute-phase pneumatic conveying systems operate by suspending the calcined ash particles in a high-velocity air stream. This method is suitable for short to medium-distance transport and is ideal for materials with low to moderate moisture content. The system typically uses positive pressure or negative pressure to move the material, with positive pressure being more common due to its ability to handle longer distances and higher material loads. Dense-phase pneumatic conveying, on the other hand, involves transporting the calcined ash in a slurry-like state, where the particles are closely packed and move at a lower velocity. This method is particularly effective for handling materials that are prone to caking or for applications requiring precise control over material flow, such as in industrial processing lines.
Key Characteristics of Calcined Ash Pneumatic Conveying Systems
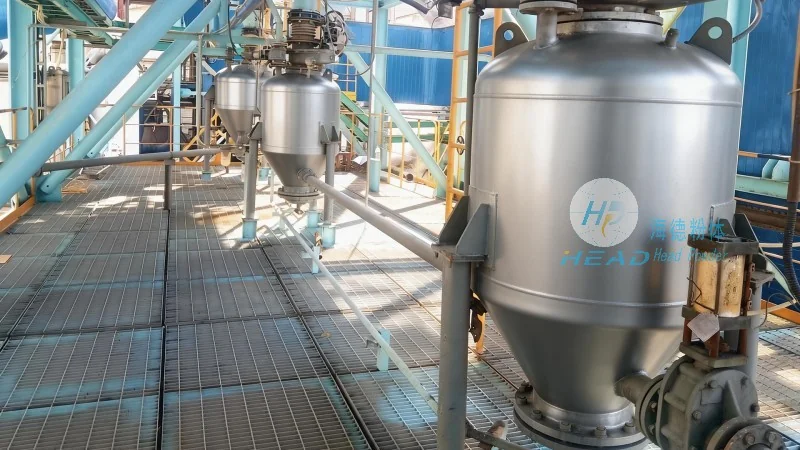
The effectiveness of a pneumatic conveying system for calcined ash is determined by several key characteristics that ensure optimal performance and reliability. First, the system must be capable of handling the specific particle size distribution and moisture content of the calcined ash. Calcined ash particles are often fine and can be abrasive, so the conveying equipment must be constructed from materials that resist wear and corrosion, such as stainless steel or special alloys. Second, the system should maintain low pressure differentials to minimize energy consumption while ensuring sufficient air velocity to prevent particle settling. This balance is crucial for maintaining consistent material flow and preventing blockages in the pipeline. Third, the system must incorporate effective dust control measures, as calcined ash is a fine powder that can create significant dust hazards if not properly contained. This includes features like cyclone separators, filters, and sealed system designs to ensure compliance with environmental regulations and workplace safety standards.
Application Ranges and Use Cases
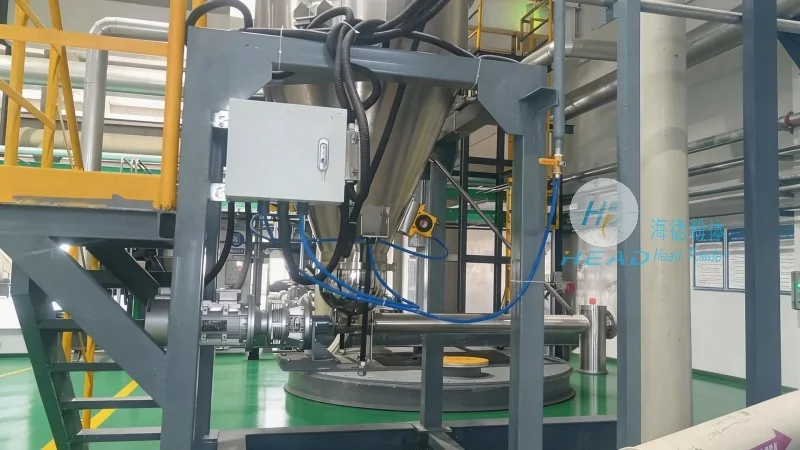
The versatility of calcined ash pneumatic conveying systems makes them suitable for a wide range of applications across various industries. In the power generation sector, these systems are commonly used to transport calcined ash from the boiler to storage silos or for further processing, such as reusing the ash in cement production or as a soil amendment. In the cement and construction industries, calcined ash is often used as a supplementary cementitious material (SCM), and pneumatic conveying systems facilitate its efficient transfer from storage facilities to production lines. Additionally, in the chemical and pharmaceutical industries, calcined ash may be used as a raw material or filler, and the systems ensure its safe and hygienic transport within manufacturing facilities. The systems are also applicable in waste management and environmental remediation projects, where calcined ash is used for land reclamation or as a component in construction materials for remediated sites.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for material handling and processing. With a focus on pneumatic conveying systems tailored for calcined ash and other fine powders, the company leverages advanced technology and industry expertise to deliver high-quality, reliable equipment. Headpowder's commitment to innovation and customer satisfaction is reflected in their comprehensive product line, which includes both standard and customized solutions to meet the unique needs of each client. The company's facilities are located in Shandong, China, where they maintain a strong presence in the industrial equipment market, serving clients both domestically and internationally. By adhering to strict quality standards and providing comprehensive technical support, headpowder ensures that their pneumatic conveying systems not only meet but exceed industry expectations, contributing to the efficient and sustainable handling of calcined ash in various applications.




