Phosphate rock powder material handling systems are essential in the industrial processing of phosphate minerals, serving as the backbone for transporting and managing these fine powders efficiently. These systems are crucial for various applications, including fertilizer production, chemical processing, and mining operations, where the reliable and safe movement of phosphate rock powders is critical to operational success. Understanding the components and design principles of such systems is vital for optimizing performance, ensuring safety, and meeting production demands.
Understanding the Phosphate Rock Powder Material Handling System
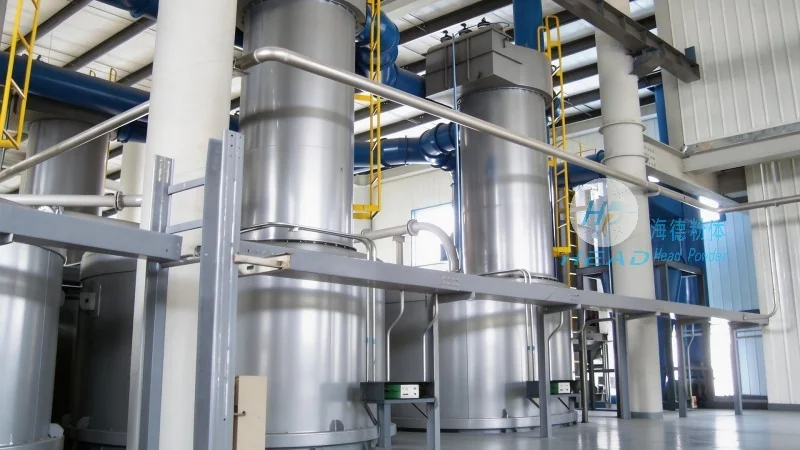
A phosphate rock powder material handling system is a specialized setup designed to transport, store, and process phosphate rock powders from extraction sites to processing facilities. The system typically includes a combination of equipment such as conveyors, feeders, storage silos, and control systems. The primary goal is to handle the fine, abrasive nature of phosphate rock powders while minimizing dust generation, material loss, and operational risks. These systems are engineered to meet the specific requirements of the phosphate industry, which often involves handling large volumes of material with varying moisture content and particle sizes.
Key Design Principles for the System
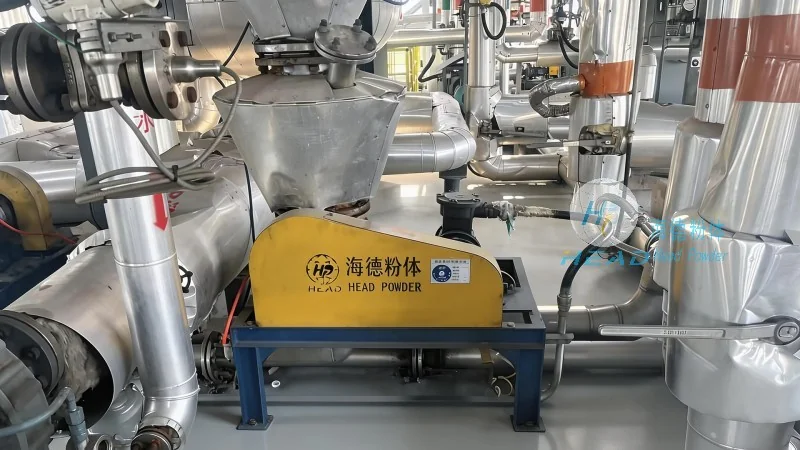
The design of a phosphate rock powder material handling system is guided by several critical principles to ensure efficiency, safety, and durability. First, the system must address the unique properties of phosphate rock powders, which are often fine, dusty, and prone to caking or bridging in storage. This requires specialized equipment like screw conveyors, pneumatic conveyors, or bucket elevators that can handle these characteristics without causing blockages or excessive wear. Second, the design emphasizes dust control and environmental compliance. Advanced filtration systems and enclosed conveyor designs are integrated to minimize airborne dust, protecting both personnel and the environment. Third, the system is built for scalability and adaptability, allowing for future expansions or modifications as production needs evolve. Additionally, the design incorporates robust materials and components to withstand the abrasive nature of phosphate rock, ensuring long-term reliability and low maintenance costs.
Components and Functionality of the System
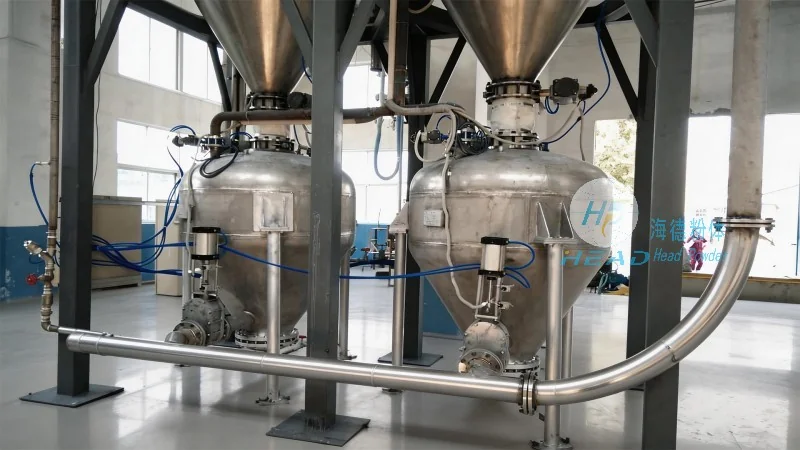
The core components of a phosphate rock powder material handling system include feeders, conveyors, storage silos, and control panels. Feeders, such as rotary or vibratory feeders, regulate the flow of phosphate rock powders from storage to the conveyor system, ensuring consistent and controlled material delivery. Conveyors, often belt or screw types, transport the powders horizontally or vertically, with some systems using pneumatic conveying for long-distance or high-volume transport. Storage silos are used to hold large quantities of phosphate rock powders, providing a buffer for production fluctuations and enabling steady supply to processing units. Control systems, including sensors and automation software, monitor and adjust the system's operations in real-time, optimizing performance and preventing issues like overfilling or underflow. Each component is carefully selected and integrated to work in harmony, ensuring the system operates smoothly and efficiently.
HeadPowder's Expertise in Designing Phosphate Rock Powder Systems
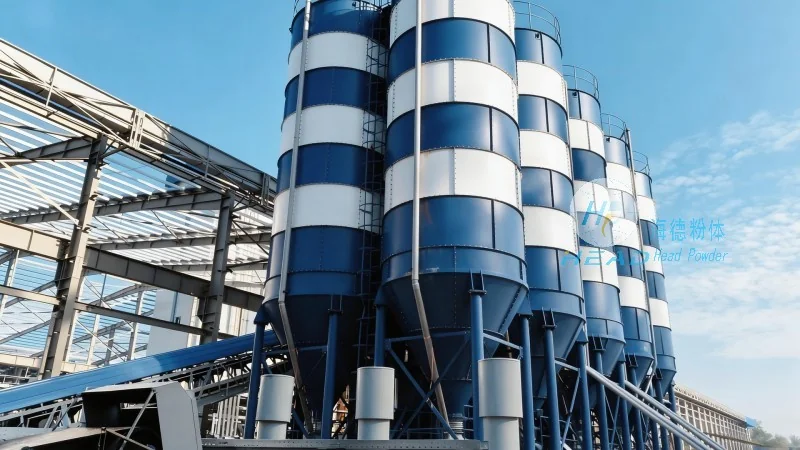
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in designing and manufacturing customized phosphate rock powder material handling systems. With a deep understanding of the unique challenges posed by phosphate rock powders, HeadPowder leverages advanced engineering and material science to develop solutions that meet the specific needs of clients. The company's team of experienced engineers and technicians works closely with clients to assess their operational requirements, site conditions, and production goals, ensuring the final system is tailored to their unique situation. HeadPowder's commitment to quality and innovation is reflected in the robust design and durable construction of their systems, which are built to withstand the harsh conditions of the phosphate industry and deliver long-term performance. The company's facilities in Shandong, China, house state-of-the-art equipment and testing capabilities, allowing for thorough evaluation and optimization of each system before deployment. By focusing on client collaboration and technical excellence, HeadPowder ensures that their phosphate rock powder material handling systems not only meet but exceed industry standards, providing reliable and efficient solutions for the global phosphate market.




