

What is a Mineral Ore Material Handling System Equipment? What Are Its Design Principles?
Understanding the mineral ore material handling system equipment and its design principles is crucial for efficient operation in mining and processing industries. This equipment is specifically engineered to transport and manage mineral ores from extraction sites to processing facilities, ensuring smooth workflow and optimal performance.
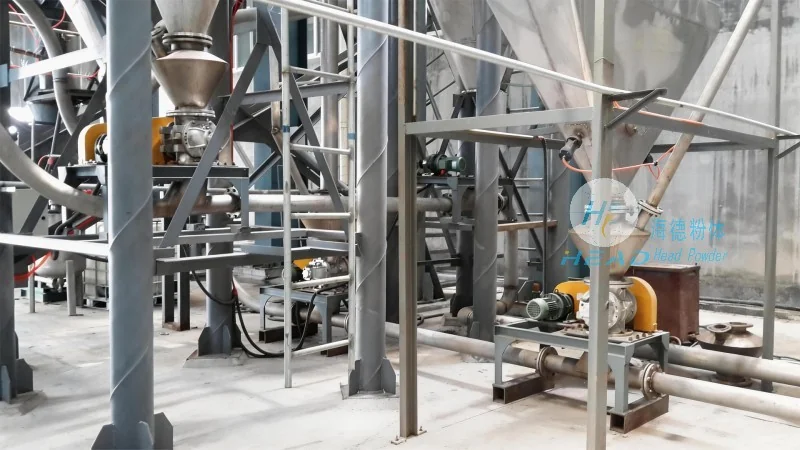
Overview of Mineral Ore Material Handling Systems
Mineral ore material handling systems are complex machinery designed to handle the transportation of bulk mineral ores. These systems typically include components such as conveyors, feeders, elevators, and storage bins. The primary goal is to move large quantities of ore with minimal labor and energy consumption, while maintaining safety and efficiency throughout the process.
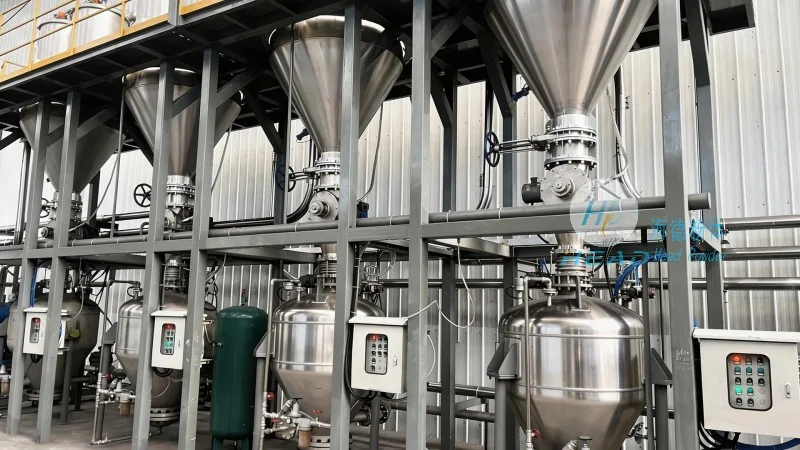
Key Components and Their Functions
The design of a mineral ore material handling system involves several critical components, each playing a vital role in the overall operation. For instance, belt conveyors are commonly used for horizontal and slight incline transport due to their high load capacity and low maintenance requirements. Screw conveyors, on the other hand, are ideal for vertical or inclined transport, especially when dealing with fine or sticky materials. Additionally, bucket elevators are employed for vertical lifting, capable of handling heavy loads with consistent speed.
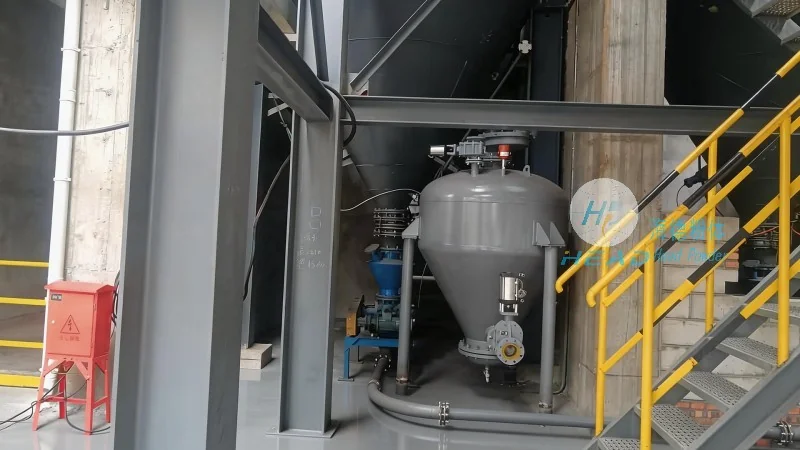
Design Principles for Efficient Operation
The design principles of mineral ore material handling systems focus on several key factors to ensure optimal performance. First, the system must be capable of handling the specific characteristics of the mineral ore, such as size, density, and moisture content. This involves selecting appropriate conveyor types and materials to prevent wear and tear. Second, the system should be designed for high throughput and reliability, minimizing downtime and maintenance intervals. Third, safety is a paramount consideration, with features like emergency stop mechanisms and protective guards integrated into the design. Finally, the system must be cost-effective, balancing initial investment with long-term operational costs.
Application in Mining and Processing
Mineral ore material handling systems are widely used in various stages of mining and processing. From the extraction of raw ore from mines to its transportation to processing plants, these systems play a central role. In open-pit mining, for example, large-scale conveyor systems are used to transport ore from the excavation site to processing facilities, reducing the need for heavy machinery and manual labor. In underground mining, bucket elevators and vertical conveyors are used to move ore from deep levels to the surface, ensuring a continuous supply of material for processing.
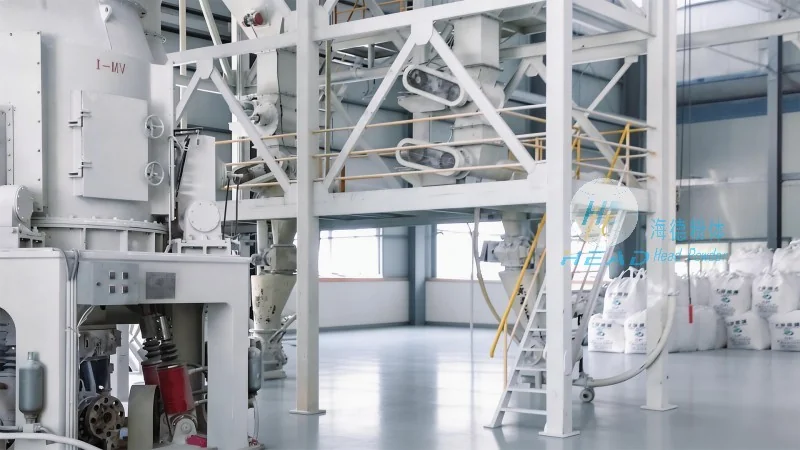
Engineering and Manufacturing by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of mineral ore material handling systems. With a strong focus on engineering excellence and customer satisfaction, the company has developed a range of high-quality equipment tailored to meet the diverse needs of the mining industry. The company's products are designed based on robust engineering principles, ensuring durability, efficiency, and safety. By leveraging advanced manufacturing techniques and rigorous quality control processes, Shandong HeadPowder Engineering Co., Ltd. delivers systems that enhance operational performance and reduce costs for its clients.