HeadPowder, a leading engineering company based in Shandong, China, specializes in providing advanced material handling solutions. The company’s expertise lies in designing and manufacturing efficient systems for industrial applications, particularly those requiring dust control and seamless material transfer. This article explores the working principle and key features of the tonne bag dust-free loading station material handling system, a critical piece of equipment for industries dealing with bulk materials.
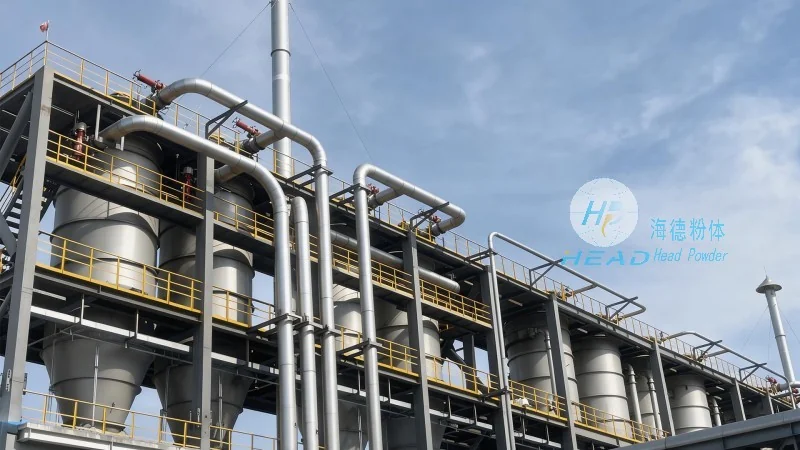
Overview of the Tonne Bag Dust-Free Loading Station
The tonne bag dust-free loading station is a specialized system engineered to handle bulk materials from tonne bags while maintaining a clean, dust-free environment. It integrates multiple components, including a hopper, conveyor system, dust extraction unit, and control panel, to ensure safe and efficient material transfer. This system is particularly valuable in industries such as chemicals, food processing, and pharmaceuticals, where contamination and dust exposure are major concerns.
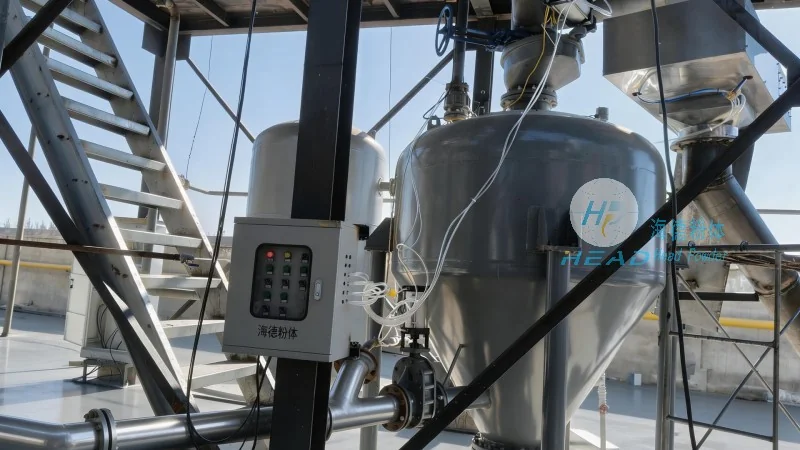
Working Principle of the Material Handling System
The operation of the tonne bag dust-free loading station begins with the placement of a tonne bag onto the hopper. The system then uses a combination of mechanical and pneumatic mechanisms to open the bag and release the material into the hopper. Once the material is inside, a conveyor system transports it to the next processing stage. Simultaneously, a dust extraction system actively removes airborne particles, preventing contamination and ensuring a safe working environment. The control panel allows operators to monitor and adjust the system parameters, such as conveyor speed and dust extraction intensity, to optimize performance.
Key Features and Advantages
The tonne bag dust-free loading station material handling system offers several notable features that enhance its functionality and efficiency. First, its automated operation reduces the need for manual handling, minimizing the risk of human error and improving safety. The integrated dust extraction system effectively captures and filters dust, maintaining a clean workspace and complying with environmental regulations. Additionally, the system’s modular design allows for easy integration with existing production lines, making it a versatile solution for various industrial settings. Another key advantage is its high throughput capacity, which enables rapid material transfer, thereby increasing overall productivity. The system also incorporates advanced sensors and controls to ensure consistent performance and minimize downtime.
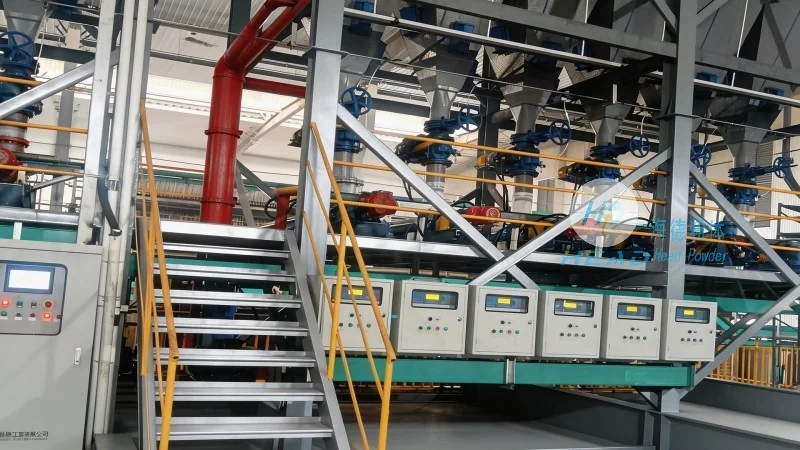
Application and Industry Impact
HeadPowder’s tonne bag dust-free loading station is widely used in industries where bulk material handling is essential. In the chemical industry, for example, it helps in transferring raw materials without compromising product quality or safety. In food processing, the system ensures that materials are handled hygienically, preventing contamination and meeting stringent food safety standards. The pharmaceutical industry also benefits from this system, as it maintains a sterile environment, critical for producing high-quality medications. By providing a reliable and efficient material handling solution, HeadPowder contributes to the operational efficiency and safety of its clients.




