Working Principle and Features of Dry Cobblestone Powder Pneumatic Conveying Equipment
Release time:2026-09-18 03:01:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for dry cobblestone powder. These systems are engineered to efficiently transport dry cobblestone powders over varying distances with minimal loss and optimal performance. The following content provides a detailed exploration of the working principle and key features of such equipment, highlighting its technical advantages and practical applications.
Working Principle of Dry Cobblestone Powder Pneumatic Conveying Equipment
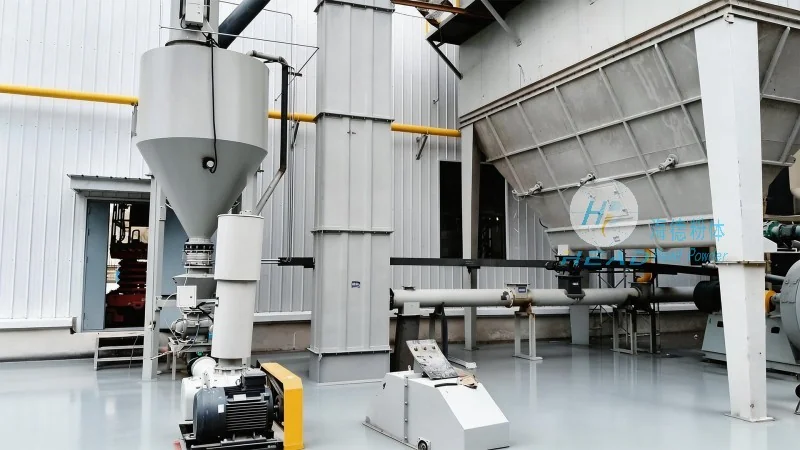
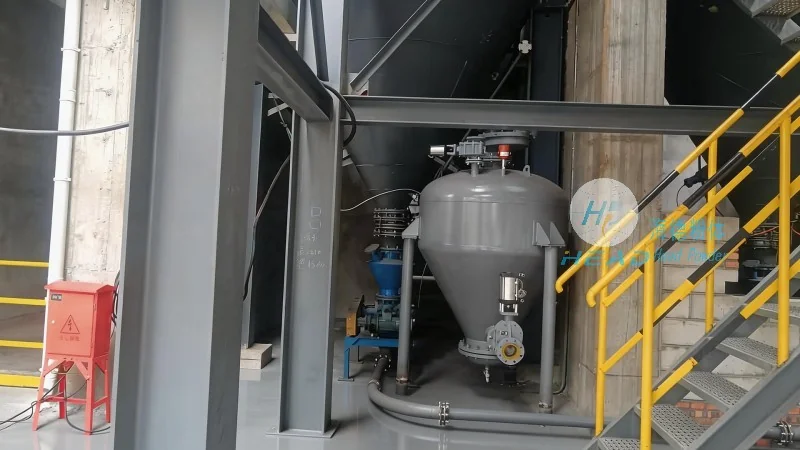
The core working principle of dry cobblestone powder pneumatic conveying equipment revolves around the use of compressed air to transport dry powders through a sealed pipeline system. In a typical setup, the system operates by first feeding the dry cobblestone powder into a hopper or feeder. The feeder then controls the flow rate of the powder into the conveying line, ensuring a consistent and controlled input of material. Simultaneously, a high-pressure blower or compressor generates a continuous air stream that propels the powder particles through the pipeline. The air and powder mixture travels through the pipeline to a separation unit, where the powder is separated from the air using centrifugal force or filtration. The separated powder is then collected in a receiving hopper, while the air is either filtered and recycled back into the system or released after being cleaned of dust particles. This closed-loop operation minimizes air consumption and reduces operational costs, making the system energy-efficient. The entire process is automated, with sensors monitoring the flow rates and pressure levels to maintain optimal performance and prevent system failures.
Key Features of Dry Cobblestone Powder Pneumatic Conveying Equipment
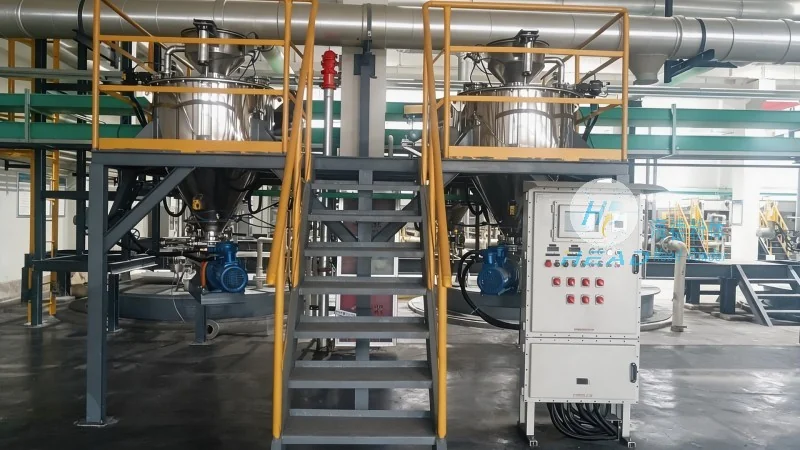
Dry cobblestone powder pneumatic conveying equipment from HeadPowder is characterized by several notable features that enhance its performance and usability. Firstly, the system offers high efficiency in material transport, capable of moving dry cobblestone powders over long distances with minimal energy consumption. The sealed pipeline design prevents dust leakage and contamination, ensuring compliance with environmental regulations and maintaining product purity. Secondly, the equipment is designed for low maintenance, with components such as the feeder and blower built to withstand the abrasive nature of dry cobblestone powders, reducing downtime and operational costs. The use of wear-resistant materials in the construction of the conveying lines and separation units further enhances durability. Additionally, the system provides flexibility in operation, supporting both pressure and suction modes depending on the application requirements, allowing for versatile use in different industrial settings. The modular design of the equipment allows for easy integration into existing production lines, enabling manufacturers to upgrade their material handling processes without major overhauls. The system also includes safety features such as pressure relief valves and overcurrent protection to ensure safe operation in industrial environments.
Technical Advantages and Application Scenarios
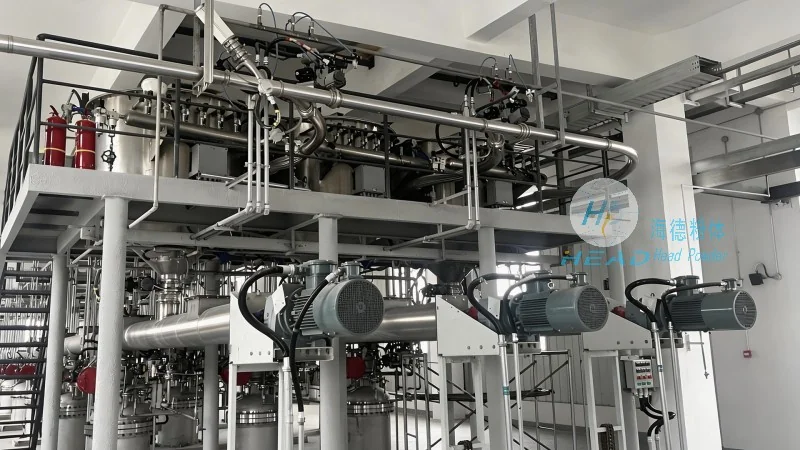
HeadPowder's dry cobblestone powder pneumatic conveying equipment leverages several technical advantages that make it suitable for a wide range of applications. The system's ability to handle abrasive materials like dry cobblestone powders without significant wear or degradation is a key advantage, as these materials can otherwise damage traditional conveyor systems. The sealed and dust-free operation contributes to a cleaner working environment, which is particularly beneficial in industries where dust control is critical, such as construction and mining. Furthermore, the equipment's modular design allows for easy integration into existing production lines, enabling manufacturers to upgrade their material handling processes without major overhauls. In practical applications, this equipment is commonly used in the production of building materials, where dry cobblestone powders are a key ingredient in concrete and mortar mixes. It is also utilized in mining operations for transporting crushed stone and powder from processing facilities to storage or processing areas. The consistent and reliable performance of the system ensures that production processes remain uninterrupted, supporting high productivity and quality standards. Additionally, the system's energy efficiency and low maintenance requirements make it a cost-effective solution for long-term material handling needs, providing a competitive edge to businesses in the construction and mining sectors.




