Working Principle and Features of Barley Malt Powder Pneumatic Conveying Line
Release time:2026-09-18 05:01:27
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
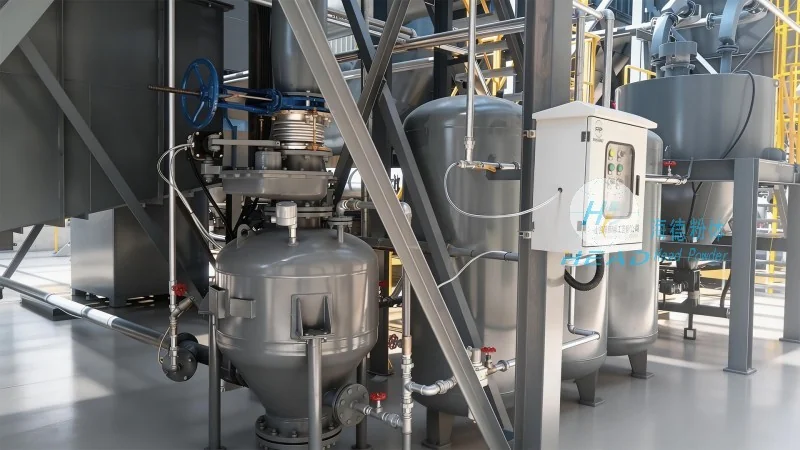
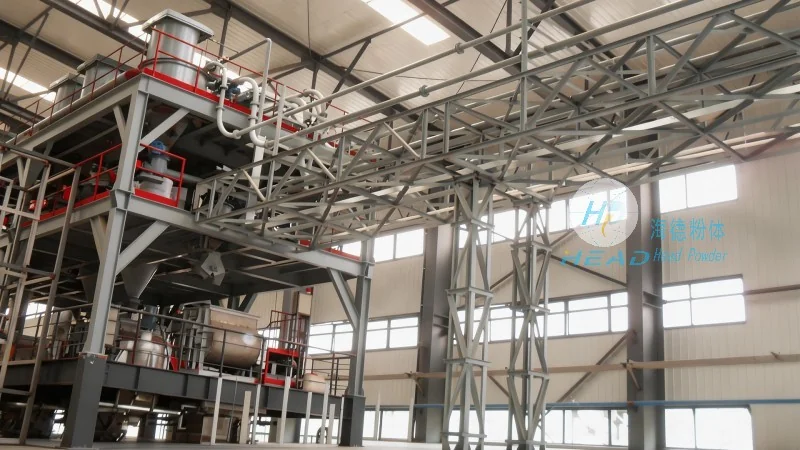
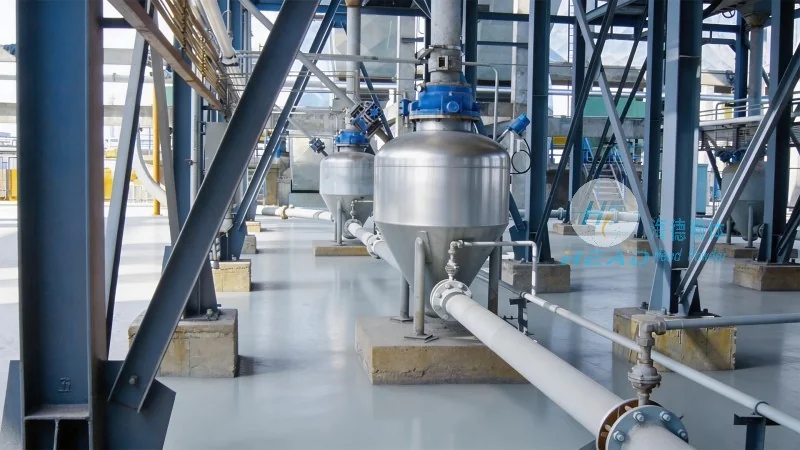
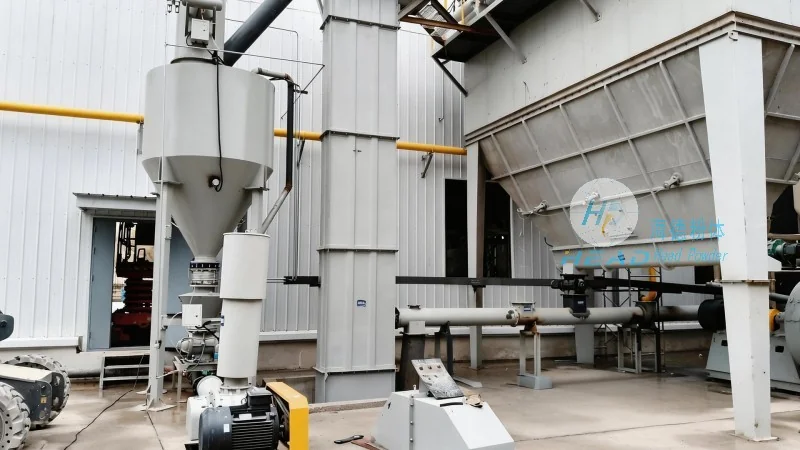
The working principle of a barley malt powder pneumatic conveying line is centered on the utilization of compressed air to transport dry powder materials, in this case, barley malt powder. The system operates by drawing the powder from a storage hopper into a pipeline where it is mixed with high-velocity air. The blower or compressor, which is the heart of the system, generates the necessary pressure to move the powder through the network of pipes. As the air flows through the pipeline, it entrains the powder particles, creating a slurry of air and powder that travels to the destination point. The design of the system is critical to ensure that the powder is conveyed without degradation or clogging. The velocity of the air is carefully controlled to maintain the powder in a suspended state, preventing it from settling or sticking to the pipe walls. This process is efficient and can handle large volumes of powder, making it an ideal solution for breweries that require consistent and reliable transport of malt ingredients.
Key Features of Barley Malt Powder Pneumatic Conveying Line
Shandong HeadPowder Engineering Co., Ltd. develops advanced pneumatic conveying systems that incorporate several key features tailored for the unique properties of barley malt powder. One of the primary features is the flexibility in system design, which allows for both positive pressure and negative pressure configurations. Positive pressure systems use a blower to push air and powder through the pipeline, while negative pressure systems use a vacuum to draw the material. This flexibility enables the system to be adapted to various production layouts and operational requirements. The equipment is constructed from high-quality materials, such as stainless steel and food-grade plastics, which are resistant to corrosion and ensure compliance with food safety standards. The system also includes advanced control systems, such as variable frequency drives (VFDs) and pressure sensors, that allow for precise regulation of air flow and pressure. These controls help optimize energy consumption and prevent overloading of the system, leading to cost savings and increased efficiency. Additionally, the conveying line is equipped with dust collection and filtration systems to maintain a clean and safe working environment, which is essential in food processing applications. The company's engineering expertise ensures that each system is customized to handle the specific characteristics of barley malt powder, such as its moisture content and particle size distribution, resulting in a reliable and efficient transport solution.
Benefits of Implementing a Professional Pneumatic Conveying System
Adopting a professional pneumatic conveying system for barley malt powder offers significant advantages for breweries and malt processing facilities. The most notable benefit is the improvement in operational efficiency, as the system enables continuous and automated transport of powder, reducing the need for manual handling and labor. This not only saves time but also minimizes the risk of product contamination and human error. The system also enhances product quality by minimizing exposure to air and moisture, which can affect the flavor and nutritional value of the barley malt. The compact design of the conveying line saves valuable floor space in production facilities, making it suitable for both new installations and retrofitting into existing breweries. The reliability of the system, with minimal downtime due to maintenance, ensures consistent production output and reduces the risk of bottlenecks in the manufacturing process. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive support services, including installation, commissioning, and maintenance, to ensure that clients receive a fully operational and reliable system. The company's commitment to quality and customer satisfaction ensures that each client receives a solution that meets their specific needs and contributes to their overall operational success.




