For industrial applications involving the handling of brown sugar, efficient and reliable material transport is crucial. The pneumatic conveying system, specifically designed for brown sugar material, offers a sophisticated solution that addresses the unique challenges of transporting this type of bulk material. This article explores the working principle and key features of such a system, highlighting its benefits and operational advantages.
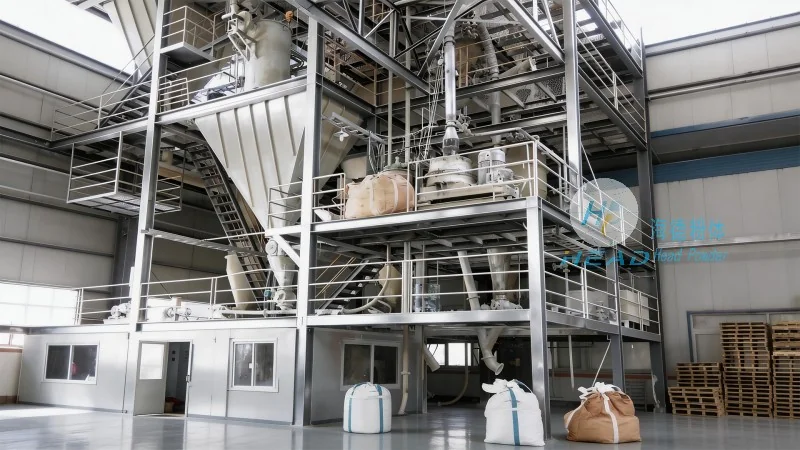
Introduction to Brown Sugar Material Pneumatic Conveying System
The system is engineered by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field of material handling solutions. With headquarters located in Shandong, China, the company specializes in developing advanced pneumatic conveying technologies tailored to various industrial needs. The brown sugar material pneumatic conveying system is a testament to their expertise in creating systems that enhance productivity while maintaining the quality of the material being transported.
Working Principle of the Pneumatic Conveying System
The core mechanism of the brown sugar material pneumatic conveying system relies on the principles of air flow and pressure differentials. The system operates by generating a flow of air within a pipeline network. As air is introduced into the system, it creates a pressure difference that propels the brown sugar particles through the conveying line. This process involves several key components, including a blower or air compressor, which supplies the necessary air pressure, and a series of pipes, valves, and inlets/outlets that guide the material from the source to the destination.
During operation, the brown sugar is introduced into the system at the inlet point, often through a hopper or feeder. The air flow then lifts and transports the material particles along the pipeline. The system can be configured as either a positive pressure or negative pressure system, depending on the specific requirements of the application. Positive pressure systems use compressed air to push the material forward, while negative pressure systems use suction to draw the material through the line. For brown sugar, a positive pressure system is commonly preferred due to its ability to handle the material's density and moisture content effectively.
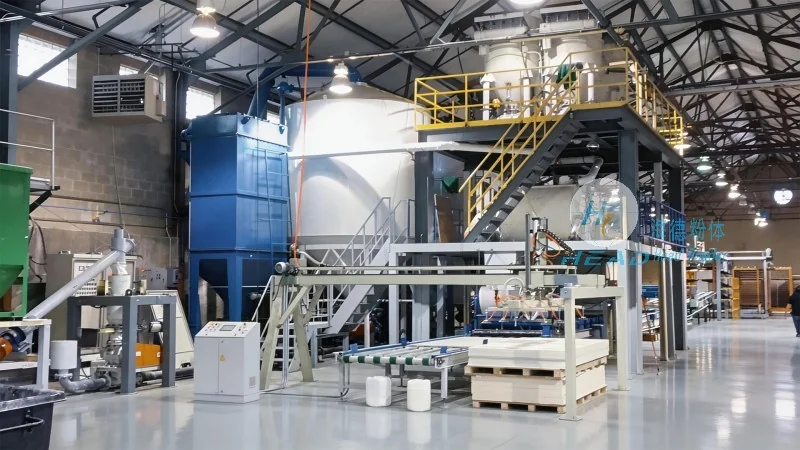
Key Features and Advantages of the System
The brown sugar material pneumatic conveying system offers several distinct features that make it an ideal choice for industrial operations. One of the primary advantages is its high efficiency in material transport. By using air as the conveying medium, the system minimizes the need for mechanical components like belts or buckets, reducing maintenance requirements and operational downtime. This results in a more reliable and cost-effective solution for moving large volumes of brown sugar.
Another significant feature is the system's ability to maintain the quality of the brown sugar. Unlike traditional mechanical conveying methods that may cause abrasion or contamination, the pneumatic system ensures that the material remains clean and free from foreign particles. This is particularly important for brown sugar, which is often used in food and beverage applications where product purity is paramount. The system also helps in controlling dust and preventing cross-contamination, contributing to a safer working environment.
The system's flexibility is another notable feature. It can be easily integrated into existing production lines and adapted to various layouts and distances. Whether the transport distance is short or long, the system can be scaled to meet the specific needs of the facility. Additionally, the system allows for multiple discharge points, enabling the distribution of brown sugar to different storage or processing areas without the need for additional equipment.
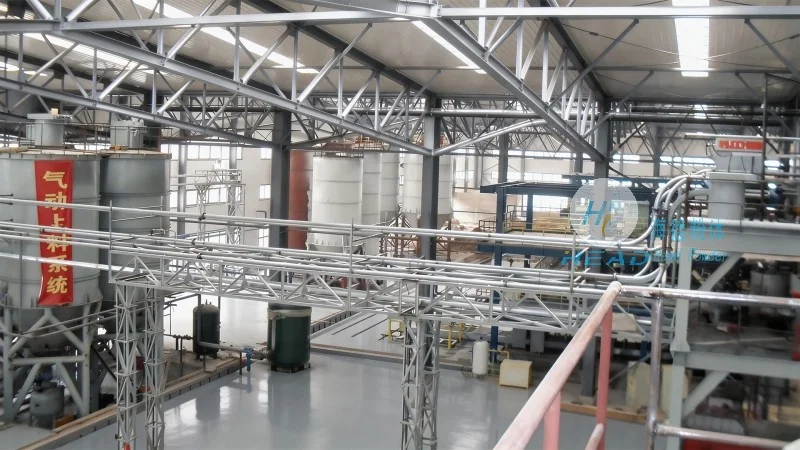
Operational Benefits and Application Scope
Implementing the brown sugar material pneumatic conveying system provides numerous operational benefits. The system enhances overall productivity by streamlining the material handling process, reducing the time and labor required for manual transport. It also improves safety in the workplace by eliminating the need for manual handling of bulk materials, which can be hazardous. Furthermore, the system's energy efficiency contributes to lower operational costs, making it a sustainable choice for industrial operations.
The application scope of this system is broad, covering various industries that handle brown sugar, such as food processing, pharmaceuticals, and chemical manufacturing. Whether used for transporting raw brown sugar from storage to processing units or for moving finished products to packaging lines, the system ensures consistent and reliable material flow. The adaptability of the system allows it to be customized for different production scales, from small-scale operations to large industrial facilities.
Conclusion
In conclusion, the brown sugar material pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and efficient solution for the transport of brown sugar. Its working principle, based on air flow and pressure differentials, combined with its key features such as high efficiency, material quality preservation, and operational flexibility, makes it a superior choice for industrial applications. By leveraging this technology, companies can enhance their productivity, maintain product quality, and ensure a safe and sustainable material handling process.




