This article introduces the fundamental principles and operational characteristics of stone aggregate powder conveying lines. Such systems are essential in industries that handle bulk materials, particularly in construction and mining sectors. The focus is on how these lines function and where they are most effectively applied.
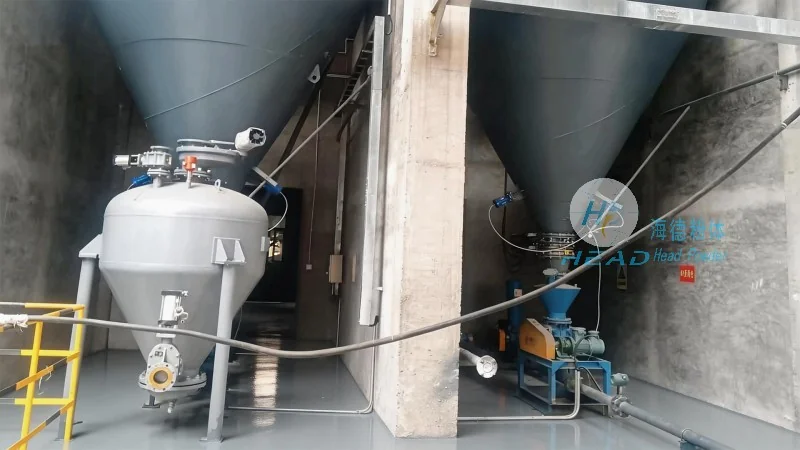
Core Principles of the Conveying System
The principle of a stone aggregate powder conveying line revolves around the efficient transport of loose, granular materials from a source to a destination. This is typically achieved through a combination of mechanical components like screw conveyors, pneumatic systems, or belt conveyors. The system ensures minimal material loss, consistent flow rates, and the ability to handle various particle sizes and moisture contents. The design is tailored to maintain material integrity and prevent clogging, which is crucial for maintaining operational efficiency.
Key Working Scene Characteristics
The working scene characteristics of stone aggregate powder conveying lines vary based on the specific application. For instance, in construction sites, these lines are often used to transport sand, gravel, and other aggregates from storage areas to mixing stations or construction zones. The key characteristics here include high capacity, flexibility in layout, and the ability to operate in diverse environmental conditions. In industrial settings, such as cement plants or mining operations, the lines may handle larger volumes of material over longer distances, requiring robust infrastructure and advanced control systems.
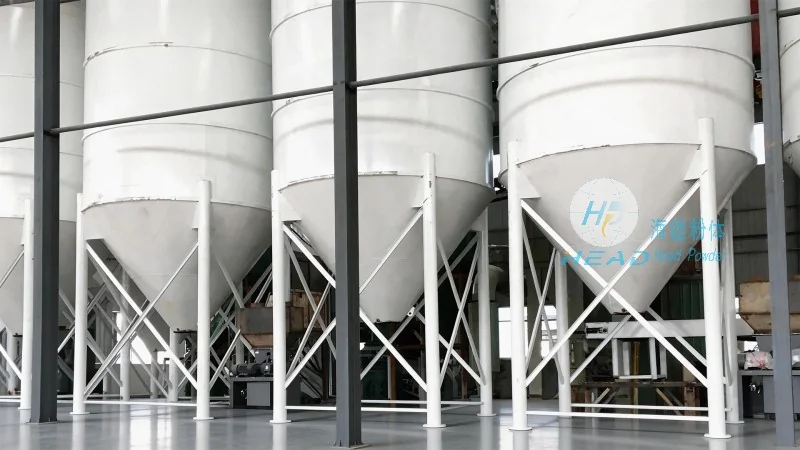
Application in Construction and Industrial Projects
In construction projects, stone aggregate powder conveying lines play a vital role in streamlining material handling processes. They reduce the need for manual labor and minimize the risk of material contamination or spillage. The systems are designed to integrate seamlessly with existing construction workflows, enhancing overall project efficiency. In industrial applications, like the production of concrete or other building materials, these lines ensure a steady supply of raw aggregates, which is critical for maintaining production schedules and quality standards.
Technical Advantages and Efficiency
The technical advantages of modern stone aggregate powder conveying lines include high throughput rates, energy efficiency, and low maintenance requirements. Advanced control systems allow for real-time monitoring and adjustment of the conveying process, optimizing performance based on material characteristics and operational needs. The use of durable materials and components ensures long-term reliability, reducing downtime and operational costs. Additionally, the systems are designed to be scalable, allowing businesses to expand their operations without significant changes to the conveying infrastructure.
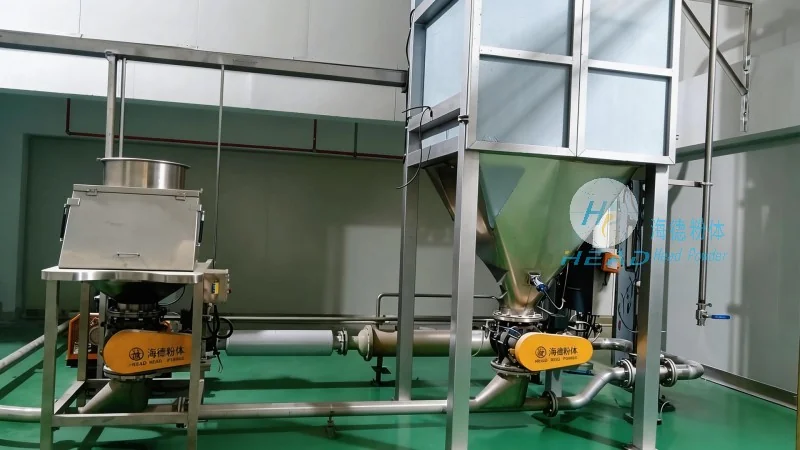
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of these advanced conveying systems, is a leading company in the field of bulk material handling solutions. With a strong presence in China, particularly in Shandong province, the company specializes in designing, manufacturing, and installing high-quality stone aggregate powder conveying lines. The company's commitment to innovation and customer satisfaction has earned it a reputation for delivering reliable and efficient solutions tailored to the unique needs of each project.
Location and Service Area
HeadPowder Engineering is headquartered in Shandong, China, a region known for its robust industrial and construction sectors. The company serves clients across China and beyond, providing comprehensive support from initial consultation and system design to installation and after-sales service. The local presence ensures quick response times and personalized service, which is essential for maintaining strong client relationships and ensuring project success.




