HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced sugar powder conveying systems. These systems are engineered to efficiently handle the transportation of granular or powdered sugar, ensuring optimal performance in various industrial applications. This article provides a detailed overview of the operational process and working principles of such equipment, highlighting the key components and mechanisms involved.
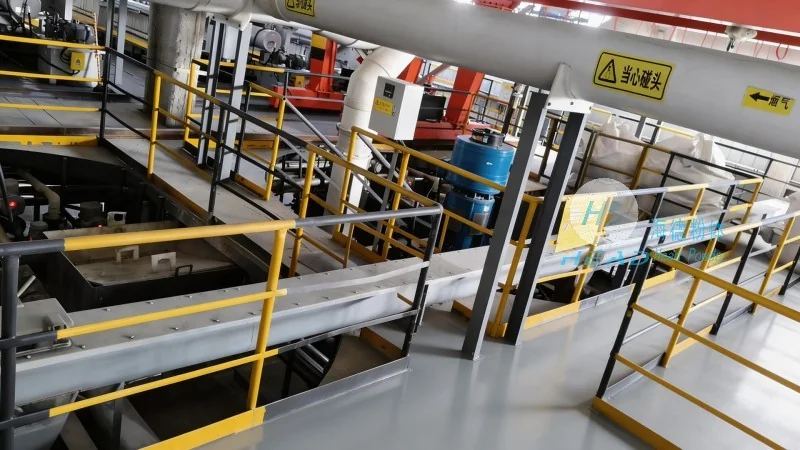
Overview of the Sugar Powder Conveying System
The sugar powder conveying system typically consists of several core components, including a hopper for material storage, a conveyor mechanism (such as a screw conveyor or pneumatic system), and control systems for monitoring and regulating the flow. The system is designed to maintain consistent material flow rates, minimize product degradation, and ensure safe operation in industrial settings. Each component works in tandem to achieve efficient and reliable sugar powder transportation.
Key Components and Their Functions
1. Hopper: The hopper serves as the primary storage container for the sugar powder. It is equipped with a discharge valve or gate to control the flow of material into the conveyor system. The design of the hopper, often with a conical or rectangular shape, helps in preventing material bridging and ensuring smooth material release.
2. Conveyor Mechanism: The conveyor is the heart of the system, responsible for moving the sugar powder from the hopper to the desired destination. In many applications, a screw conveyor is used due to its ability to handle dry, free-flowing powders without the need for additional air or pressure. The screw conveyor consists of a rotating helical screw inside a cylindrical tube, which pulls the material forward through the system.
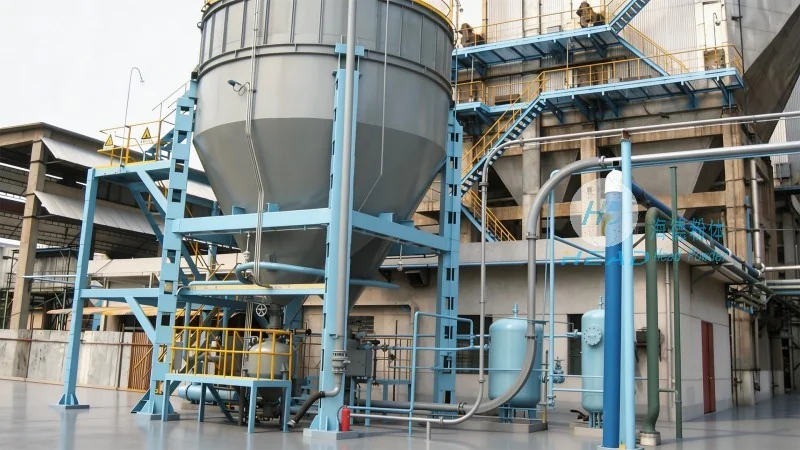
3. Pneumatic Conveying Option: For applications requiring longer distances or more complex routing, a pneumatic conveying system may be employed. This system uses compressed air to transport the sugar powder through a pipeline. The material is carried in a stream of air, allowing for flexible and efficient movement across different locations.
4. Control System: Modern sugar powder conveying systems are equipped with advanced control systems that monitor parameters such as flow rate, pressure, and temperature. These systems use sensors and automation technology to adjust the operation in real-time, ensuring optimal performance and preventing issues like clogging or overloading.
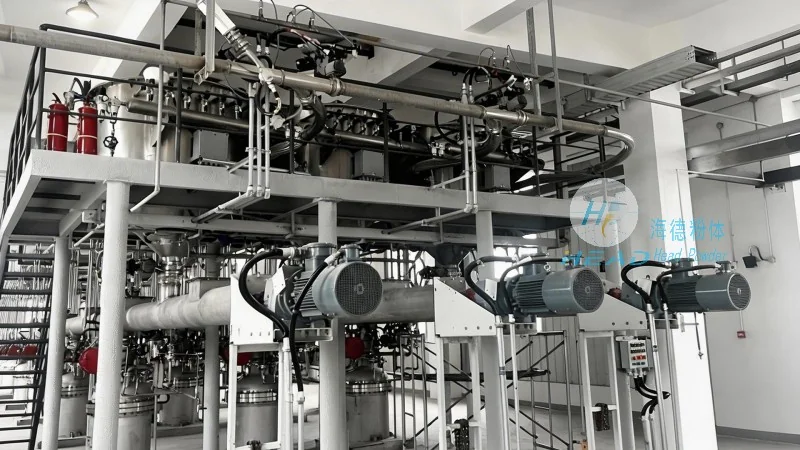
Operation Process of the Sugar Powder Conveying System
The operation process of the sugar powder conveying system begins with the loading of sugar powder into the hopper. The material is then released from the hopper into the conveyor mechanism under controlled conditions. In a screw conveyor system, the rotating screw pushes the powder forward, while in a pneumatic system, the compressed air propels the material through the pipeline. The material is transported to the discharge point, where it is collected and used in subsequent processes. Throughout the operation, the control system continuously monitors the system's performance and adjusts parameters as needed to maintain consistent and efficient material flow.
Working Principle of the Sugar Powder Conveying System
The working principle of the sugar powder conveying system is based on the physical properties of the material and the mechanical or pneumatic forces applied to it. For screw conveyors, the principle involves the use of a rotating screw to create a pushing force that moves the powder along the conveyor path. The design of the screw, including its pitch and diameter, is optimized to handle the specific characteristics of sugar powder, such as its density and flowability. In pneumatic systems, the principle relies on the Bernoulli effect, where the high-velocity air stream creates a low-pressure area that draws the powder into the pipeline and transports it to the destination.
Both mechanisms ensure that the sugar powder is conveyed without degradation, maintaining its quality and consistency. The control system plays a crucial role in maintaining the stability of the process, preventing issues like clogging or uneven flow. By integrating these components and principles, the sugar powder conveying system from HeadPowder provides reliable and efficient transportation of sugar powder in industrial settings.




