Grain silo pneumatic conveying systems represent a critical technology in modern agricultural and food processing operations. These systems are engineered to efficiently transport bulk grains, seeds, and similar materials within storage silos or between different storage and processing facilities. By utilizing compressed air as the primary transport medium, the system ensures a dust-free, hygienic, and low-maintenance method of material handling. The equipment is designed to maintain the quality and integrity of the conveyed products, making it an indispensable component in grain storage and handling infrastructure.
Key Components and Their Functional Roles
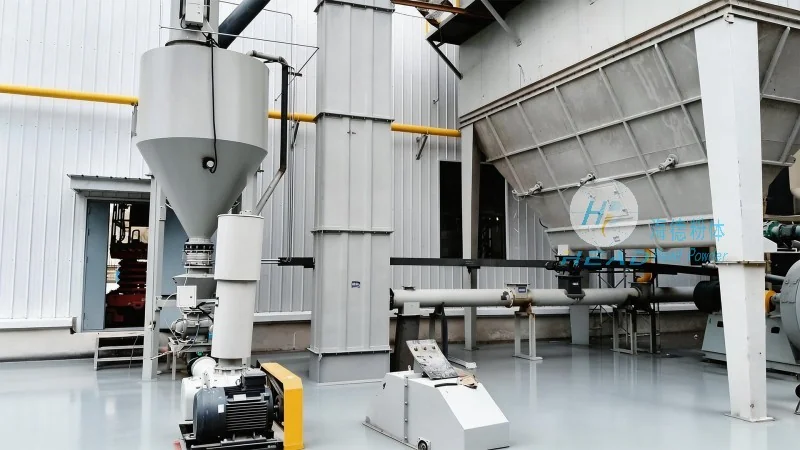
The pneumatic conveying system for grain silos comprises several interrelated components, each playing a vital role in the overall operation. The primary components include the material hopper, airlock valve, conveying pipeline, and material receiver. The hopper is the initial point of material intake, where bulk grains are loaded and stored before being conveyed. It is typically equipped with a discharge gate or valve to control the flow of material into the system. The airlock, often a rotary or sliding type, acts as a critical control device. Its function is to regulate the flow of material into the conveying line, preventing backflow and maintaining consistent air pressure within the system. This component ensures that material is transferred in a controlled manner without causing pressure fluctuations that could disrupt the conveying process. The conveying line, usually constructed from metal or flexible tubing, is the pathway through which the material and air travel. It is designed to withstand the abrasive nature of grains and the pressure of compressed air. The line's diameter and length are carefully selected to optimize air velocity and material transport efficiency. The receiver is the final destination for the conveyed material, where it is deposited for further processing or storage. It is equipped with a discharge valve to control the release of material from the system.
Structural Principles and Operational Mechanics
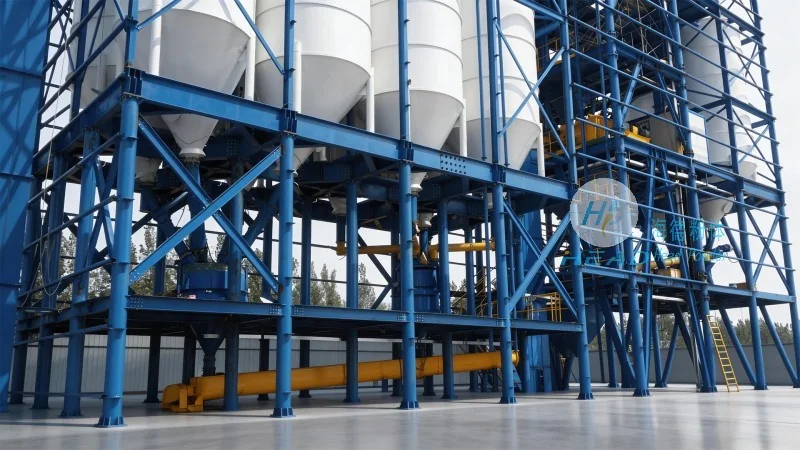
The structural design of the grain silo pneumatic conveying system is based on fundamental principles of fluid dynamics and material transport. The system operates by creating a pressure differential between the hopper and the receiver. Compressed air is introduced into the conveying line, generating a flow that lifts and propels the grains. The air velocity within the line is a critical parameter, as it must be sufficient to overcome the gravitational force of the material and maintain a stable flow. The system's design ensures that the air velocity remains within an optimal range to prevent material degradation, such as breakage or excessive dust generation. The use of appropriate materials for the conveying line and components is essential to withstand the abrasive and corrosive properties of grains. For instance, stainless steel or high-grade metal alloys are commonly used for the pipeline to ensure durability and resistance to wear. The system's control mechanisms, including pressure sensors and flow meters, monitor and regulate the air pressure and material flow, ensuring consistent and reliable operation. The structural integrity of the components is also a key consideration, as they must withstand the forces exerted by the material and air during operation.
Advantages and Benefits for Grain Storage Operations
Adopting a pneumatic conveying system in grain silo operations offers numerous advantages that enhance operational efficiency and product quality. One of the most significant benefits is the elimination of dust and contamination, which is crucial for maintaining the hygienic standards required in food processing and agricultural storage. The system provides a closed-loop operation, preventing the release of dust into the environment and reducing the risk of material loss or degradation. This feature is particularly important for handling sensitive grains, such as wheat or rice, where dust can affect their quality and market value. Another advantage is the automation of material handling, which reduces labor costs and minimizes the risk of human error. The system allows for continuous and uninterrupted material transfer, enabling round-the-clock operation without the need for manual intervention. This automation also improves safety in the workplace by reducing the need for workers to handle heavy or bulky materials manually. The compact design of the pneumatic conveying system allows for installation in confined spaces within the silo, optimizing the use of available storage area. This is especially beneficial in facilities with limited space or where space efficiency is a priority. Additionally, the low maintenance requirements of the system contribute to long-term cost savings. The components are designed for durability and reliability, with minimal moving parts that require regular maintenance. This reduces downtime and ensures consistent performance over the system's service life.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
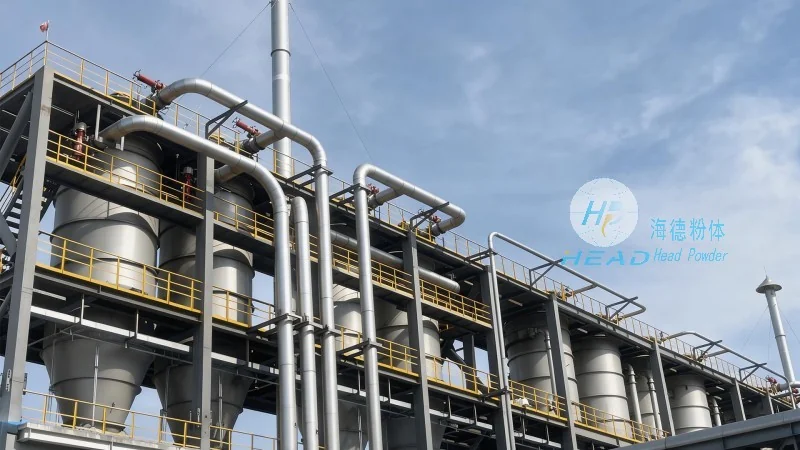
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a prominent manufacturer specializing in grain handling and processing equipment. The company has established itself as a leader in the industry, providing high-quality pneumatic conveying systems and other grain storage solutions. HeadPowder's commitment to innovation and customer satisfaction drives its product development and manufacturing processes. The company leverages advanced engineering and manufacturing technologies to design and produce equipment that meets the evolving needs of the agricultural sector. With a focus on reliability, efficiency, and durability, HeadPowder's products are widely used in grain silos, feed mills, and food processing plants across China and internationally. The company's headquarters and manufacturing facilities are located in Shandong, China, where it employs a team of experienced engineers and technicians dedicated to research, development, and quality control. HeadPowder adheres to international standards and certifications, ensuring that its products are compliant with regulatory requirements and industry best practices. The company's customer-centric approach and technical expertise have earned it a reputation for delivering reliable and effective grain handling solutions that enhance operational performance and product quality.




