Organic fertilizer powder conveying systems are critical components in the agricultural and fertilizer processing industries, designed to efficiently transport bulk organic materials such as compost, manure, and other organic waste. These systems play a vital role in optimizing the handling and distribution of organic fertilizers, ensuring consistent and reliable material flow from production to application. Understanding the structural design and operational principles of these systems is essential for selecting the most suitable equipment for specific applications, enhancing productivity, and maintaining product quality.
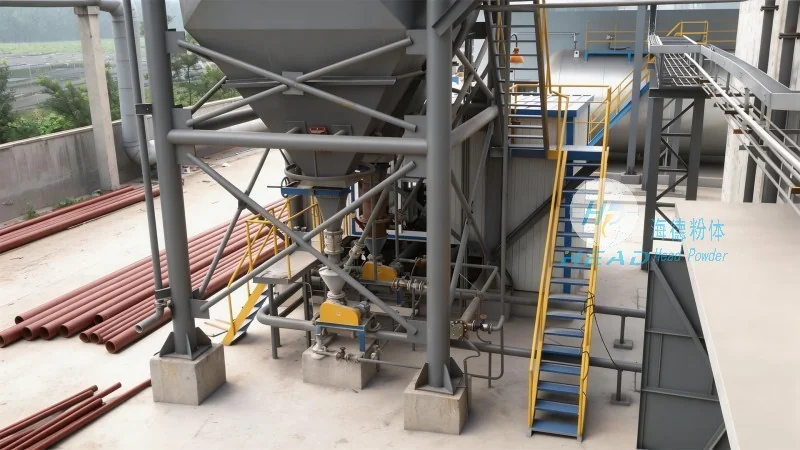
Key Structural Components of Powder Conveying Systems
The core structure of an organic fertilizer powder conveying system typically includes several key components that work in tandem to achieve efficient material transport. The primary components include the hopper or feed bin, which stores and feeds the organic fertilizer powder into the conveying system. This is often followed by a feeding mechanism, such as a rotary valve or screw feeder, that regulates the flow of material into the conveyor. The conveyor itself, which may be a pneumatic system (air-swept) or a mechanical system (e.g., belt or screw conveyor), is responsible for moving the powder through the system. Additionally, the system may include a dust collection or filtration unit to control airborne particles and ensure environmental compliance. Control panels and sensors are also integral, providing real-time monitoring and adjustment of the conveying process to maintain optimal performance.
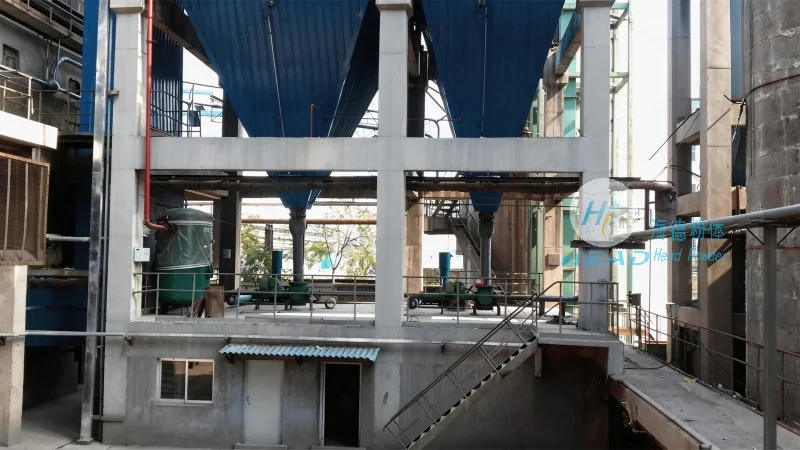
Working Principles of Organic Fertilizer Powder Conveying
The operational principle of organic fertilizer powder conveying systems varies based on the type of conveyor used. Pneumatic conveying systems, for example, utilize compressed air to create a flow of air and material through a pipeline. The organic fertilizer powder is suspended in the air stream and transported to the destination. This method is particularly effective for handling fine powders and can achieve long-distance transport with minimal material degradation. Mechanical conveyors, on the other hand, rely on mechanical forces such as gravity, screw rotation, or belt movement to move the powder. Screw conveyors, for instance, use a rotating screw to push the material forward, while belt conveyors use a moving belt to transport the powder in a horizontal or inclined path. Each system has its advantages and is selected based on factors like material characteristics, distance, and system layout.
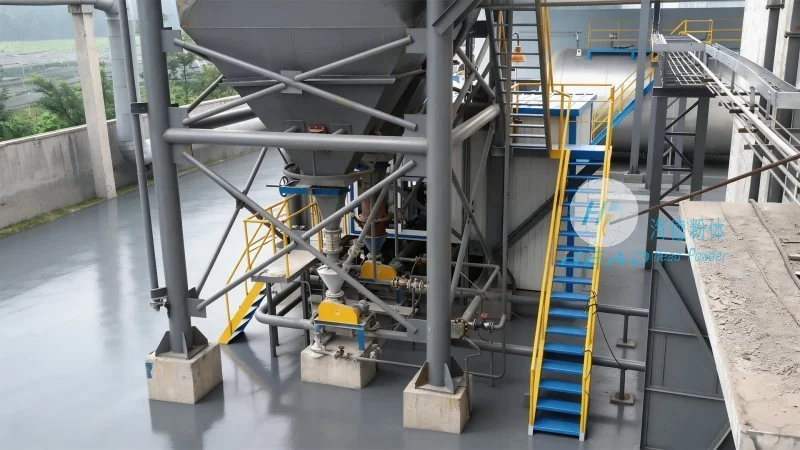
Benefits of Efficient Organic Fertilizer Powder Conveying
Implementing an efficient organic fertilizer powder conveying system offers numerous benefits for agricultural and fertilizer processing operations. Firstly, it enhances productivity by enabling continuous and uninterrupted material flow, reducing downtime and labor costs associated with manual handling. Secondly, it improves product quality by minimizing material degradation, segregation, and contamination during transport. This is crucial for maintaining the nutrient content and effectiveness of organic fertilizers. Thirdly, the system contributes to operational safety by reducing the need for manual handling of bulk materials, which can be heavy and potentially hazardous. Additionally, efficient conveying systems can improve energy efficiency and reduce operational costs through optimized air or power usage and reduced maintenance requirements.
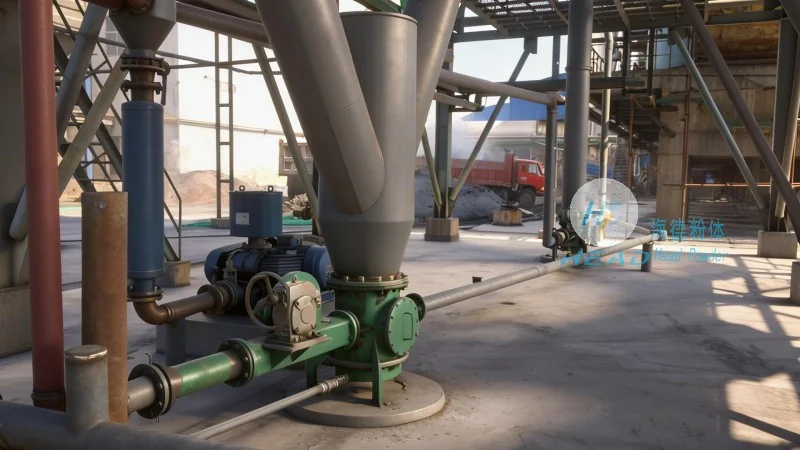
HeadPowder Engineering: Your Partner in Organic Fertilizer Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of specialized equipment for organic fertilizer processing and conveying. With a focus on innovation and customer-centric solutions, HeadPowder provides high-quality, reliable systems tailored to the unique needs of the organic fertilizer industry. The company’s expertise lies in designing and manufacturing equipment that meets stringent industry standards for efficiency, durability, and environmental compliance. HeadPowder’s products are engineered to handle a wide range of organic materials, ensuring consistent performance and minimal maintenance. The company’s commitment to quality and customer satisfaction has established it as a trusted partner for businesses seeking to optimize their organic fertilizer handling processes. HeadPowder’s facilities are located in Shandong, China, where the company leverages local resources and expertise to deliver cutting-edge solutions to clients worldwide.




