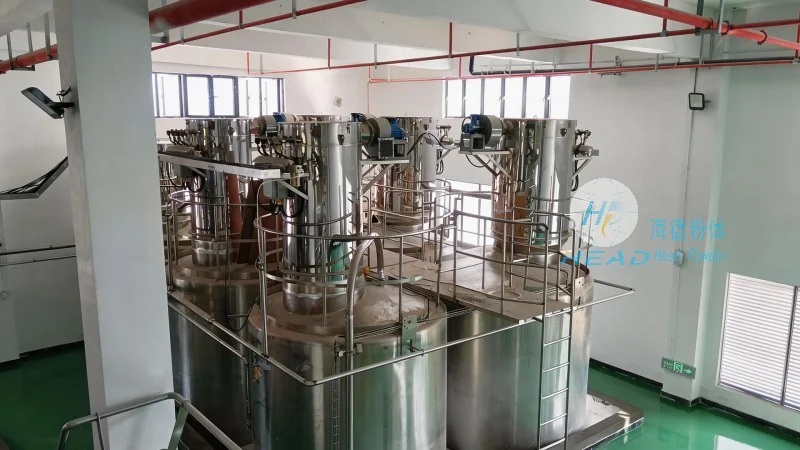
For industrial operations that require the efficient and reliable transportation of bulk powders, the gray tank truck powder conveying equipment stands out as a critical solution. This equipment is designed to handle various types of powders, including those with different flow properties and moisture content, ensuring seamless material transfer from the source to the destination. The design and functionality of this system are tailored to meet the demands of modern industrial processes, offering enhanced productivity and operational safety.
Company Overview and Expertise
HeadPowder, the manufacturer of this advanced powder conveying equipment, is a leading company in the field of bulk material handling solutions. With years of experience and a commitment to innovation, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of high-quality industrial equipment. The company's focus on research and development ensures that their products are not only efficient but also comply with international standards, making them suitable for diverse industrial applications worldwide.
Structural Components of the Gray Tank Truck Powder Conveying System
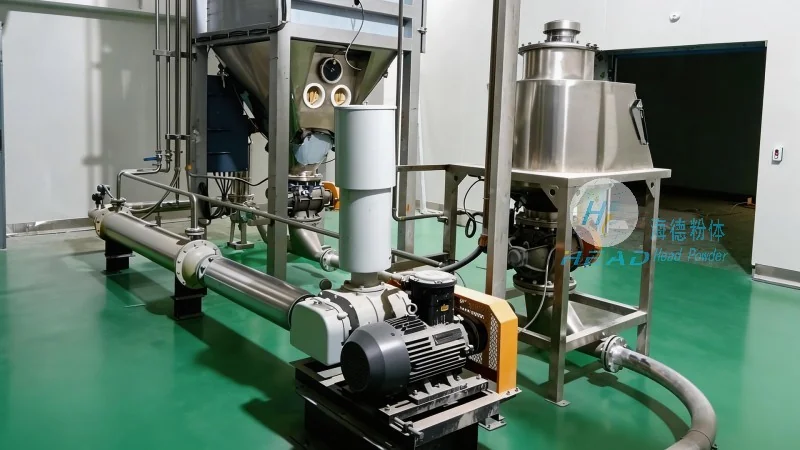
The gray tank truck powder conveying equipment consists of several key components that work in harmony to achieve effective powder transport. The primary components include the tank truck itself, which is equipped with a specialized hopper and agitator system to prevent material bridging and ensure consistent flow. The hopper is designed with a conical or wedge-shaped bottom to facilitate smooth material discharge, while the agitator, often a screw or paddle type, helps to maintain the powder's uniformity and prevent clogging. Additionally, the system incorporates a pressure relief valve and a level indicator to monitor the material level and prevent overfilling. The truck is also fitted with a discharge valve that can be controlled remotely, allowing for precise material release at the destination.
Working Principle and Operational Mechanism
The operation of the gray tank truck powder conveying equipment follows a systematic process that ensures efficient and safe powder transfer. Initially, the bulk powder is loaded into the tank truck at the source location. The agitator then begins to rotate, breaking up any agglomerates and ensuring that the powder is evenly distributed within the tank. As the truck moves to the destination, the agitator continues to operate, maintaining the powder's flowability. Upon arrival, the discharge valve is activated, and the powder is released into the receiving container or processing unit. The system's design minimizes the risk of material loss and contamination, making it ideal for applications where product purity is paramount.
Advantages and Applications
One of the key advantages of the gray tank truck powder conveying equipment is its ability to handle a wide range of powders, from fine to coarse particles, without compromising on efficiency. The equipment is also highly adaptable, allowing for integration with existing industrial systems and processes. Its compact design and easy maintenance make it suitable for various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. The system's reliability and durability ensure long-term performance, reducing downtime and maintenance costs for the end-user.
Quality Assurance and Technical Specifications
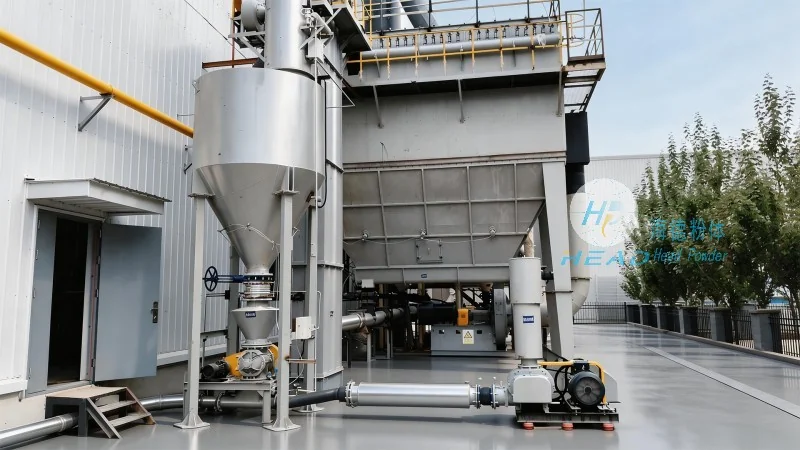
HeadPowder adheres to stringent quality control measures to ensure that each unit of the gray tank truck powder conveying equipment meets the highest standards. The company uses advanced manufacturing techniques and rigorous testing protocols to verify the performance and safety of their products. Technical specifications of the equipment include a maximum conveying capacity, which varies based on the powder type and truck size, typically ranging from 10 to 50 cubic meters per hour. The system operates under low pressure, reducing energy consumption and operational costs. Additionally, the equipment is constructed from corrosion-resistant materials, ensuring longevity and resistance to harsh environmental conditions.
Conclusion and Future Prospects
In conclusion, the gray tank truck powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for bulk powder handling. Its robust design, efficient operation, and adaptability make it an essential asset for industries that rely on consistent and reliable material transport. As industrial demands continue to evolve, the company remains committed to innovation, developing new technologies and solutions to meet the changing needs of the market. The equipment's performance and reliability ensure that it will remain a vital component in the future of bulk material handling.




