Biological enzyme powder transport systems represent a sophisticated technological solution designed to handle the efficient and precise delivery of enzyme powders in industrial and laboratory settings. These systems are integral to processes where enzyme activity and purity are critical, such as in pharmaceutical manufacturing, food processing, and biotechnology applications. The core function of these systems is to ensure that enzyme powders are transported without degradation, maintaining their biological activity and structural integrity throughout the process.
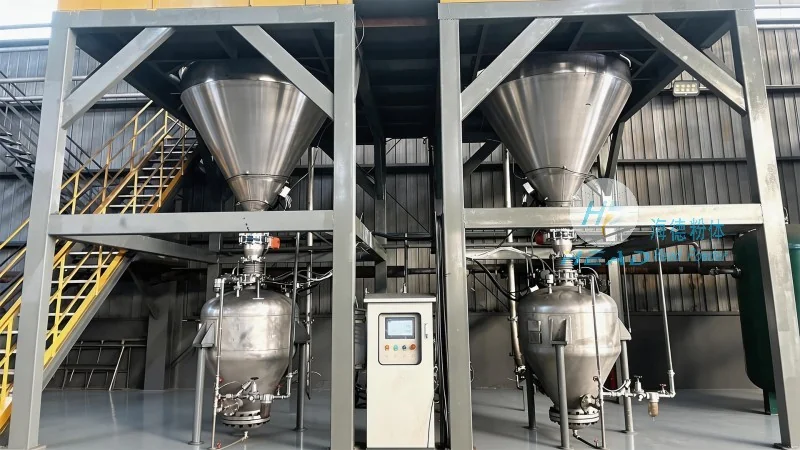
Key Components of the Biological Enzyme Powder Transport System
The biological enzyme powder transport system typically comprises several key components that work in tandem to achieve optimal performance. These components include a powder feeding mechanism, a transport conduit (often equipped with specialized liners or coatings to prevent enzyme degradation), and a control system for regulating flow rates and pressure. The feeding mechanism may involve a hopper or a dosing valve that ensures a consistent and controlled release of the enzyme powder. The transport conduit is designed with materials that are chemically inert to the enzymes, such as stainless steel or specialized polymers, to minimize interaction and maintain the powder's quality. The control system integrates sensors and actuators to monitor and adjust the transport parameters in real-time, ensuring that the enzyme powder is delivered under optimal conditions.
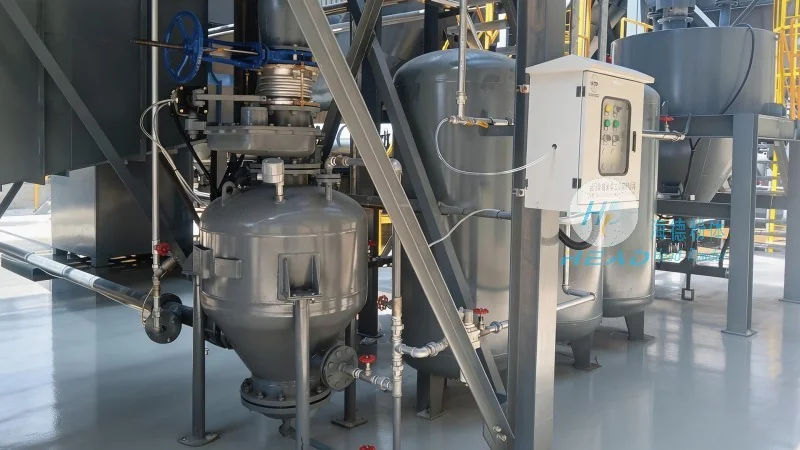
Design Principles Behind the Biological Enzyme Powder Transport System
The design principles of the biological enzyme powder transport system are centered on several critical factors to ensure reliability and efficiency. First, the system is engineered to minimize shear forces and mechanical stress on the enzyme particles, as excessive force can denature the enzymes and reduce their activity. This is achieved through the use of low-speed, gentle transport mechanisms, such as pneumatic conveying or screw conveyors with specialized blades. Second, the system prioritizes temperature control, as many enzymes are sensitive to temperature fluctuations. The transport conduit and associated components are often equipped with insulation or temperature-regulating features to maintain a stable environment. Third, the system incorporates contamination prevention measures, including sealed connections and sterile processing protocols, to ensure that the enzyme powder remains free from microbial contamination and other impurities. These design principles collectively contribute to the system's ability to deliver high-quality enzyme powders while preserving their biological activity.
Applications and Benefits of the Biological Enzyme Powder Transport System
The biological enzyme powder transport system finds applications in various industries where enzyme powders are essential. In the pharmaceutical industry, these systems are used to transport enzymes used in drug synthesis and formulation, ensuring that the final product meets strict quality standards. In the food industry, they are employed in processes such as cheese production and baking, where enzymes are used to improve texture and flavor. In biotechnology, the system supports research and development activities by providing a reliable method for handling enzyme powders during experiments and scale-up operations. The benefits of using this system include improved process efficiency, reduced enzyme degradation, and enhanced product quality. By maintaining the integrity of the enzyme powder, the system helps to minimize waste and lower production costs, making it a valuable asset for businesses operating in enzyme-dependent processes.
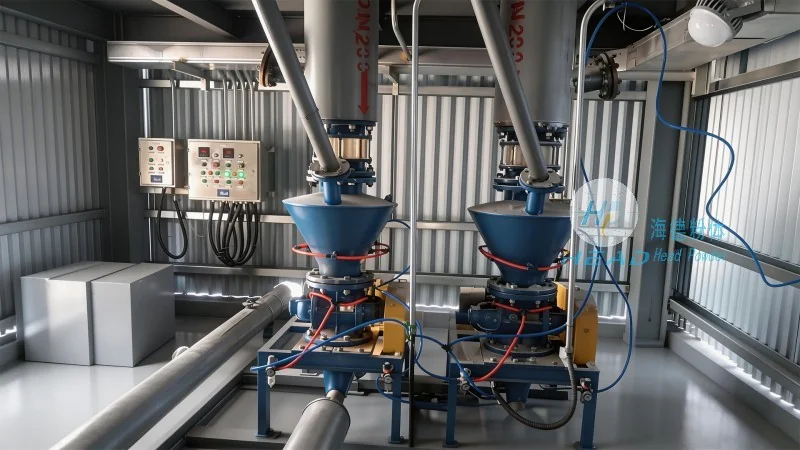
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized powder handling equipment. The company is headquartered in Shandong, China, and has established itself as a trusted provider of high-quality biological enzyme powder transport systems and related solutions. With a focus on innovation and customer satisfaction, headpowder leverages advanced engineering and manufacturing capabilities to deliver systems that meet the stringent requirements of modern industrial applications. The company's commitment to quality and reliability has made it a preferred choice for businesses seeking efficient and effective enzyme powder transport solutions.




