Understanding the Potassium Carbonate Fertilizer Powder Conveying System Equipment is crucial for those involved in the agricultural and chemical industries. This specialized equipment is designed to handle the efficient and safe transportation of potassium carbonate, a vital component in modern fertilizers. The system integrates advanced engineering principles to ensure optimal performance, reliability, and safety in handling this essential material.
Key Components of the Powder Conveying System
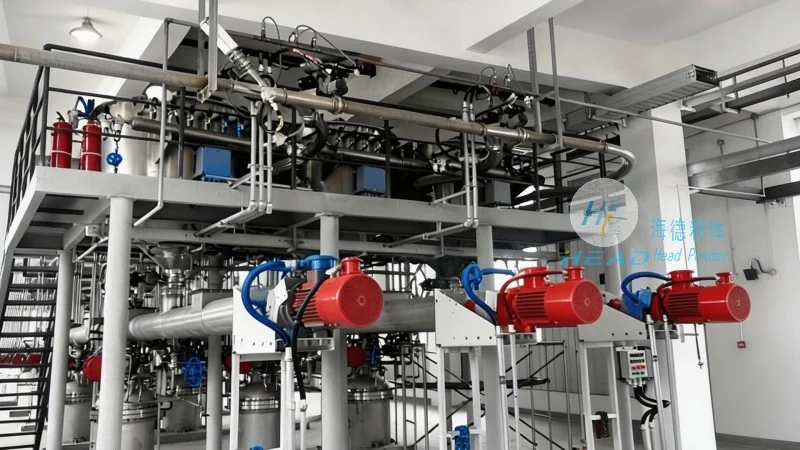
The Potassium Carbonate Fertilizer Powder Conveying System typically consists of several key components that work in harmony to achieve effective material handling. These components include feed hoppers, conveyor belts or pneumatic pipelines, control systems, and dust collection units. Each part plays a critical role in the overall operation, ensuring that the powder is moved from storage to processing or packaging areas without loss or contamination.
Design Principles and Engineering Considerations
The design of the Potassium Carbonate Fertilizer Powder Conveying System is based on several fundamental principles aimed at maximizing efficiency and minimizing operational risks. One of the primary considerations is the prevention of material buildup and clogging, which can occur due to the hygroscopic nature of potassium carbonate. Engineers incorporate features such as anti-static coatings, self-cleaning mechanisms, and adjustable speed controls to address these challenges. Additionally, the system is designed with material compatibility in mind, using corrosion-resistant materials like stainless steel to prevent contamination and ensure longevity.
Operational Efficiency and Safety Features
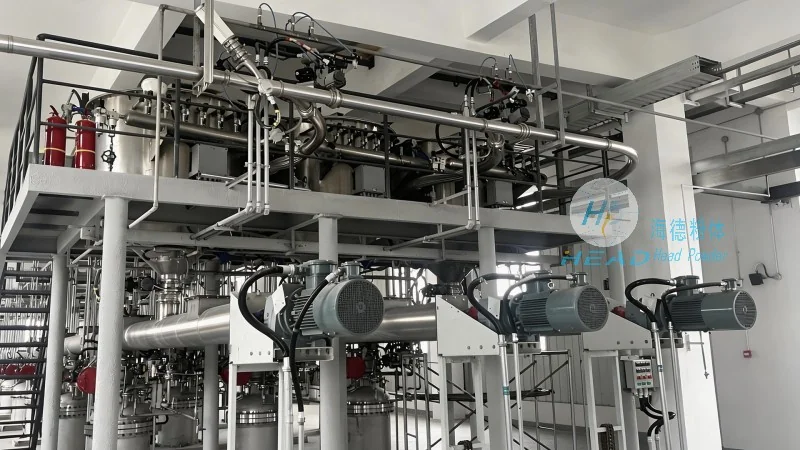
Operational efficiency is a key aspect of the system's design, with features that enhance throughput and reduce downtime. The control systems are equipped with sensors and monitoring tools that provide real-time data on flow rates, pressure, and temperature, allowing operators to adjust settings as needed. Safety features are also integral, including emergency shut-off valves, dust suppression systems, and protective enclosures to prevent exposure to airborne particles. These measures not only protect personnel but also comply with environmental regulations, ensuring the system operates within safe and sustainable parameters.
Applications in Fertilizer Production
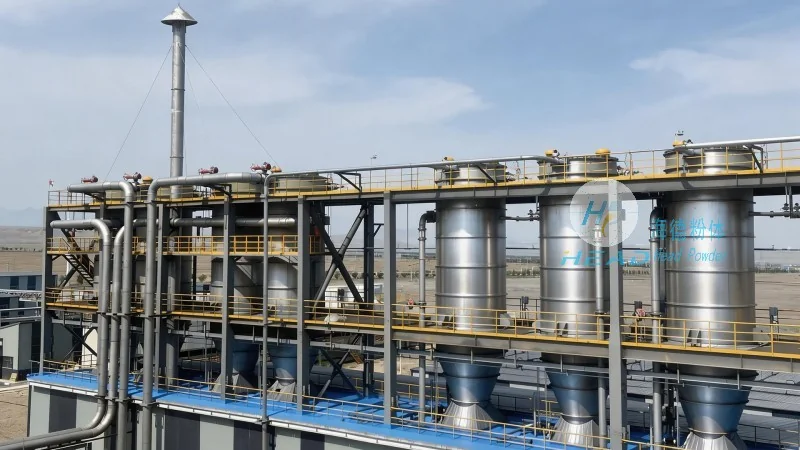
The Potassium Carbonate Fertilizer Powder Conveying System is widely used in fertilizer production facilities to transport potassium carbonate from raw material storage to blending and packaging stages. Its ability to handle large volumes of powder with precision and reliability makes it an essential part of modern fertilizer manufacturing processes. The system's design allows for seamless integration with other production equipment, such as mixers and granulators, creating a streamlined workflow that enhances overall productivity.
Advantages of Using a Specialized Conveying System
Investing in a specialized Potassium Carbonate Fertilizer Powder Conveying System offers several advantages over traditional methods. These systems provide higher throughput and lower energy consumption compared to manual or less efficient conveying methods. They also reduce the risk of material loss and contamination, which can impact product quality and profitability. Furthermore, the advanced control systems enable better monitoring and maintenance, reducing the likelihood of unexpected downtime and increasing the system's overall lifespan.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of specialized powder handling equipment, including the Potassium Carbonate Fertilizer Powder Conveying System. With years of experience in the industry, the company has developed a reputation for producing high-quality, reliable equipment tailored to the specific needs of its clients. HeadPowder's facilities are located in Shandong, China, where the company leverages advanced manufacturing techniques and a skilled workforce to ensure each product meets the highest standards of performance and safety.




