The intelligent tonne bag loading station powder conveying machine is a specialized industrial equipment designed for efficient handling and transportation of bulk powders from large tonne bags. This system integrates advanced automation technologies to streamline the process of material transfer, ensuring high accuracy, safety, and operational efficiency in various industrial applications.
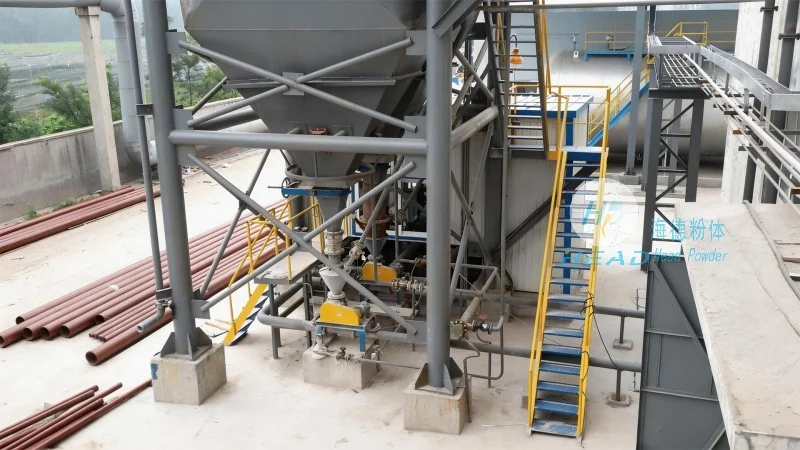
About HeadPowder: Your Trusted Partner in Powder Handling Solutions
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing and supplying advanced powder handling equipment. With years of expertise in the field, HeadPowder has established itself as a reliable partner for industries requiring robust and reliable powder conveying systems. The company’s commitment to innovation and quality ensures that its products meet the highest standards of performance and durability.
Core Components and Design of the Tonne Bag Loading Station
The intelligent tonne bag loading station typically consists of several key components that work in harmony to achieve seamless powder transfer. These include a vertical or horizontal screw conveyor, a bag opening mechanism, a dust collection system, and an automated control panel. The design emphasizes user-friendly operation and minimal maintenance, making it suitable for continuous industrial production lines.
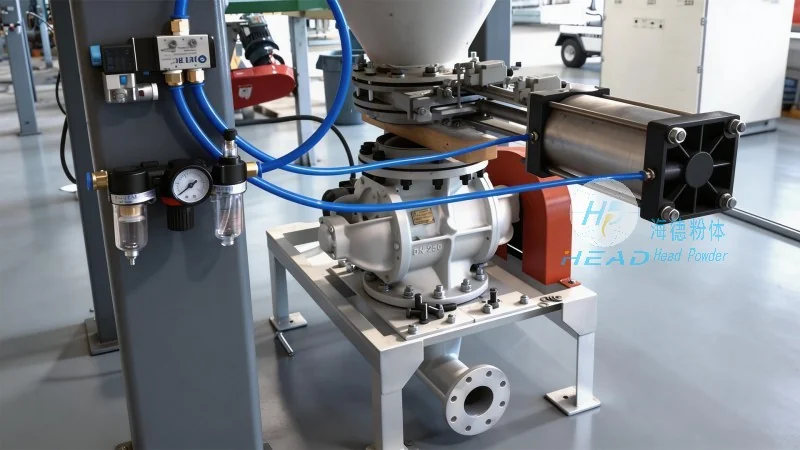
Design Principles: Ensuring Efficiency and Reliability
The design principles of the tonne bag loading station are centered around optimizing material flow, minimizing downtime, and enhancing safety. Key principles include: 1. Material Flow Optimization: The system is engineered to ensure smooth and consistent flow of powders from the bag to the conveyor, reducing blockages and ensuring uniform material transfer. 2. Automation and Control: Advanced control systems allow for precise regulation of the conveying process, enabling operators to monitor and adjust parameters in real-time. 3. Safety Features: Integrated safety mechanisms, such as emergency stop buttons and dust suppression systems, protect both personnel and equipment from potential hazards. 4. Modular Design: The equipment is designed with modular components that can be easily customized or upgraded to meet specific customer requirements.
Key Features and Benefits of the Powder Conveying Machine
HeadPowder’s intelligent tonne bag loading station offers a range of features that enhance its performance and usability. These include: - High Capacity and Efficiency: Capable of handling large volumes of powders at high speeds, reducing processing time and increasing overall productivity. - Low Maintenance Requirements: Robust construction and easy-to-clean components minimize downtime and maintenance costs. - Adaptability: The system can be configured to handle various types of powders, including fine, coarse, or abrasive materials. - Environmental Compliance: Integrated dust collection systems ensure compliance with environmental regulations and maintain a clean working environment.
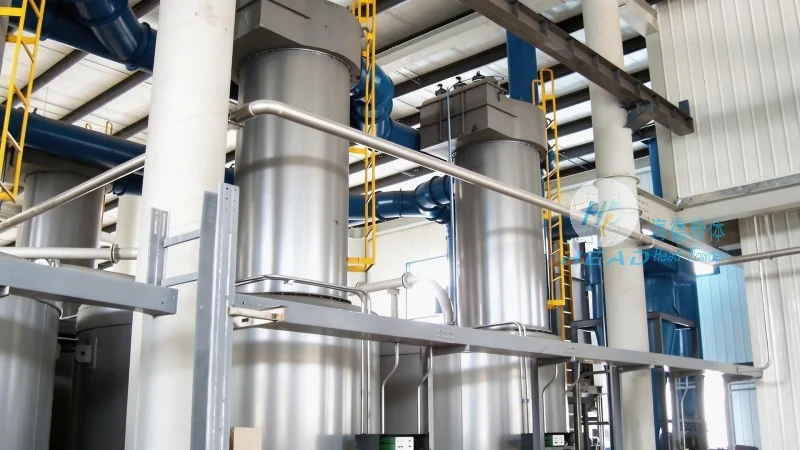
Applications in Industrial Settings
The intelligent tonne bag loading station is widely used in industries such as pharmaceuticals, food processing, chemicals, and mining. It is particularly valuable in applications where large quantities of powders need to be transferred from storage bags to processing equipment, such as mixers, reactors, or packaging lines. The system’s ability to handle different powder types and its high efficiency make it an essential component in modern industrial operations.
Conclusion: Enhancing Productivity with Advanced Powder Handling Technology
HeadPowder’s intelligent tonne bag loading station powder conveying machine represents a significant advancement in bulk powder handling technology. By combining advanced design principles with robust construction, this equipment provides industries with a reliable and efficient solution for their material transfer needs. With its focus on automation, safety, and adaptability, the system helps businesses improve productivity, reduce costs, and maintain compliance with industry standards. As a leading manufacturer in Shandong, China, HeadPowder continues to innovate and deliver high-quality solutions that meet the evolving demands of the powder handling industry.




