Nanometer calcium carbonate (n-CaCO₃) is a widely used industrial filler and reinforcement material, known for its high surface area and excellent dispersion properties. As a key component in various industries, including plastics, coatings, and paper, the efficient handling and transportation of n-CaCO₃ are crucial for maintaining product quality and production efficiency. This article explores the material handling equipment specifically designed for n-CaCO₃, detailing its design principles and operational considerations.
The Importance of Specialized Equipment for Nanometer Calcium Carbonate
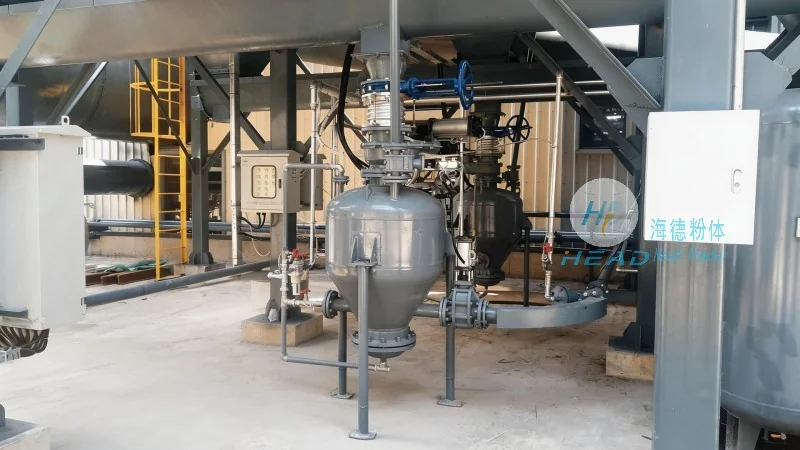
The unique physical and chemical properties of nanometer calcium carbonate, such as its fine particle size and high surface energy, make conventional bulk material handling equipment unsuitable. Standard conveyors or silos may cause agglomeration, caking, or uneven distribution, leading to inconsistent product performance. Specialized equipment is therefore essential to ensure the material remains in a free-flowing state, preventing quality degradation and optimizing processing. The design of such equipment must address challenges like dust generation, material flow control, and compatibility with the material's sensitivity to moisture and temperature.
Design Principles of Nanometer Calcium Carbonate Material Handling Equipment
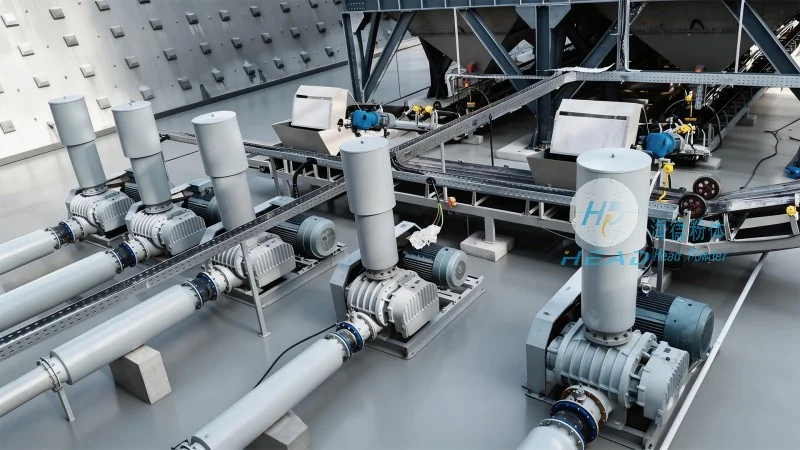
The design of nanometer calcium carbonate material handling equipment focuses on several critical principles to ensure optimal performance and material integrity. First, the equipment must minimize particle attrition and surface damage, as n-CaCO₃ particles are highly susceptible to mechanical stress. This is achieved through the use of smooth, low-friction surfaces and gentle handling mechanisms, such as screw conveyors with slow rotation speeds or pneumatic conveying systems with low air velocity. Second, the equipment is engineered to prevent agglomeration and caking, which can occur due to moisture absorption or static electricity. Anti-static coatings, moisture-proof seals, and humidification systems are integrated into the design to maintain the material's free-flowing state. Third, the equipment must ensure uniform material distribution and consistent flow rates, which is vital for downstream processing. This is accomplished through adjustable feed mechanisms, flow control valves, and level sensors that regulate the material's movement through the system.
Key Components and Operational Features
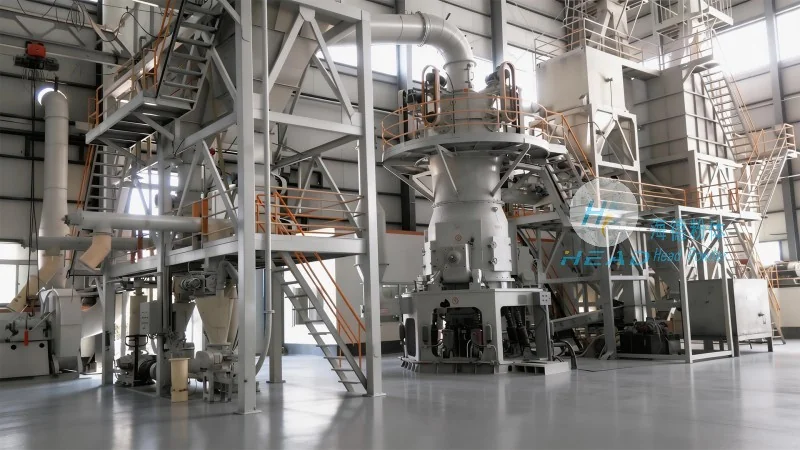
Specialized nanometer calcium carbonate material handling equipment typically includes several key components that work in tandem to achieve efficient and safe operation. The primary components include a hopper or storage silo, a conveying system (such as a screw conveyor or pneumatic conveyor), a feeding mechanism, and a control system. The hopper is designed with a conical or wedge-shaped bottom to facilitate uniform material discharge and prevent bridging. The conveying system is constructed from materials resistant to chemical corrosion and wear, such as stainless steel or special alloys, to withstand the abrasive nature of n-CaCO₃ particles. The feeding mechanism, often a rotary valve or a metering pump, regulates the flow rate of the material into the conveying system, ensuring precise control over the amount of n-CaCO₃ delivered to the processing line. The control system, equipped with sensors and automation software, monitors parameters like pressure, temperature, and material level, providing real-time feedback and adjusting operations as needed to maintain optimal performance.
Benefits of Using Specialized Material Handling Equipment for n-CaCO₃
Implementing specialized material handling equipment for nanometer calcium carbonate offers numerous benefits that directly impact production efficiency and product quality. By preventing agglomeration and maintaining the material's fine particle structure, the equipment ensures consistent product performance across batches. This leads to improved product uniformity, reduced waste, and lower costs associated with reprocessing or material replacement. Additionally, the equipment minimizes dust generation and improves workplace safety, as the design incorporates dust collection systems and sealed enclosures. The precise control over flow rates and material distribution also enhances the efficiency of downstream processing equipment, reducing downtime and increasing overall production throughput. For manufacturers, this translates to higher profitability and a competitive edge in the market.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized material handling equipment for industrial powders, including nanometer calcium carbonate. With a focus on innovation and customer-centric solutions, the company has developed advanced equipment designed to meet the unique challenges of handling fine and sensitive materials. Headpowder's products are engineered with high-quality materials and advanced technology to ensure durability, efficiency, and reliability. The company's facilities are located in Shandong, China, where it leverages local expertise and resources to deliver superior products and services to clients worldwide. By combining technical expertise with practical experience, headpowder provides tailored solutions that enhance the performance and productivity of its customers' operations.




