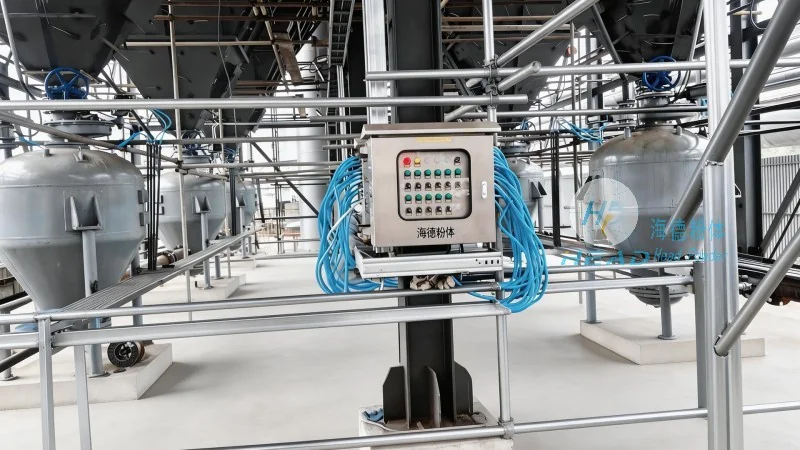
Intelligent weighing material handling conveyors represent a sophisticated integration of automation, precision measurement, and material transport technologies. These systems are engineered to streamline production processes by combining the functions of conveying materials with real-time weighing capabilities. The core objective is to enhance operational efficiency, reduce human error, and ensure consistent product quality in various industrial applications.
Introduction to Intelligent Weighing Material Handling Conveyors
An intelligent weighing conveyor is a specialized piece of industrial equipment designed to transport bulk materials or packaged goods while simultaneously measuring their weight. Unlike traditional conveyors that only move items from one location to another, these systems incorporate load cells, sensors, and advanced control systems to provide accurate weight data at each stage of the process. This integration enables real-time monitoring, quality control, and data-driven decision-making, making them indispensable in industries such as food processing, pharmaceuticals, chemicals, and manufacturing.
Key Components and Functional Design
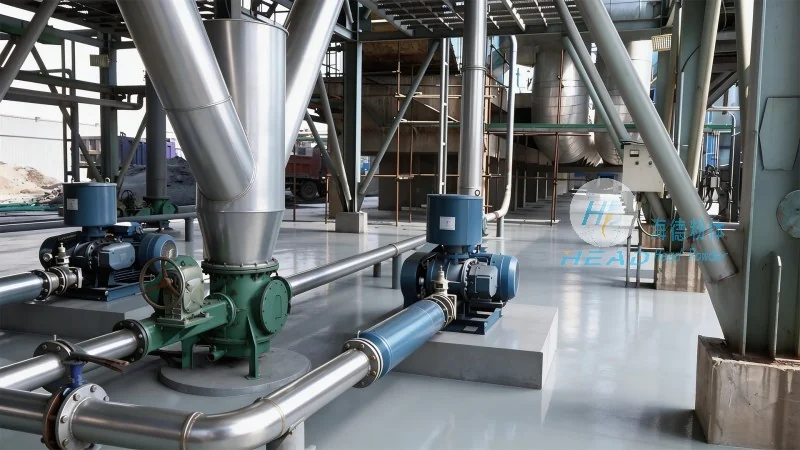
The design of an intelligent weighing conveyor typically involves several critical components that work in harmony to achieve precise performance. At the heart of the system are load cells, which are sensors that convert the weight of the material into an electrical signal. These signals are then processed by a control unit, often equipped with a digital display or connected to a central system for data logging and analysis. The conveyor itself may consist of belt systems, roller tracks, or chain-driven mechanisms, tailored to the specific characteristics of the materials being handled—whether they are granular, powdery, or solid items.
Additional components may include level sensors to detect the presence of material, speed controllers to regulate conveyor movement, and integration with other automation equipment such as sorters or packaging machines. The control system typically employs programmable logic controllers (PLCs) or industrial computers, allowing for customization of weighing parameters, alarm settings, and data output formats. This modular design enables manufacturers to adapt the system to diverse production requirements while maintaining high levels of accuracy and reliability.
Core Design Principles for Precision and Efficiency
The design principles underlying intelligent weighing conveyors prioritize two main objectives: precision measurement and operational efficiency. Precision is achieved through the use of high-quality load cells with low hysteresis and excellent linearity, ensuring that even small variations in weight are accurately captured. The control system employs advanced algorithms, such as digital filtering and calibration routines, to minimize noise and environmental interference, further enhancing measurement accuracy. Additionally, the conveyor's speed is carefully controlled to allow sufficient time for the load cells to stabilize, preventing errors caused by rapid movement.
Efficiency is optimized through the integration of automation and real-time data processing. By combining weighing with material transport, the system eliminates the need for separate weighing stations or manual weighing operations, reducing cycle times and labor costs. The ability to monitor weight in real time enables immediate corrective actions, such as adjusting feed rates or identifying product defects, which can prevent waste and improve overall production throughput. Furthermore, the data collected by the weighing system can be used for quality control, inventory management, and process optimization, providing valuable insights into production performance.
Application Scenarios and Industry Integration
Intelligent weighing conveyors find applications across a wide range of industries, where precise material handling and quality control are critical. In the food and beverage sector, these systems are used to weigh ingredients during mixing or packaging, ensuring consistent product composition and compliance with regulatory standards. In the pharmaceutical industry, they are employed to weigh active pharmaceutical ingredients (APIs) and finished dosage forms, maintaining strict dosage accuracy and batch traceability. The chemical industry utilizes them for weighing raw materials in bulk processing, while manufacturing sectors rely on them for quality inspection of components before assembly.
The versatility of these systems allows them to be integrated into existing production lines or used as standalone units, depending on the specific needs of the operation. They can be customized to handle different material types, such as powders, granules, or liquids, and can be scaled to accommodate varying production volumes. The integration with other automation equipment, such as sorters, fillers, or packaging machines, further enhances their functionality, creating a seamless workflow from material input to final product output.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
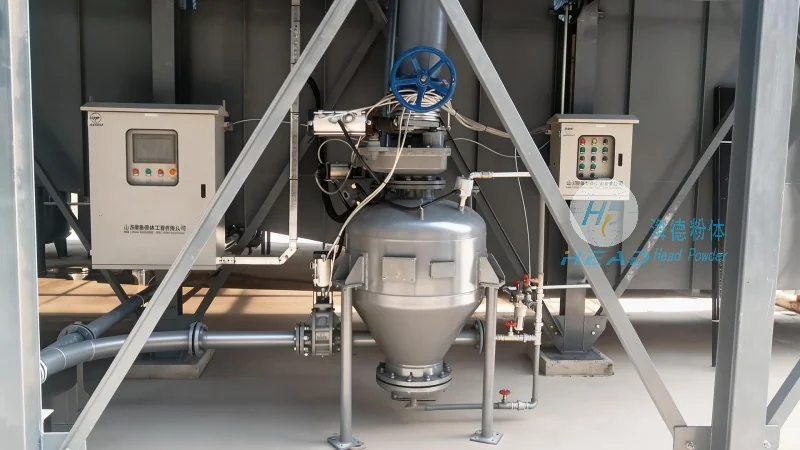
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of industrial automation, specializes in the design, development, and production of intelligent weighing material handling conveyors. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking to enhance their production efficiency and product quality. HeadPowder's products are engineered to meet the highest industry standards, incorporating advanced technology and robust construction to ensure long-term reliability and performance.
HeadPowder's headquarters is located in Shandong, China, where the company operates a state-of-the-art manufacturing facility equipped with modern equipment and skilled technicians. The company's team of engineers and technicians brings extensive experience in industrial automation, ensuring that each product is tailored to the unique requirements of the customer. By leveraging cutting-edge technologies and adhering to strict quality control processes, HeadPowder delivers solutions that not only meet but exceed industry expectations.
With a focus on customer satisfaction and continuous improvement, Shandong HeadPowder Engineering Co., Ltd. provides comprehensive support to its clients, including design consultation, installation, and after-sales service. The company's dedication to excellence has earned it a reputation for delivering reliable and efficient intelligent weighing conveyors that contribute to the success of its clients' operations. Through its commitment to innovation and quality, HeadPowder remains at the forefront of the industrial automation industry, providing solutions that drive productivity and enhance competitiveness.




