For industries dealing with powders, maintaining a stable and efficient handling process is crucial. Nitrogen circulation powder transport systems offer a solution that enhances safety, efficiency, and product integrity. This article explores the working principle and key features of such systems, providing insights into how they operate and their benefits in industrial applications.
Working Principle of Nitrogen Circulation Powder Transport
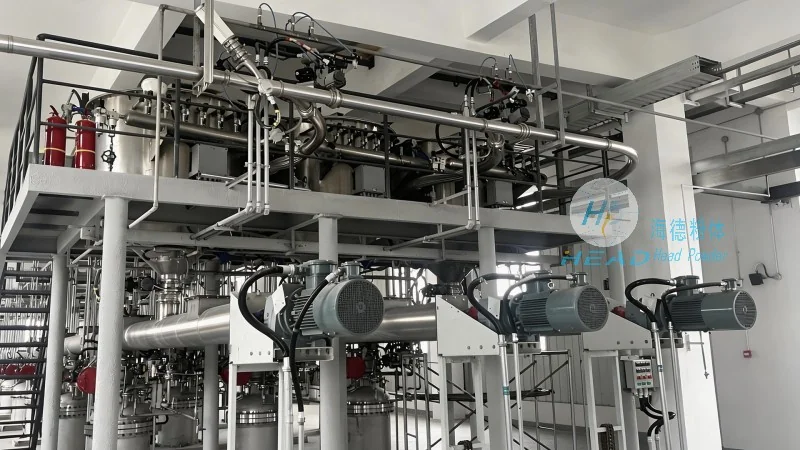
The core of a nitrogen circulation powder transport system lies in its closed-loop design, which utilizes nitrogen gas to create a controlled environment for powder movement. The process typically begins with a powder storage silo or hopper. From there, the powder is drawn into a transport line using a nitrogen-powered conveyor or pneumatic system. Nitrogen gas is introduced into the system to displace air, preventing oxidation and contamination of the powder. The gas then carries the powder particles through the pipeline to the destination, such as a processing unit or another storage area. The system recirculates the nitrogen gas, ensuring minimal waste and maintaining a consistent pressure and flow rate throughout the transport process. This closed-loop mechanism not only improves efficiency but also reduces the risk of dust explosions and other safety hazards associated with open powder handling.
Key Features of Nitrogen Circulation Powder Transport Systems
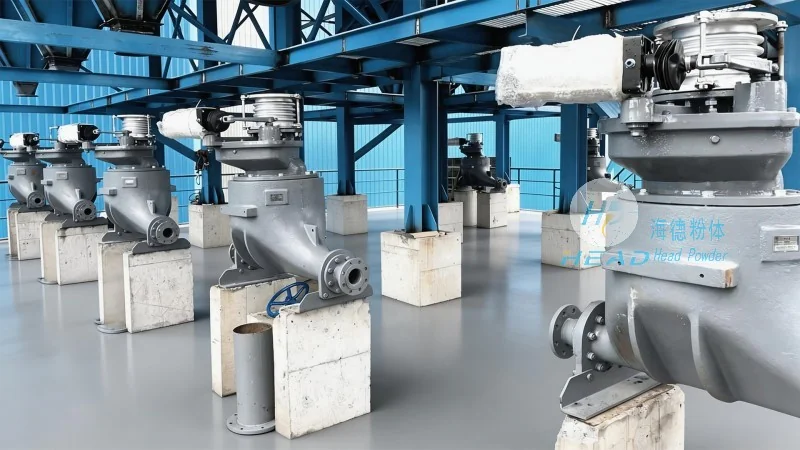
Several distinct features make nitrogen circulation powder transport systems highly effective for various industrial needs. First, the closed-loop design ensures that the powder remains in a controlled atmosphere, minimizing exposure to ambient air and contaminants. This is particularly important for sensitive materials, such as pharmaceuticals, food products, or chemicals that are prone to degradation. Second, the use of nitrogen gas provides an inert environment, which is essential for preventing oxidation and chemical reactions that could alter the powder's properties. Third, the system's ability to maintain consistent pressure and flow rates ensures reliable and uniform powder delivery, reducing variations in product quality. Additionally, the recirculation of nitrogen gas reduces operational costs by minimizing the need for continuous gas supply and reducing waste. The systems are also designed for easy maintenance, with components that can be accessed and serviced without disrupting the entire operation. This makes them suitable for continuous production environments where downtime is a critical factor.
Benefits and Applications
Implementing a nitrogen circulation powder transport system offers numerous advantages for businesses. The primary benefit is enhanced safety, as the closed-loop system eliminates the risk of dust explosions by removing oxygen from the environment. This is especially valuable in industries where powder handling is a regular part of operations, such as in chemical manufacturing, food processing, and pharmaceutical production. Another significant benefit is improved product quality and consistency. By preventing contamination and oxidation, the system ensures that the powder reaches its destination with the same properties as when it was initially stored. This is crucial for applications where product purity is non-negotiable, such as in the production of high-value pharmaceuticals or specialty chemicals. Furthermore, the energy efficiency of the recirculating system reduces operational costs over time, making it a cost-effective solution for long-term use. The systems are versatile and can be adapted to handle a wide range of powder types and sizes, from fine powders to bulk materials. This flexibility allows companies to use the same system for multiple applications, reducing the need for specialized equipment and simplifying inventory management.
Conclusion
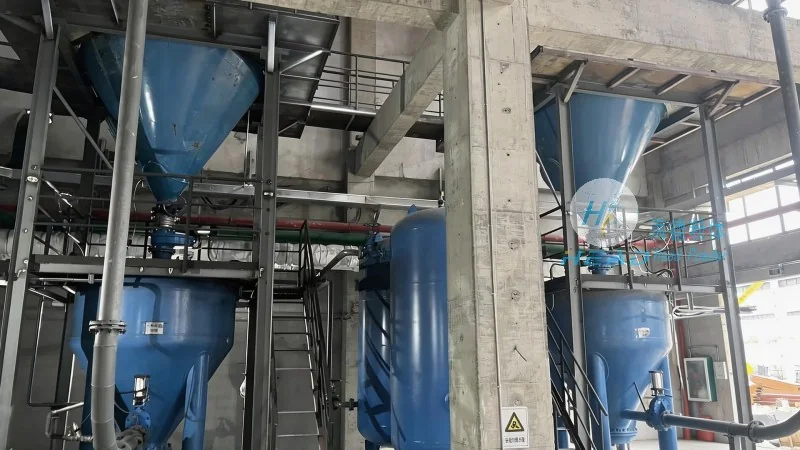
Nitrogen circulation powder transport systems represent a sophisticated approach to handling powders in industrial settings. By combining a closed-loop design with the inert properties of nitrogen gas, these systems offer a reliable, safe, and efficient method for transporting powders. The key features, including controlled atmosphere, consistent flow, and reduced waste, make them an attractive option for businesses seeking to improve their powder handling processes. As industries continue to prioritize safety and product quality, the adoption of such systems is likely to increase, providing a sustainable solution for the future of powder transport.




