Small stone powder conveying systems are essential in various industrial applications where the efficient transport of bulk materials is required. These systems are designed to handle materials like small stones and powders, ensuring smooth and reliable material handling processes. The technology behind these systems is crucial for optimizing production workflows and maintaining operational efficiency in industries such as mining, construction, and chemical processing.
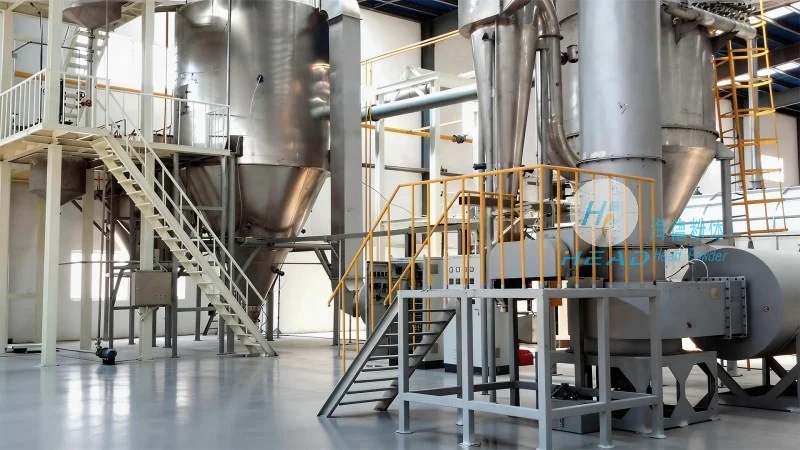
Working Principle of Small Stone Powder Conveying Systems
The core working principle of small stone powder conveying systems involves the use of specialized equipment to move bulk materials from one location to another. Typically, these systems utilize mechanisms like screw conveyors, pneumatic conveyors, or belt conveyors, depending on the specific material characteristics and operational requirements. The process begins with the material being fed into the conveyor system, where it is then transported through a series of components. For example, in a screw conveyor, a rotating screw (or auger) pushes the material forward along a trough or pipe. This mechanism ensures that the material is moved continuously without the need for external forces like gravity or pressure. Pneumatic conveyors, on the other hand, use compressed air to create a flow that carries the powder or small stones through a pipeline. This method is particularly effective for materials that are dusty or require a dust-free environment. The choice of conveyor type depends on factors such as the material's density, moisture content, and the distance it needs to be transported. By understanding the fundamental working principles, users can select the most appropriate system for their specific needs, ensuring optimal performance and minimal downtime.
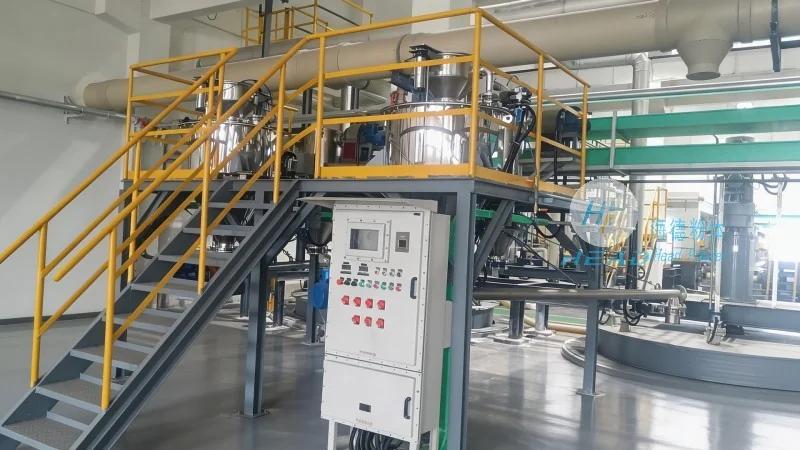
Key Features of Small Stone Powder Conveying Systems
Small stone powder conveying systems offer several key features that make them valuable in industrial settings. One of the primary advantages is their ability to handle a wide range of materials, including fine powders and small stone particles. This versatility allows these systems to be used in diverse applications, from food processing to mining operations. Another important feature is the system's efficiency in terms of energy consumption and operational costs. Modern conveying systems are designed to minimize energy usage while maximizing material throughput, leading to significant cost savings over time. Additionally, these systems are often equipped with advanced control systems that allow for precise monitoring and adjustment of the conveying process. This includes features like variable speed drives, which can be adjusted to match the material flow rate, and sensors that detect blockages or other issues, preventing system failures. The durability of the equipment is also a critical feature, as it must withstand the abrasive nature of small stones and powders. High-quality materials and robust construction ensure that the system has a long service life, reducing maintenance and replacement costs. Furthermore, the systems are designed to be compact and space-efficient, making them suitable for installations in limited spaces. This is particularly beneficial in facilities where floor space is at a premium. The ability to integrate with other industrial equipment is another notable feature, as these conveying systems can be connected to storage silos, processing units, or packaging machinery, creating a seamless material handling workflow. Overall, the combination of efficiency, versatility, and durability makes small stone powder conveying systems a reliable choice for industries that require consistent and reliable material transport.
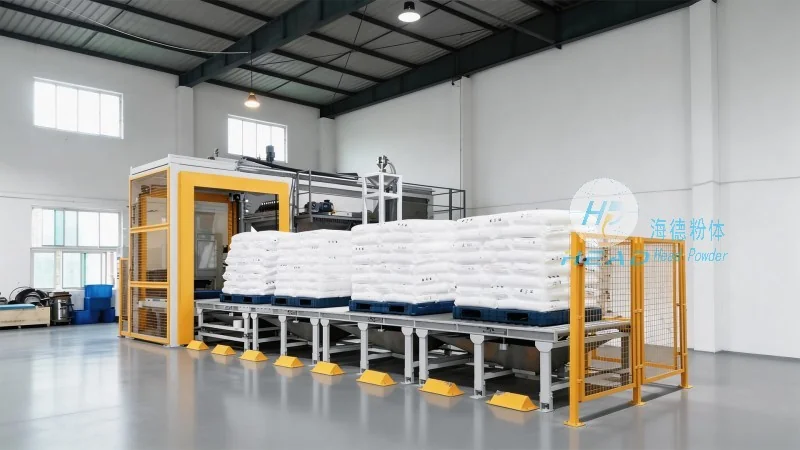
Applications and Benefits in Industrial Settings
Small stone powder conveying systems find applications in various industries, each benefiting from the unique capabilities of these systems. In the mining industry, for example, these systems are used to transport crushed stone and fine powders from processing plants to storage facilities or for further processing. The ability to handle abrasive materials without significant wear and tear makes them ideal for this application. In the construction industry, small stone powder conveying systems are used to transport sand, gravel, and other aggregates to construction sites. This ensures that materials are delivered efficiently and in the right quantities, supporting timely project completion. The chemical industry also utilizes these systems to transport powders and small stones used in manufacturing processes. The systems' ability to maintain a dust-free environment is particularly important in this sector, as it helps to prevent contamination and ensure product quality. The benefits of using small stone powder conveying systems extend beyond just material transport. By improving the efficiency of material handling, these systems can reduce labor costs and increase overall productivity. The reduced need for manual handling of bulk materials also enhances workplace safety, as it minimizes the risk of accidents and injuries. Additionally, the consistent flow of materials ensures that production processes run smoothly, avoiding bottlenecks and delays. The environmental benefits are also significant, as these systems help to reduce the amount of dust and particulate matter released into the air, contributing to a cleaner working environment. Overall, the applications and benefits of small stone powder conveying systems make them a valuable investment for any industry that relies on bulk material transport.
Conclusion and Company Overview
Small stone powder conveying systems are critical components in modern industrial operations, providing efficient and reliable transport of bulk materials. The working principles and features of these systems are designed to meet the diverse needs of various industries, ensuring optimal performance and minimal operational issues. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of high-quality conveying systems tailored to specific customer requirements. With a focus on innovation and durability, the company ensures that its products meet the highest standards of performance and safety. Based in Shandong, China, HeadPowder leverages its expertise and experience to deliver solutions that enhance operational efficiency and reduce costs for its clients. By understanding the working principles and features of small stone powder conveying systems, industries can make informed decisions about their material handling needs, ultimately leading to improved productivity and profitability. The combination of advanced technology and professional service makes HeadPowder a trusted partner for businesses seeking reliable and efficient conveying solutions.




