Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and manufacturing of advanced powder conveying systems tailored for industries handling white and gray powders. This article explores the working principle and key features of such systems, offering insights into their efficiency and reliability.
Overview of White Gray Powder Conveying Systems
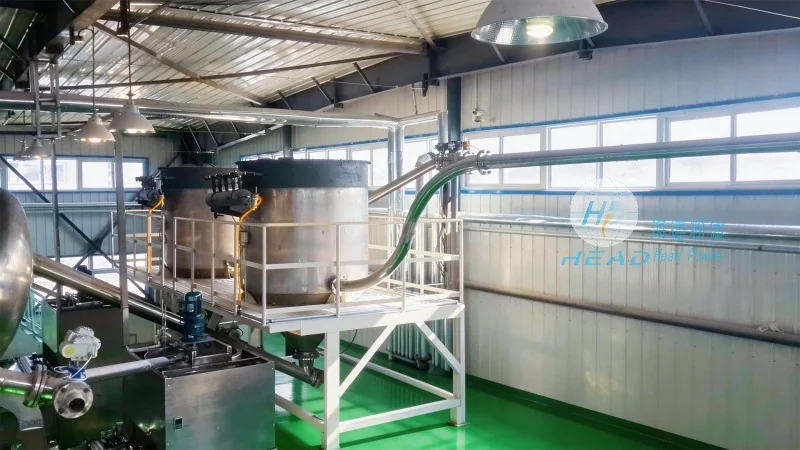
White gray powder conveying systems are engineered to transport fine powders like white cement, gray fly ash, or similar materials with high precision and minimal loss. These systems integrate multiple components to ensure smooth material handling, from initial storage to final discharge. The core components typically include a hopper for material storage, a feeding mechanism to control the flow rate, a conveying unit (either pneumatic or mechanical), and a discharge valve for targeted delivery.
Working Principle of the Powder Conveying System
The operation of a white gray powder conveying system begins with material loading into the hopper. The system uses a controlled feeding device, such as a rotary valve or a screw feeder, to regulate the flow of powder into the conveying line. For pneumatic systems, compressed air is introduced to create a pressure differential, drawing the powder particles along the pipeline. Mechanical systems, like screw conveyors or belt conveyors, rely on rotating components to move the material through the system. The system ensures consistent material flow by maintaining proper pressure and speed, preventing blockages or material degradation.
Key Features of the White Gray Powder Conveying System
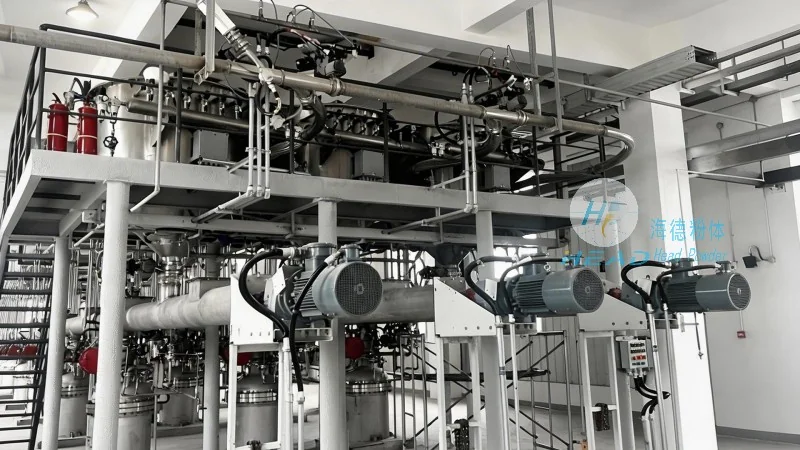
Efficiency and reliability are paramount in white gray powder conveying systems. The design incorporates features such as anti-caking mechanisms to prevent material buildup in the hopper, which is crucial for powders prone to agglomeration. The system also includes dust collection and filtration components to maintain air quality and comply with environmental regulations. Additionally, the conveying units are constructed from corrosion-resistant materials, suitable for handling moisture-sensitive or chemically active powders. The control system allows for real-time monitoring and adjustment of flow rates, ensuring optimal performance under varying operational conditions.
Application and Benefits in Industrial Settings
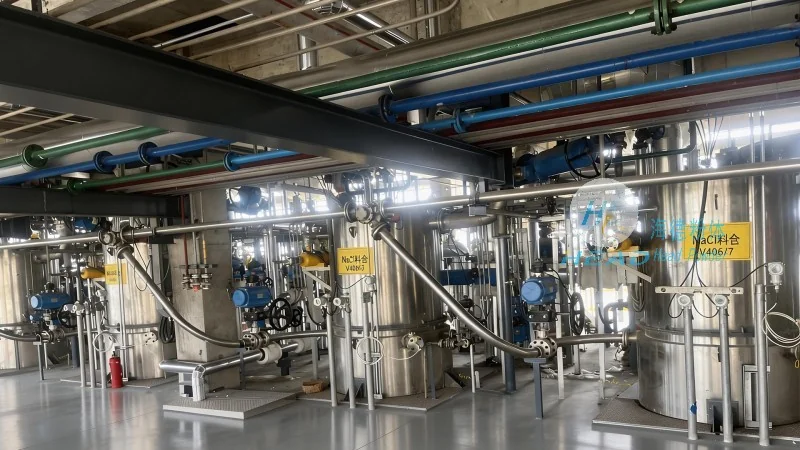
These conveying systems are widely used in construction, cement production, and industrial manufacturing where consistent and safe powder transport is critical. The benefits include reduced labor costs due to automated operation, minimized material waste through precise control, and enhanced safety by eliminating manual handling of powders. The systems also contribute to improved production efficiency by ensuring a steady supply of raw materials to processing units.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for white gray powder conveying systems, combining advanced technology with robust engineering. The systems' working principle and features make them ideal for industries requiring reliable, efficient, and environmentally friendly powder handling. By understanding these aspects, businesses can make informed decisions about integrating such systems into their operations, ultimately enhancing productivity and operational safety.




